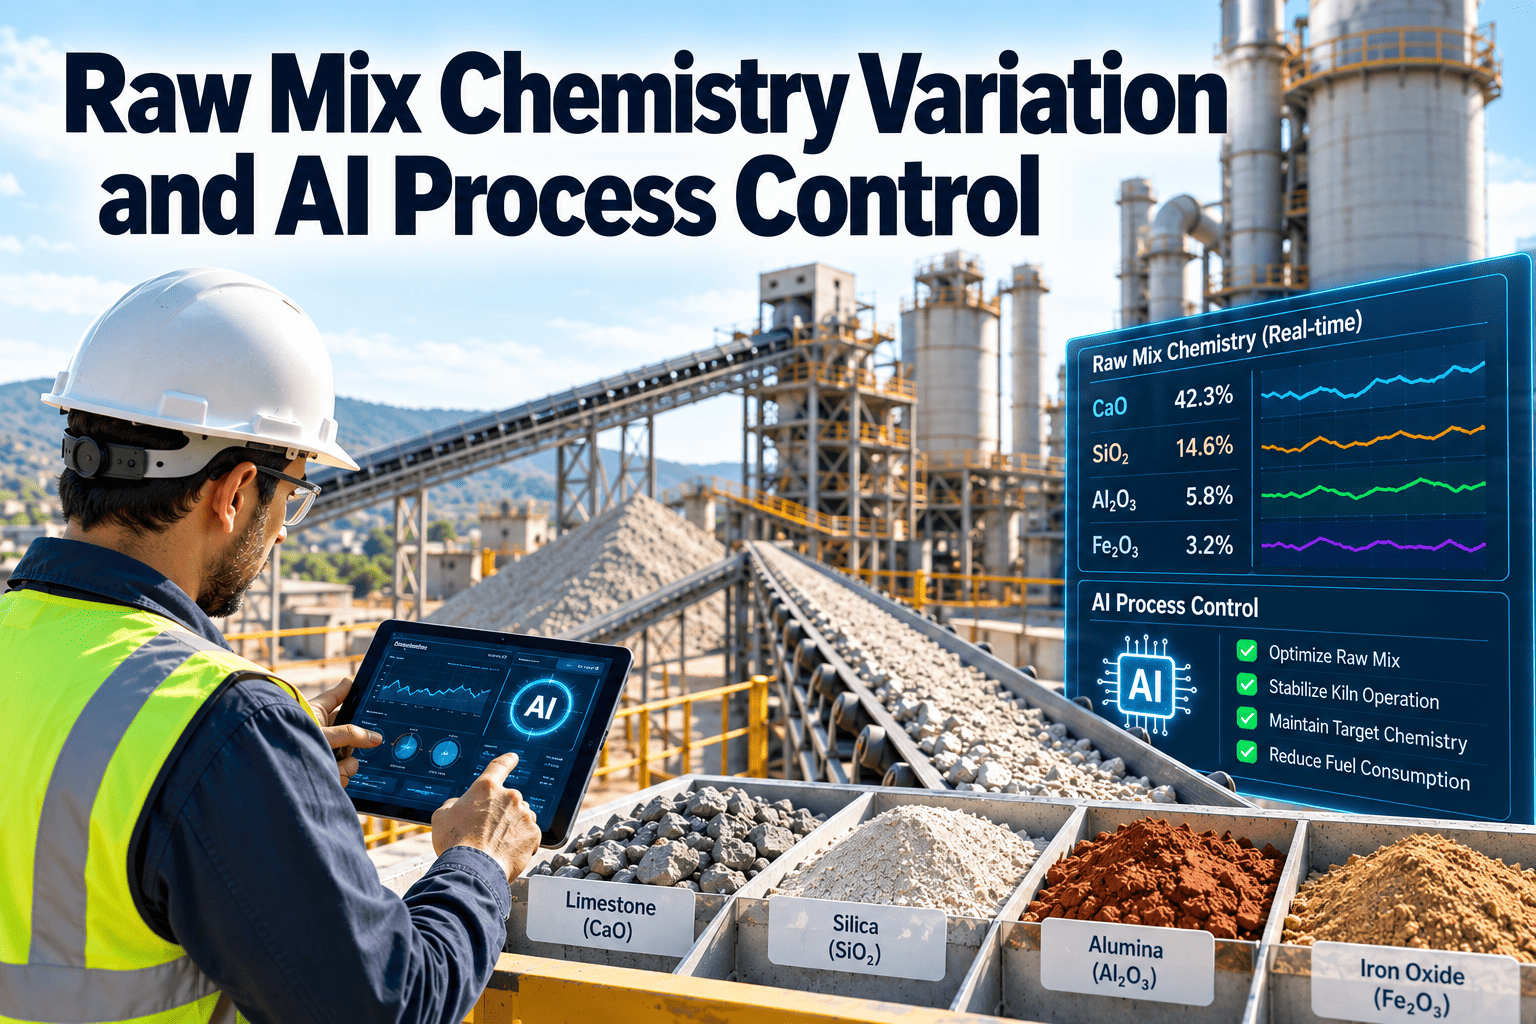
Stable kiln operation starts upstream. When raw mix chemistry swings, the kiln must be steered around it, with more fuel, more operator interventions and less consistent clinker. Variation comes from the quarry, from blending and from the equipment that feeds, mills and measures the mix, which makes it both a process problem and a maintenance problem. This guide explains the main sources of variability, how online analysis and AI process control reduce it, and why reliable feeders, analysers and blending equipment decide whether control strategies deliver the benefit they promise.
Raw Mix Chemistry Variation and AI Process Control
Variation in lime saturation factor, silica modulus and alumina modulus directly affects burnability, fuel use, coating behaviour and clinker strength. See where variation arises, how AI control reduces it, and which assets must stay reliable for control to work.
The real cost of raw mix variability
Every deviation in chemistry forces a response somewhere downstream. The cost accumulates in fuel, quality and stability, even if no single event looks serious.
Kiln stability and operator workload
A raw mix that is harder to burn one hour and easier the next requires constant adjustment of fuel, feed and draft. These adjustments raise the risk of unstable burning, ring formation and build-up. Stable chemistry gives the kiln and the operators a predictable target and allows steady-state operation.
Fuel consumption and heat efficiency
To avoid undersintered clinker, operators often burn harder than the average mix requires, leaving a safety margin against the hardest batches. The wider the variation, the larger the margin and the higher the heat consumption. Reducing variation permits a smaller margin and a measurable fuel saving.
Clinker quality and cement performance
Variations in lime saturation, silica and alumina modulus change the phase composition of clinker, with effects on strength, setting and grindability. Customers and downstream cement mills experience the variation as inconsistent performance, which can force costly blending or adjustments.
Refractory life and coating behaviour
Unstable chemistry and temperature cause fluctuating coating, which thickens and sheds unpredictably, stressing the refractory lining. More stable feed lowers thermal cycling and helps extend refractory life, an area where process and maintenance goals clearly overlap.
Where raw mix variation comes from
To reduce variation, first find where it enters. Different sources have different time scales and call for different remedies.
Quarry geology and extraction
Limestone and clay quality change across the quarry face and with depth. Selective mining, blast planning and pre-blending plans determine how much variation reaches the crusher. Link geological models and quarry sampling to the plant chemistry targets, so planning is proactive.
Stockpiling and reclaiming
Stacking and reclaiming systems with poor layering or segregation create cyclic variation. Stacker and reclaimer condition, such as worn blades, misaligned booms or faulty positioning, directly affects blending efficiency. Maintain these assets as part of the quality chain, not only as handling equipment.
Weigh feeders and dosing accuracy
Feeders deliver limestone, clay, sand and iron corrective materials to the raw mill. Calibration drift, belt wear, build-up and sticking hoppers cause deviations from the commanded proportions that look like chemistry noise. Regular calibration and inspection pay back quickly.
Raw mill, silo and homogenisation effects
Mill fluctuations and silo extraction patterns affect how variation is smoothed or amplified. Homogenising silos reduce short-term variation if air systems and extraction arrangements work properly. Aeration pads, blowers and valves require routine checks to maintain homogenising performance.
AI control can only be as good as the instruments and feeders behind it. OxMaint tracks analyser calibration, feeder performance, sampler condition and blending equipment faults, so your process model always works with reliable inputs.
Measuring chemistry quickly and accurately
Control is limited by measurement. Fast, accurate and reliable chemistry data is the foundation of both manual and AI-based strategies.
Online analysers: PGNAA and XRF
Online analysers measure the chemical composition of the material stream, giving results in minutes rather than hours. They need stable sample presentation, clean windows or sources, correct calibration and monitoring of their health indicators. A drifting analyser feeds errors directly into the controller.
Sampling systems and sample preparation
For laboratory and cross-belt or cross-stream methods, representative sampling is crucial. Worn cutters, blocked chutes and poor preparation give biased results that look like process variation. Treat samplers as critical equipment, with defined inspection and cleaning tasks.
Laboratory correlation and bias checking
Compare online analyser results with laboratory results on a schedule and track the bias over time. A growing bias suggests analyser drift, calibration error or sampling problem. Keep the comparison data in one place so that the analyser model can be updated when justified.
Data quality, time stamps and validation
Controllers depend on valid data. Missing values, flatlined signals, time misalignment between feeders and analysers and unvalidated lab entries all degrade performance. Implement automatic checks, and flag questionable data rather than letting it enter the control loop.
How AI and advanced control tighten the loop
Advanced process control has long been used in cement. AI methods extend it with better prediction, adaptation and pattern recognition, but the basics of good instrumentation still apply.
From manual correction to automatic feedback
Traditional practice adjusts proportions after laboratory results arrive, which means the correction lags the disturbance. Automatic feedback using online analysis shortens the delay. This alone can lower variation, provided feeders respond accurately and consistently.
Feedforward and model-predictive control
Predictive controllers use models of the mill, silo and process delays, together with incoming chemistry data, to adjust feed proportions before the deviation reaches the kiln feed. They handle interactions between several moduli and constraints such as feeder limits. Their performance depends on the accuracy of the models and the health of actuators.
Soft sensors and machine learning
Machine learning models can estimate hard-to-measure quantities, such as upcoming kiln feed chemistry or burnability indicators, from available signals. They can also detect drift in analysers and equipment by comparing expected and actual behaviour. Validate models against laboratory data and retrain them when raw materials or equipment change.
Keeping people in the loop
Operators and quality engineers need to understand what the controller is doing and why. Provide clear displays, safe override options and a defined process for model updates. Adoption improves when the system explains its actions and when maintenance and operations agree who responds to alerts.
Why maintenance underpins process control
The best model cannot compensate for a feeder that sticks or an analyser that drifts. Equipment reliability is therefore a direct driver of chemistry stability.
Weigh feeder reliability and calibration
Track feeder accuracy, belt tension, load cell condition, hopper build-up and drive performance. Use scheduled calibration with test weights or material tests, and record as-found errors. Rising error rates predict when a feeder needs intervention before it harms control quality.
Analyser health and availability
Monitor source strength, detector condition, window cleanliness, cooling and sample flow. Trigger maintenance when diagnostics move outside limits, and track analyser availability as a KPI. Plan spare parts for sensitive components, since long repair times mean reverting to slower manual control.
Stacker-reclaimer and handling equipment
Failures in blending piles, conveyors and reclaimers produce abrupt chemistry changes or feed interruptions. Apply condition monitoring to gearboxes, drives and structures, and keep accurate position and weighing instrumentation, which the blending model needs to work.
Silo extraction, aeration and valves
Blocked aeration pads, failing blowers and sticky valves disturb homogenisation and extraction flow. Check pressure, flow and valve response regularly, and include inspection of internal conditions during planned shutdowns.
Implementing a variation reduction programme
Plants that succeed usually follow a sequence: understand, repair, control and sustain.
Baseline the variation
Calculate the standard deviation and percentage within target for LSF, silica modulus and alumina modulus at several points, from quarry to kiln feed. Compare short-term and long-term variation to identify where the biggest reductions are available.
Fix instruments and actuators first
Calibrate feeders, verify analysers, repair samplers and correct handling issues before investing in advanced control. Many projects discover that most of the early gain comes from restoring equipment to design condition.
Pilot and expand control
Start with a well-defined loop, such as raw mill feed proportioning, and prove the benefit with before and after data. Expand to additional loops, constraints and optimisation targets after the results are accepted by operations.
Govern, measure and sustain
Assign owners for models, instruments and data quality. Track KPIs such as variation, kiln feed chemistry stability, fuel use per tonne of clinker and analyser availability. Review them regularly, and link any degradation to maintenance records to find root causes.
Raw mix variation: sources and corrective actions
Match each symptom to its likely source before choosing a remedy.
| Source of Variation | How It Appears | Typical Cause | Corrective Action |
|---|---|---|---|
| Quarry feed | Slow drift in LSF over days | Changing face composition or poor blending plan | Adjust mining plan, update model targets |
| Stockpile blending | Cyclic swings over hours or shifts | Poor stacking, segregation, reclaimer faults | Review stacking pattern, repair stacker-reclaimer |
| Weigh feeders | Short-term noise and proportion errors | Calibration drift, build-up, belt wear | Calibrate, clean, inspect wear parts |
| Online analyser | Sudden steps or slow bias against the lab | Detector, source or sampling issue | Verify against lab, service analyser, check sampler |
| Homogenising silo | Poor smoothing of incoming variation | Blocked aeration, valve faults | Inspect pads, blowers and valves |
| Raw mill operation | Fluctuating mill output chemistry | Mill instability, feed interruptions | Stabilise mill, review control loops |
Frequently Asked Questions
What causes raw mix chemistry variation?
Common sources are quarry heterogeneity, poor pre-blending, feeder inaccuracy, analyser errors, mill fluctuations and silo behaviour. Identifying which dominates in your plant guides where to invest, and a simple variance breakdown from quarry to kiln feed is often the best starting point.
How does AI improve raw mix control?
AI and model-predictive controllers use trends, models and online analysis to adjust feed proportions ahead of deviations, rather than correcting after the fact. They can also detect drift and anomalies. The gains depend on data quality and on actuators that respond as commanded.
Why does maintenance matter for process control?
Controllers assume feeders deliver correctly and analysers read accurately. If those assets drift or fail, the model optimises on false information. Tracking them in a CMMS with calibration schedules, health indicators and failure history protects control performance.
Which KPIs should we track?
Monitor standard deviation of LSF and moduli, percentage of time within target, feeder accuracy, analyser availability, bias against the laboratory, fuel consumption per tonne of clinker and kiln stability indicators. Together they show both quality results and the reliability of the supporting equipment.
How quickly can a plant see results?
It depends on the starting condition. Repairing instruments and feeders can show benefits within weeks, while advanced control projects usually need months for modelling, pilot testing and operator adoption. Establish a baseline first so that improvement can be demonstrated rather than assumed.
Do we need new analysers to use AI control?
Not always. Many plants first improve the performance and maintenance of existing analysers and samplers, and only then add instruments where gaps remain. Assess the accuracy, availability and response time of current measurements before buying new equipment.
How do we handle changes in raw materials or fuels?
Treat every significant change in quarry zone, corrective material or fuel as a trigger to review models, targets and calibration. Compare analyser and laboratory results closely for the first weeks, retune controllers where behaviour has shifted, and record the change and its effects, so that later teams can understand why settings were altered.
What role does the laboratory play once online analysis is installed?
The laboratory remains the reference. It validates analyser accuracy, provides detailed checks on chemistry and trace elements, and supplies data for model updates. Keep sample handling, preparation and instrument calibration under the same scheduled maintenance discipline as the online equipment, since an error in the reference method undermines everything compared against it.
How can maintenance data help find the cause of chemistry swings?
Overlay feeder faults, analyser alarms, reclaimer stops, silo events and mill trips on the chemistry trend. Many apparent process disturbances line up with a specific equipment event, such as a feeder calibration drift or a blocked sampler. Storing these events with accurate time stamps in a maintenance system makes the pattern visible, and turns root cause analysis into a routine activity instead of a special project.
What is a realistic first target for variation reduction?
Set the first target from your own baseline rather than from a published figure. A common approach is to aim for a measurable cut in the standard deviation of kiln feed LSF within the first quarter, using quick wins such as feeder calibration, sampler repair and analyser verification. Once the improvement is proven and sustained, raise the target and extend it to silica and alumina moduli, using the same measurement method so that results stay comparable over time.
Stabilise the Mix, Stabilise the Kiln
OxMaint keeps the analysers, feeders and blending equipment behind your AI control reliable, so chemistry stays on target, fuel margins shrink and the kiln runs steadier.
Free 14-day trial · No credit card