A chiller tube can lose much of its wall to erosion, pitting, or corrosion while the machine still looks healthy on the control panel. By the time refrigerant and water cross over, the repair is a shutdown, a cleanup, and often a lost cooling season. Eddy current testing inspects tube walls from the inside and finds thinning long before rupture. This guide covers when to test, what the results mean, and how to schedule it with preventive maintenance software so inspections are never forgotten.
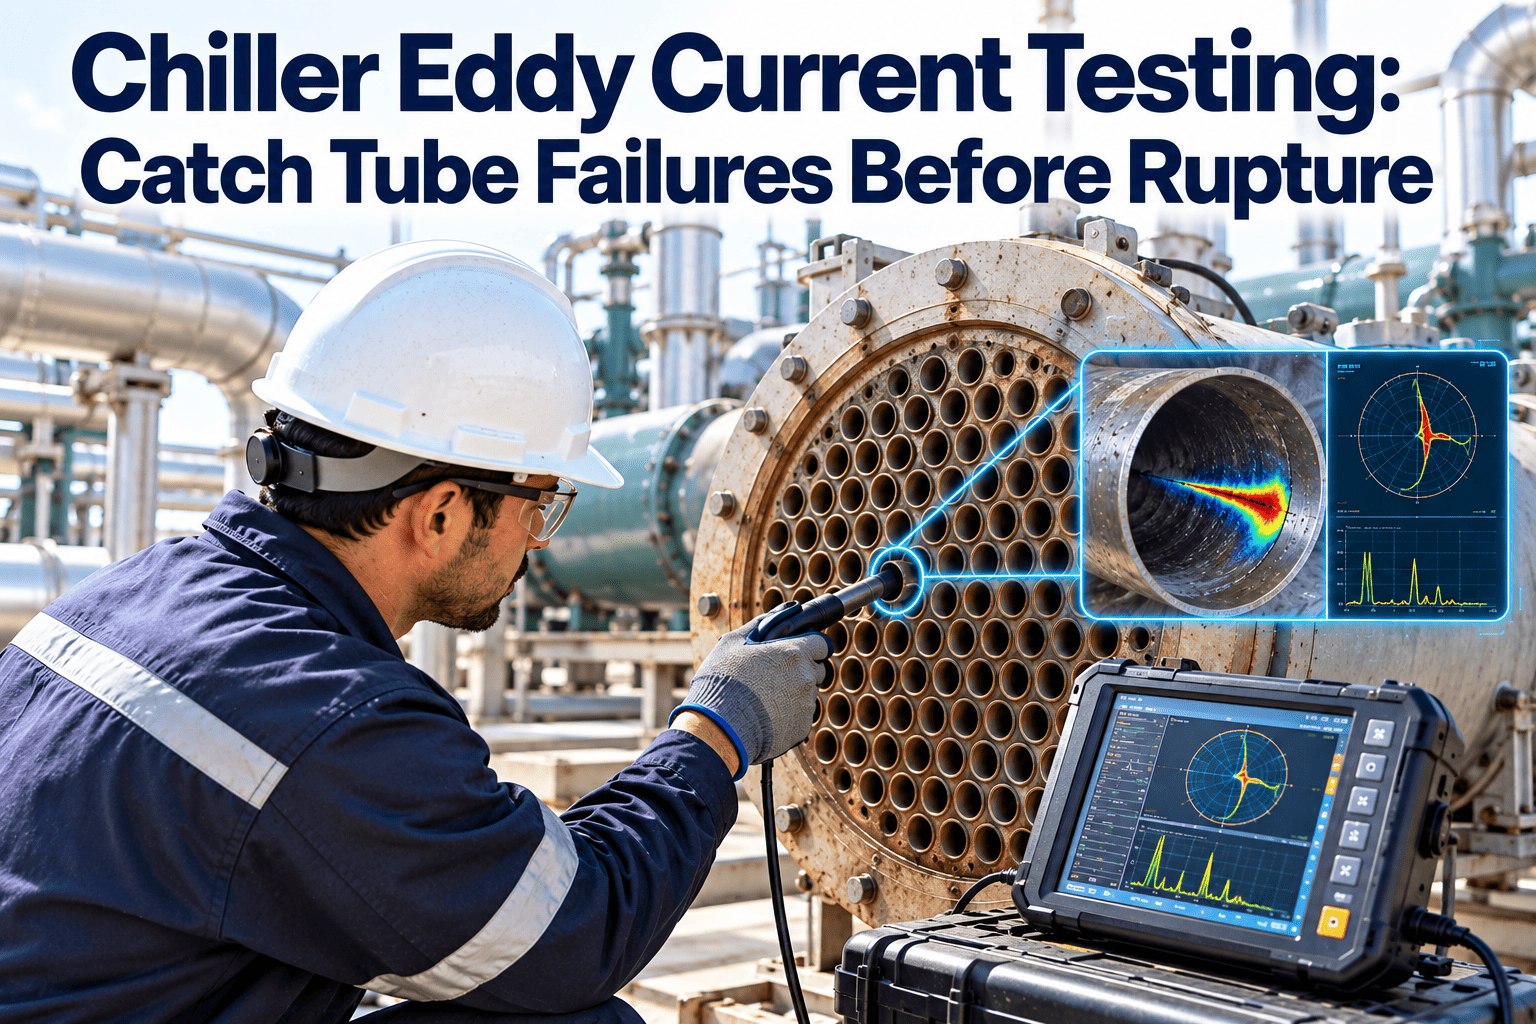
Chiller Eddy Current Testing: Catch Tube Failures Before Rupture
Eddy current testing turns hidden tube wall loss into a measured trend, so plugging and retubing become planned work instead of an emergency.
New tube
Year 5 test
Year 10 test
Plug or retube
Why tube failures surprise facility teams
- Tubes sit inside the shell and cannot be seen during routine rounds
- Thinning is local, so averages like approach temperature may look normal
- Failures often start at supports, inlets, or deposits where water flow is uneven
- A leaking evaporator tube can send water into the refrigerant circuit and damage the compressor
- Condenser leaks can contaminate water or lose refrigerant, depending on pressure
Pass-fail limits come from the chiller manufacturer, the tube material, and the inspector, not from a generic guide.
How eddy current testing works
Clean tubes
Insert probe
Pull through tube
Compare signal to reference
Report wall loss
A probe induces eddy currents in the tube wall. Defects such as wall loss change the electrical response, which the technician compares with calibration standards.
- Works well on non-ferromagnetic tubes such as copper alloys
- Ferromagnetic tubes, like carbon steel, need other techniques such as remote field testing
- Tubes must be clean, so cleaning is part of the test plan
Standards and documentation to reference
ASME Section V
Provides the nondestructive examination methods, including requirements for eddy current examination of tubular products.
TEMA
Heat exchanger construction and tube standards, useful for understanding tube layout, materials, and tolerances.
Manufacturer limits
Define plugging or replacement criteria for your specific model and tube material.
Test cadence: baseline first, then a trend
A
Baseline
Test new or recently retubed units to document the starting condition.
B
Routine interval
Many facilities test every few years. Set it by tube material, water quality, and run hours.
C
Shortened interval
Test more often after poor water treatment, known fouling, or earlier tube failures.
D
Event-driven test
Test after a tube leak, a major cleaning, or an unexplained loss of refrigerant or efficiency.
Schedule tube testing before the failure schedules you
Set test intervals, assign vendors, and keep reports attached to each chiller record.
Common tube damage mechanisms
| Mechanism | Typical cause | Where it appears | Maintenance response |
|---|---|---|---|
| Pitting | Deposits, poor water chemistry | Under scale or in low-flow areas | Improve water treatment and cleaning |
| Erosion at inlet | High velocity, debris, air | Tube ends near the water box | Check strainers and flow rates |
| Support wear | Vibration at tube supports | Mid-tube at support plates | Review flow and operating conditions |
| General wall loss | Corrosion, aggressive water | Along the tube length | Adjust chemistry, plan retubing |
| Cracking | Stress, freeze events | Near rolled joints or damaged areas | Investigate cause, plug affected tubes |
Reading results: what to ask the inspector
How was the probe calibrated and on what reference tube?
What is the percentage wall loss and location for each flagged tube?
Which tubes were not inspected or could not be passed?
What plugging criteria were applied, and who set them?
How do results compare with the previous test?
Which tubes are close to the limit and need earlier retest?
Plugging reduces heat transfer area. Track the plugged tube count and total share per chiller, and discuss capacity impact with the manufacturer.
A practical test workflow
1
Plan the outage
Pick a period of low cooling load and check the redundant capacity can carry the building.
2
Isolate and drain
Lock out the chiller and open the water boxes per site procedure.
3
Clean tubes
Brush or flush so the probe reads the wall, not the deposit.
4
Test and mark
Inspect every tube and mark those that need plugging or follow-up.
5
Repair and close
Plug, rebox, leak test, and return to service.
6
Record and trend
Attach the report and update the next test date.
Pair eddy current with other chiller condition data
- Approach temperatures and delta-T trends to spot fouling between tests
- Condenser and evaporator pressure trends
- Refrigerant top-ups, which may signal leaks
- Oil analysis and vibration readings on the compressor
- Water treatment logs for conductivity, pH, and inhibitor levels
- Strainer and filter inspection records
No single test explains a chiller. Combining readings lets you decide whether to clean, treat water, retest, or retube.
KPIs for tube integrity
Tests on schedule
Plugged tube share by chiller
Wall loss trend per test
Unplanned tube leaks
Refrigerant added per year
Water treatment compliance
How Oxmaint supports chiller testing programs
- Chiller asset records with tube material, install date, and test history
- Preventive maintenance schedules for tube cleaning, water treatment checks, and test dates
- Work orders that attach vendor reports and plugging records
- Condition-based workflows that open inspections when readings drift
- Dashboards for overdue tests and critical asset status
Frequently asked questions
How often should chiller tubes be tested?
It depends on material, water quality, and history. Set intervals with your inspector.
Does eddy current work on all tubes?
It suits non-ferromagnetic tubes. Steel tubes may need other methods.
Do tubes need cleaning before testing?
Yes. Deposits hide defects and reduce signal quality.
How do we remember the next test?
Use recurring schedules. Try Oxmaint for reminders and records.
Can we build a testing plan?
Yes. Book a demo to see chiller asset workflows.
Turn tube inspections into a managed program
Track chiller tests, results, and follow-up work so wall loss never reaches rupture.