Confectionery plants run on small tolerances. A chocolate that leaves the tempering machine a degree or two off can bloom on the shelf, a depositor that over-fills by a fraction wastes product all week, and a wrapper that misregisters film turns premium product into rework. Sugar, cocoa, fat, and heat also make these lines messy and hard on equipment. This guide covers tempering, depositing, and wrapping maintenance, and shows how Oxmaint maintenance management software can keep preventive tasks and quality-linked records together.
Confectionery Manufacturing Plant Maintenance: Tempering, Depositing, and Wrapping Under Control
Where Confectionery Lines Lose Time and Quality
Most confectionery losses are not dramatic breakdowns. They are repeated small events that add up across shifts: stringing at the depositor, bloom complaints, and wrapper jams.
Chocolate Tempering Equipment Maintenance
Tempering depends on accurate heating, cooling, and agitation. Real recipes set the exact temperatures, but the machine has to deliver them consistently.
What to inspect and when
| Component | Failure effect | Preventive task | Suggested trigger |
|---|---|---|---|
| Temperature sensors | False readings lead to over- or under-tempered chocolate | Verify against a reference thermometer and record deviation | Calendar, plus after any repair |
| Water circuit valves and pumps | Poor control of heating and cooling stages | Check valve response, flow, and leaks | Monthly or by running hours |
| Scraper blades and augers | Uneven heat transfer, build-up, poor mixing | Inspect for wear, fatigue, and clearance | Running hours |
| Chocolate pumps and seals | Leaks, fat contamination, flow variation | Inspect seals, lubricate, check motor load | Weekly check, seal change by condition |
| Heating elements and thermostats | Slow heat-up and uneven hold temperature | Test electrical values and controls | Quarterly |
| Refrigeration for cooling stage | Unstable crystallization and bloom risk | Check refrigerant, filters, and cooling water | Monthly |
Record a temper check result, such as a temper meter reading, in the same work order history so quality and maintenance see the same trend.
Depositor Maintenance: Accuracy Is a Maintenance Output
Depositors meter product into moulds, trays, or starch beds. Dosing accuracy comes from the condition of pistons, valves, nozzles, and drives.
Weigh and compare
Collect deposit weights at set intervals and compare against target and tolerance.Look for patterns
Check whether variation affects one nozzle, one lane, or the whole head.Inspect wear parts
Examine pistons, seals, rotary valves, and nozzle plates for scoring or leaks.Check drives
Review servo drive settings, belts, and cams that control stroke and timing.Record and verify
Log the repair, re-weigh after restart, and attach results to the work order.Typical depositor problems
- Stringing or tailing caused by cooling, nozzle wear, or incorrect cut-off timing
- Dripping between cycles from valve seat wear or heater faults
- Inconsistent weights from piston seal wear or entrained air
- Blocked nozzles from cold spots or product build-up
- Heated manifold failures that change viscosity along the line
Tie Depositor Weights and Tempering Checks to Maintenance Records
Wrapping Machine PM: Registration, Sealing, and Cutting
Wrapping machines run at high speed and tolerate very little variation. Many stops start with small wear in a few repeating components.
Flow and fold wrappers
- Sealing jaw surfaces, temperature, and pressure
- Cutting knives and anvils
- Film tracking rollers and web tension
- Print registration sensors and photo-eyes
- Infeed belts, lugs, and chain wear
Twist and bunch wrappers
- Gripper and twisting head wear
- Cam followers and linkage play
- Film feed and cutter timing
- Pocket or wheel condition on the infeed
- Lubrication points exposed to sugar dust
Wrapper failure signals to log
- Film jams near the cut-off or fin seal
- Registration marks drifting across consecutive packs
- Seal leaks or weak peel at one jaw position
- Product orientation errors at the infeed
- Repeated sensor faults after washdowns
Sugar, Cocoa, and Fat: Residue That Eats Equipment
Confectionery residue changes how equipment wears. Sugar crystallizes in bearings and chains, cocoa dust clogs sensors, and fat attracts dirt.
Changeovers and Allergen Control in Maintenance Work
Product changes introduce risk for cross-contact, particularly where nuts, milk, or other allergens are handled. Maintenance can help or hurt depending on how work is controlled.
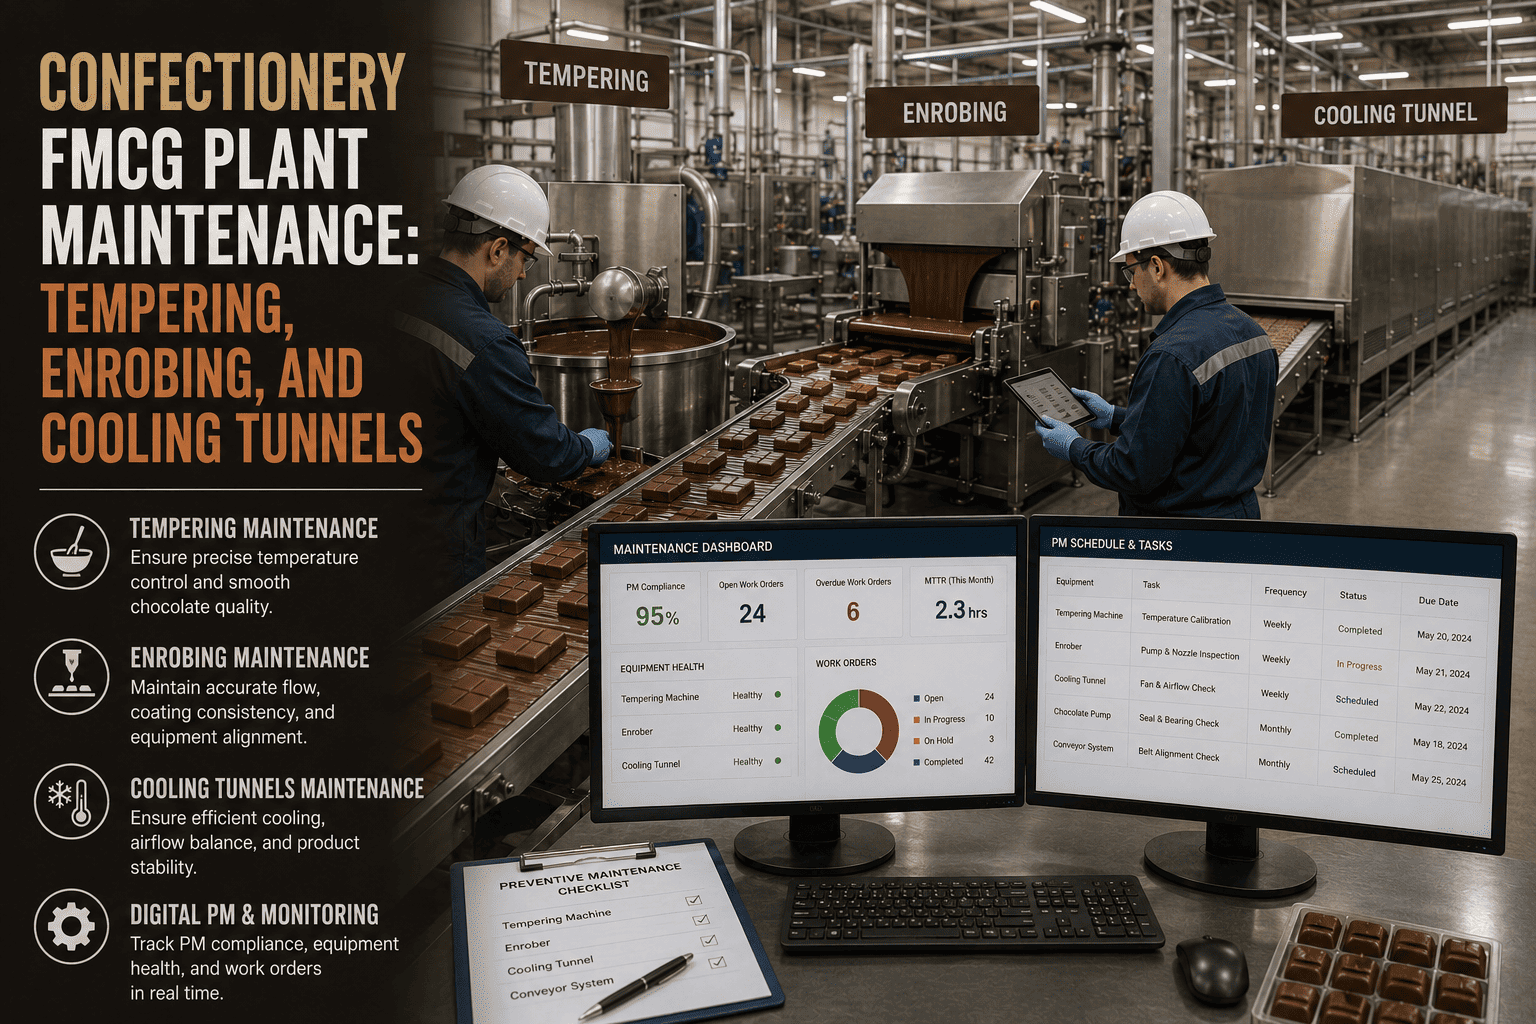
Cooling Tunnels, Enrobers, and Moulding Lines
Downstream equipment influences how well the carefully tempered chocolate actually sets. Cooling and shaping deserve their own preventive tasks.
| Equipment | Maintenance focus | Quality link |
|---|---|---|
| Cooling tunnel | Evaporators, fans, belt tracking, and temperature zones | Gloss, snap, and bloom resistance |
| Enrober | Chocolate curtain, vibration table, bottom roller, and blower | Coating weight and surface finish |
| Mould line | Mould conditioning, shakers, demoulding, and conveyors | Shape accuracy and release |
| Starch or bed systems | Handling, conditioning, and sieve condition | Product shape and cleanliness |
Mobile Checklists That Match Confectionery Routines
Short, specific checklists are more likely to be completed than long generic ones. Match each checklist to a machine and a moment in the shift.
Start of shift
- Verify temper stage temperatures
- Weigh sample deposits
- Inspect wrapper jaws and film path
- Check air, water, and chocolate supply
Mid-shift
- Review nozzle cleanliness
- Check for stringing or dripping
- Inspect wrapper registration
- Listen for abnormal noises
End of shift
- Record downtime causes
- Report parts needing attention
- Confirm cleaning completed
- Hand over open issues
Using Oxmaint to Organize Confectionery Maintenance
Different tasks need different triggers. A confectionery plant benefits from mixing calendar, run-hour, and inspection-driven schedules.
KPIs for Confectionery Maintenance Teams
Seasonal Peaks and Spare Parts Planning
Holiday and gifting seasons stretch capacity and tolerance for failure. Plan ahead so a wearing part is not discovered at peak volume.
- Review wear parts on seasonal lines several weeks before demand rises
- Stock nozzle plates, piston seals, and jaw kits for critical depositors and wrappers
- Pre-schedule calibration of temperature sensors and scales
- Plan overhauls of cooling tunnels before warm-weather load
- Use work order history to see which parts failed during the last peak
Beyond Chocolate: Gummy, Hard Candy, and Panned Lines
Many confectionery plants run more than one process family. Each family wears equipment differently, so one maintenance template rarely fits all lines.
| Process family | Equipment under most stress | Maintenance priority |
|---|---|---|
| Gummies and jellies | Cookers, depositors, starch handling, drying rooms | Temperature control, nozzle condition, starch conditioning, humidity control |
| Hard candy | Vacuum cookers, cooling tables, forming and cutting units | Vacuum integrity, heat transfer surfaces, die and cutter wear |
| Panned products | Pans, syrup spraying, drying air, drives | Spray nozzle condition, drive and gearbox health, air handling filters |
| Chewy and toffee lines | Cooking kettles, pullers, extruders, cutters | Gearbox load, scraper wear, blade condition, hot surface inspections |
Build the asset register by process family first, then let each family carry its own preventive task library.
Weighing, Checkweighing, and Detection Equipment
Quality equipment is also maintenance equipment. If a scale or detector drifts, the plant loses its ability to prove product is within specification.
- Calibrate scales and checkweighers using certified weights and record results
- Verify metal detectors or X-ray units with test pieces at the frequency your food safety plan requires
- Inspect rejection mechanisms, such as air blasts or pushers, for timing and wear
- Check belt condition and sensor alignment on inspection conveyors
- Record every failed verification and the corrective action in the same system as production equipment
From Repeated Wrapper Jam to Root Cause
A wrapper that jams every shift teaches the team to expect it. A structured response turns that pattern into a fix.
Utilities and Environmental Control
Temperature and humidity are part of the recipe in confectionery. Utility equipment should be on the PM plan alongside process machines.
Air and climate
- Air handling units and filters in packing and cooling areas
- Dehumidification equipment for sensitive products
- Temperature and humidity sensor calibration
Water, steam, and compressed air
- Hot water and chilled water circuits for tempering
- Steam traps and control valves on cookers
- Compressed air dryers and filters on packaging lines
Training, Handover, and Keeping Knowledge in the System
Confectionery lines often depend on a few experienced technicians who know every quirk. Work orders and checklists capture that knowledge before it walks out the door.
- Attach setting sheets, photos, and wear-part references to the asset record
- Use the work order notes to explain what was found, not just what was done
- Include short instructions on tasks that are easy to do incorrectly
- Review repeat repairs in team meetings and update checklists as a result
A 30-Day Starter Plan for a Confectionery Plant
A full program does not have to launch at once. These first steps give the team early wins and clean data.
Week 1
List critical assets on one pilot line, including tempering, depositing, and wrapping equipment.Week 2
Load existing PM tasks and add the sensor verification and wear-part inspections that were missing.Week 3
Start mobile checklists for operators and technicians, and code every stop with a reason.Week 4
Review the first month of downtime, rework, and overdue tasks, then adjust the schedule.Confectionery Maintenance FAQs
How often should tempering sensors be verified?
Set the interval by recipe sensitivity and drift history, and record each check in Oxmaint.
What causes depositor weight variation?
Common causes include worn pistons or seals, nozzle build-up, air in the product, and unstable heating. Weight trends point to the cause.
Can a CMMS help with wrapping machine jams?
Yes. Logging jam locations and causes shows which jaws, knives, or sensors are driving repeat stops.
How do we manage allergen risk during repairs?
Include controlled tool use, cleaning, and verification steps on the work order so they are completed and recorded.
Can we try this on one line first?
Yes. Book a demo to plan a pilot on a single line or machine.