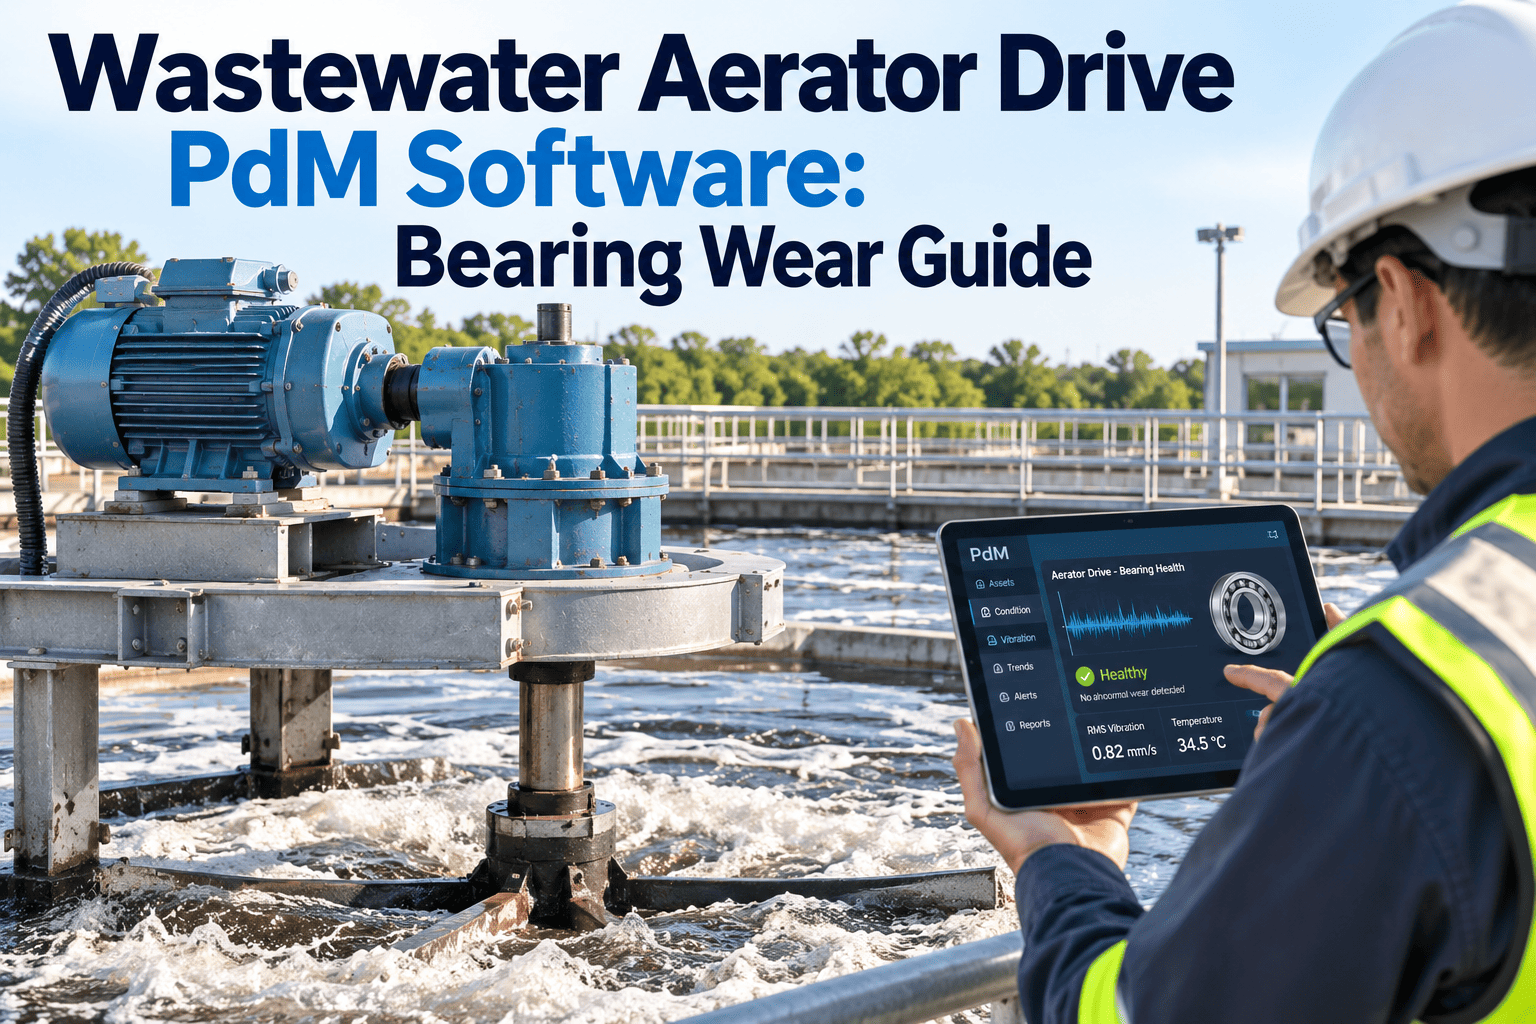
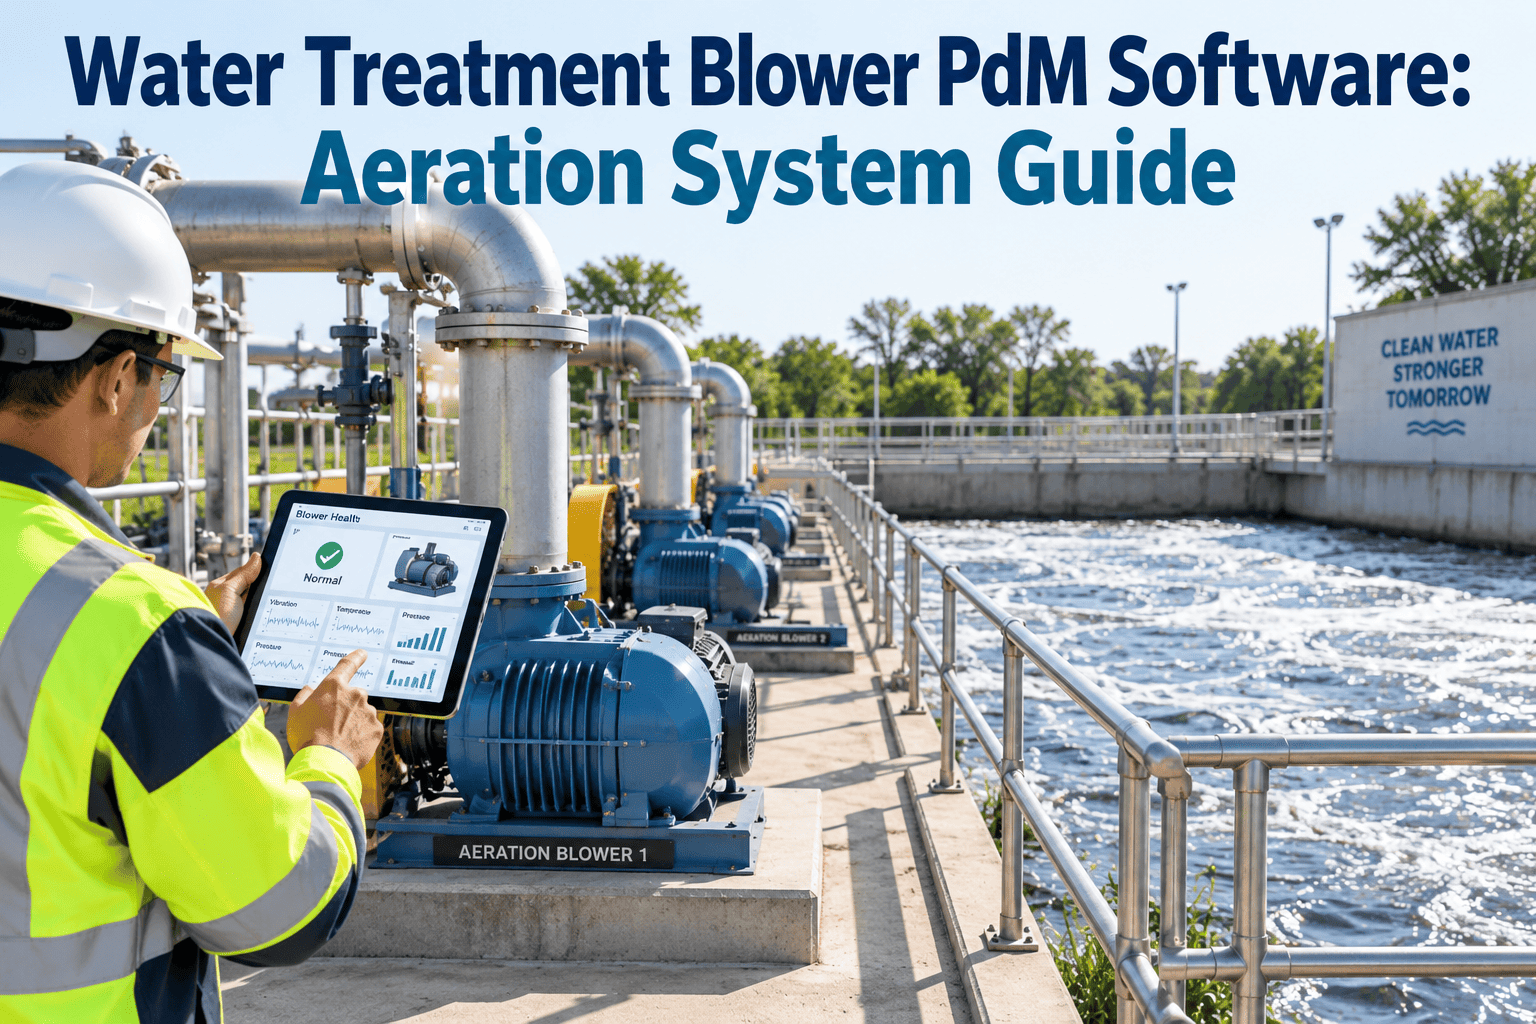
A surface aerator does not fail gracefully. Bearing wear inside an aerator drive, a mechanical mixer gearbox, or a diffused air blower begins quietly — a few extra microns of clearance, a slightly elevated running temperature, a faint tone in the vibration spectrum — and ends with a seized shaft, a dropped rotor, or a blower that will not spin up during a critical loading event. Every hour that basin sits without full aeration, dissolved oxygen falls, nitrification stalls, and the plant moves closer to a permit exceedance that regulators and the public will notice. Wastewater treatment plants running fixed maintenance intervals on aeration drive trains are, in effect, guessing at the one variable that determines whether the activated sludge process keeps working: bearing condition. Predictive maintenance software built on continuous condition monitoring changes that guess into a measurement, and CMMS-driven aeration PdM is becoming the baseline expectation for any plant that cannot afford an unplanned aerator outage — book a free aeration reliability assessment with our wastewater engineering team to see where your drive trains stand today.
70%
of rotating equipment failures in WWTPs trace back to bearing degradation that went undetected between inspection rounds
3–6 mo
typical early-warning window a vibration and temperature PdM program provides before a bearing reaches functional failure
40%
average reduction in unplanned aeration downtime reported by plants after moving from calendar-based to condition-based drive maintenance
24/7
continuous coverage needed since DO demand and blower loading shift constantly with influent flow and organic load
Stop Guessing When Your Aerator Bearings Will Fail
Oxmaint connects vibration sensors, thermal probes, and motor current data straight into work orders — so a developing bearing fault turns into a scheduled repair instead of an emergency call at 2 a.m.
Why Aerator Drive Bearings Fail — And Why the Symptoms Hide So Well
Surface aerators, mechanical surface mixers, and diffused air blowers all share the same vulnerable point: a rotating shaft supported by bearings that must survive continuous duty, submerged or humid environments, and constant torque reversals as loading changes. Bearing wear rarely starts as a dramatic event. It begins as micro-pitting on a raceway, a small increase in radial play, or the first signs of lubricant film breakdown. None of these are visible from the catwalk. An operator walking the aeration basin can hear a badly failing bearing, but by the time a bearing is audibly loud, it has typically already lost a significant portion of its remaining service life and is running on borrowed time.
The consequence of a missed bearing failure in an aeration system is disproportionate to the size of the part. A single seized bearing on a surface aerator can drop dissolved oxygen across an entire basin within an hour, disrupting nitrification and pushing effluent ammonia above permit limits. On a mechanical mixer, bearing seizure risks solids settling and septic conditions developing in the affected zone. On a diffused air blower, bearing failure can mean a complete loss of air supply to a basin bank with no redundancy path, forcing an emergency bypass or a call to the state regulator. None of these outcomes are proportional to the cost of the bearing itself — they are proportional to the plant's inability to see the failure coming.
Manual Rounds vs Continuous Condition Monitoring on Aeration Drives
Most plants still rely on operator rounds — a technician walks the aeration basins on a set schedule, feels for vibration by hand, listens for unusual sound, and checks a bearing housing temperature with a handheld gun. This catches gross failures. It almost never catches developing ones, because the interval between rounds is exactly the window in which a bearing can progress from early-stage wear to catastrophic failure.
| Detection Method |
Manual Rounds |
Continuous PdM Monitoring |
| Reading frequency |
Once per day or per shift, at best |
Every 1–15 minutes, all channels |
| Bearing temperature trending |
Single point-in-time reading |
Continuous trend against normal operating baseline |
| Vibration analysis |
Hand-held spot check, if equipment is available |
Fixed accelerometers with automated spectral analysis |
| Nighttime and weekend coverage |
Minimal to none |
Full coverage, all hours |
| Motor current signature |
Not typically captured |
Continuous current draw correlated to load and speed |
| Work order generation |
Manual, after the fact |
Automated from alert threshold directly into CMMS |
The Sensor Stack: What to Monitor on Every Aeration Drive
Vibration Monitoring
Accelerometers mounted at the bearing housing capture overall velocity and spectral signatures. Rising vibration amplitude at bearing defect frequencies is one of the earliest and most reliable indicators of raceway or rolling element wear on surface aerator gearboxes and blower shafts.
Bearing Temperature
RTD or thermocouple sensors embedded at the bearing housing track absolute temperature and, more importantly, the rate of temperature rise relative to ambient and load. A bearing running hotter than its established baseline at the same load is degrading internally even before vibration changes are obvious.
Motor Current Signature Analysis
Current draw on the aerator or blower motor reflects mechanical load on the shaft. Periodic current spikes or a slow upward drift in baseline current at constant process load can indicate bearing drag, coupling misalignment, or gearbox wear developing inside the drive train.
Oil and Lubricant Analysis
Particle counting and viscosity testing on gearbox oil samples reveal metal wear debris long before a bearing produces audible or measurable vibration symptoms, giving the earliest possible warning on gear-driven surface aerators and mechanical mixers.
Ultrasonic Acoustic Monitoring
High-frequency ultrasonic sensors detect the friction and impacting signatures of early bearing lubrication breakdown, often weeks before the same fault becomes visible in standard vibration bands, particularly useful on slower-turning surface aerator shafts.
Process Correlation Data
Dissolved oxygen, influent flow, and blower discharge pressure feed into the same platform so that a sensor reading is always interpreted against the actual operating condition of the basin, not in isolation.
Turn Sensor Data Into Scheduled Work, Automatically
A vibration spike at 2 a.m. is only useful if it reaches the right technician with the right work order attached. Oxmaint routes every aeration drive alert straight into a prioritized CMMS work order.
From Raw Sensor Reading to a Closed Work Order
1
Sensor Reading
Vibration, temperature, current, and oil data stream continuously from every aerator, mixer, and blower drive
2
Baseline Comparison
Each reading is compared against the expected value for current load, speed, and process condition
3
Anomaly Flagging
Deviations beyond the statistical threshold are flagged and cross-checked against related channels
4
Work Order Creation
A prioritized CMMS work order is generated automatically with the fault type, asset history, and required parts
5
Technician Dispatch
The nearest qualified technician receives the order on a mobile device with sensor history attached
Compliance and Reporting: Why Aeration PdM Matters Beyond the Bearing
Dissolved oxygen and effluent ammonia are directly regulated under most NPDES permits, and a state environmental agency does not accept a bearing failure as an excuse for a permit exceedance. Continuous aeration drive monitoring gives plant staff a documented, timestamped record showing when a bearing anomaly was first detected, when the work order was issued, and when the repair was completed — evidence that supports both internal reliability reviews and any regulatory inquiry that follows an aeration disruption. Plants that can show this documentation trail consistently face fewer follow-up findings during state inspections and build a stronger record for capital planning conversations with their governing board.
98%
Aeration Drive Monitoring Coverage — share of surface aerators, mixers, and blowers with active condition monitoring
< 2 hrs
Mean Time to Alert Acknowledgment — average time from anomaly detection to technician review
1.5–3x
Bearing Life Extension — typical gain when lubrication and alignment issues are corrected at early warning stage
0
Unplanned Basin Outages — target for any basin bank without built-in aeration redundancy
Frequently Asked Questions
What is the earliest reliable indicator of aerator bearing wear?
Vibration at bearing-specific defect frequencies and a slow upward drift in oil particle counts are typically the earliest measurable signs, often appearing weeks before any change in running temperature or audible noise becomes noticeable to plant staff.
How many sensors does a typical surface aerator need?
A functional setup usually includes one or two vibration accelerometers per bearing housing, a temperature sensor at each bearing, and current monitoring at the motor — enough coverage to correlate mechanical and electrical symptoms without overbuilding the sensor budget.
Can PdM software work with our existing SCADA and CMMS systems?
Yes, most aeration PdM platforms integrate with existing SCADA historians and CMMS work order systems rather than replacing them, pulling process context alongside sensor data —
sign up free to see how the integration maps to your current setup.
Does condition monitoring reduce the need for scheduled maintenance entirely?
No, it shifts the balance rather than removing scheduled work — lubrication, alignment checks, and inspection remain calendar-based, while bearing and gearbox replacement decisions move from a fixed interval to an actual condition trigger, avoiding both premature replacement and unexpected failure.
What does a typical aeration PdM rollout cost for a mid-size plant?
Sensor and platform costs vary with the number of drive units and existing instrumentation, but most mid-size plants recover the investment within one to two avoided unplanned outages, given the operational and compliance cost of a basin-wide aeration loss.
Give Your Aeration Drives the Monitoring They Need
From a single aerator to a full plant fleet, Oxmaint brings vibration, temperature, and current data together with automated CMMS work orders built for wastewater teams.