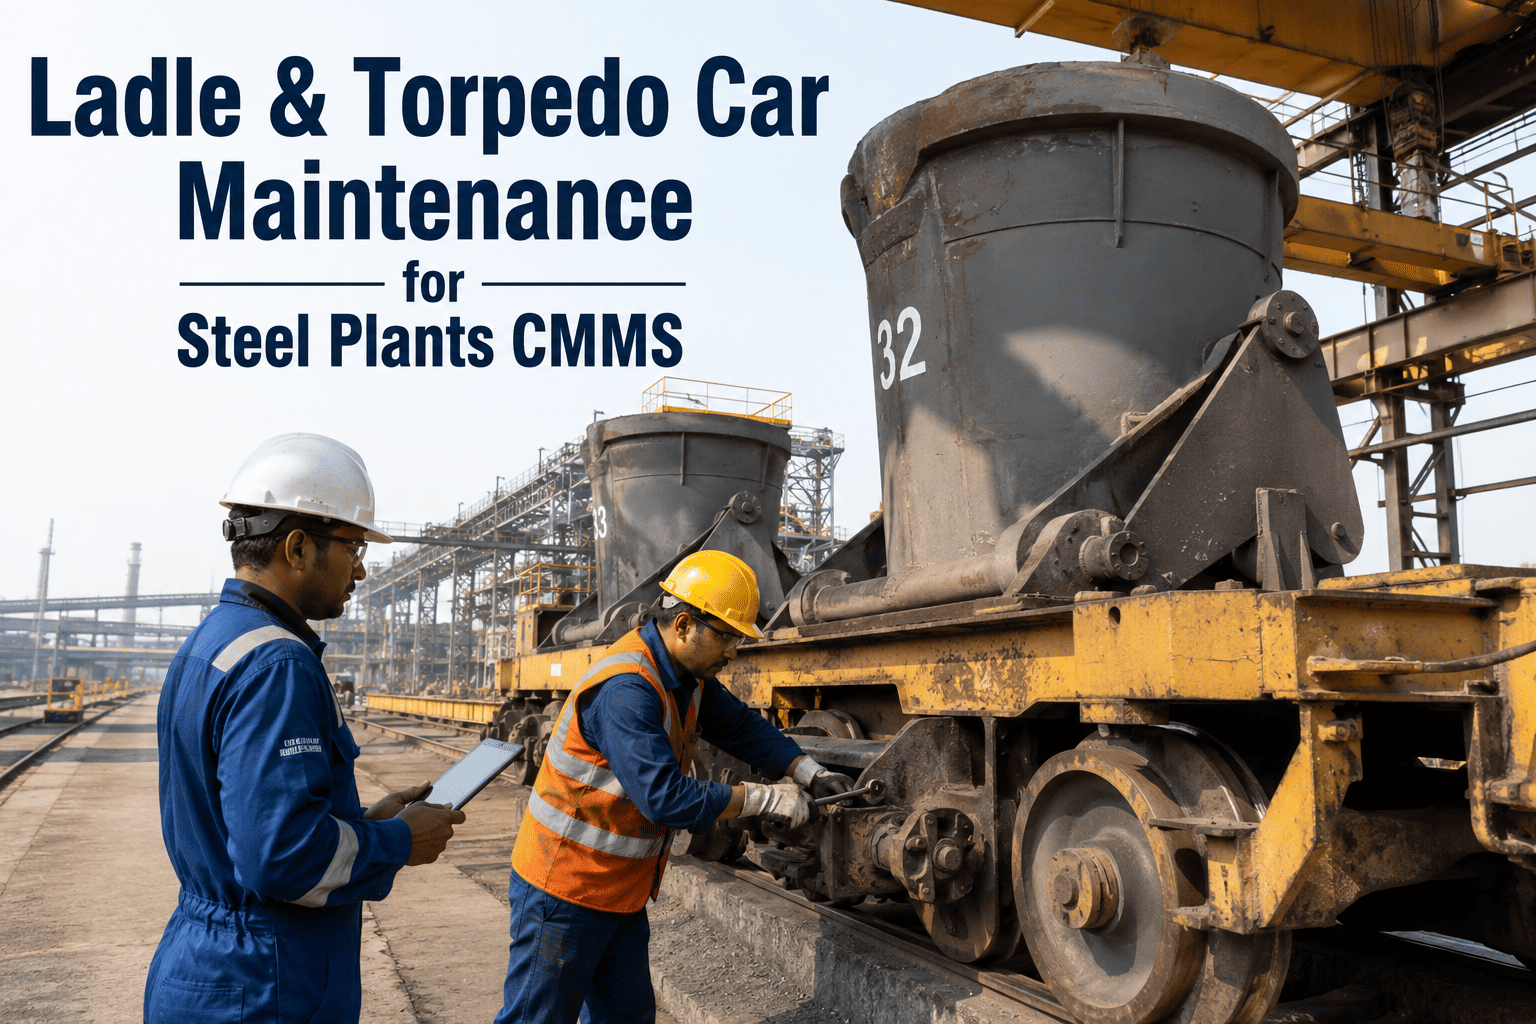
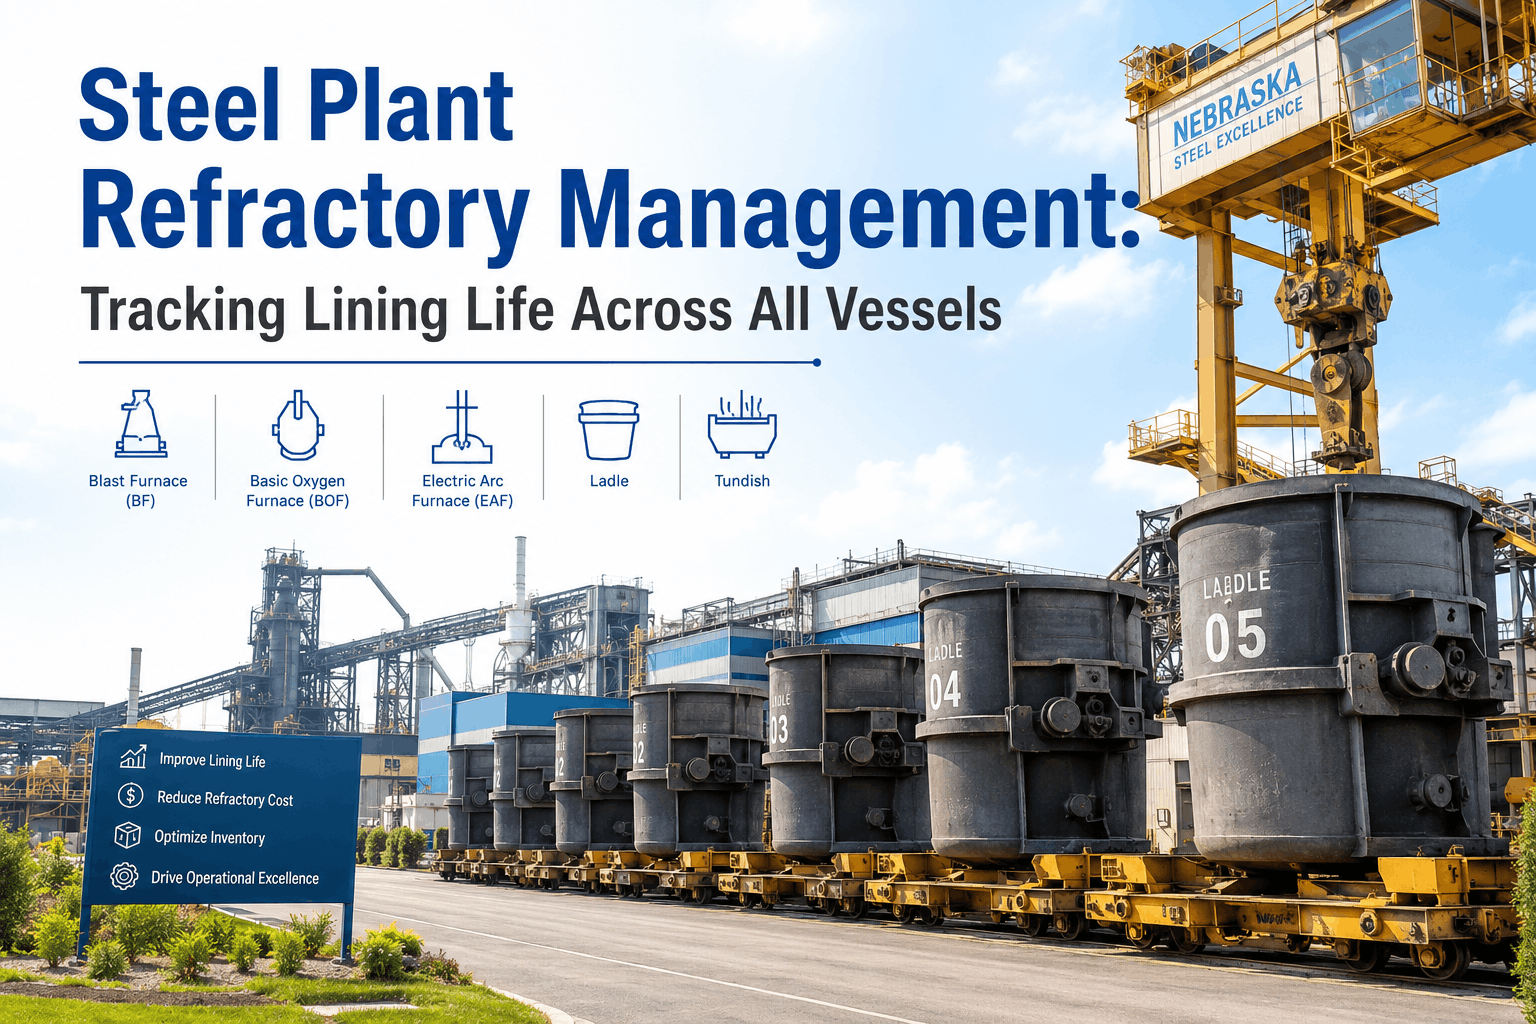
A ladle arriving at the ladle furnace with 420 heats on its refractory lining and no tracked inspection record is not an operational risk — it is a scheduled catastrophe. Secondary metallurgy sits at the highest-value point in the steelmaking route: chemistry corrections, temperature homogenisation, and inclusion flotation happen here before the ladle reaches the caster. A slide gate failure at pouring, a refractory breakout at the turret, or a decarburisation lance blockage in the vacuum degasser does not just halt one heat — it can halt a caster bay for days and write off tens of thousands of tonnes of in-process steel. Oxmaint tracks ladle life, slide gate cycles, and refining system PM in a single platform so every component in secondary metallurgy carries a current inspection record before the next heat begins. Book a demo to see ladle life tracking configured for your fleet.
Three Maintenance Gaps That Create Catastrophic Risk in Secondary Metallurgy
Secondary metallurgy handles liquid steel at 1,580°C under argon, vacuum, or oxygen-blowing conditions. Every component in the system — refractory brickwork, slide gate plates, stirring lances, alloy chutes, electrode arms — degrades on a use-cycle basis, not a calendar basis. Three failure modes explain why paper-based tracking creates compounding risk at production scale.
Without a digital heat counter tied to each ladle's asset record, the decision to reline is made on visual inspection alone — or not at all. Ladles in active rotation accumulate heats faster than paper logs can track. When a lining goes over its safe campaign limit undetected, the failure mode is a steel breakout: liquid metal through a compromised brick joint, reaching the ladle shell and potentially the crane bay. Sign up for Oxmaint to activate per-ladle heat cycle tracking.
Slide gate plates, collector nozzles, and upper tubes each carry a maximum actuator cycle limit before wear erosion compromises the seal. In a multi-strand caster bay running 24/7, a single gate can accumulate its maintenance threshold in under a week. Without cycle counting linked to individual gate assemblies, replacements happen reactively — after a steel runout at the ladle outlet, not before it. Book a demo to see slide gate monitoring in Oxmaint.
Ladle furnace electrode arms, vacuum degasser vessel linings, wire feeder drives, argon stirring plugs, and alloy addition hoppers are all maintained on separate schedules by separate teams using separate records. No single view shows which systems are due for inspection before the next production campaign begins. When a vacuum degasser vessel lining fails mid-treatment, the heat is scrapped and the degasser is offline. Sign up for Oxmaint to consolidate all secondary metallurgy PM records.
01Secondary Metallurgy Systems and Their Maintenance Requirements
Secondary metallurgy encompasses a range of refining processes — each with its own asset portfolio, wear mechanisms, and failure consequences. Effective maintenance requires tracking all of them in a unified system that connects heat cycles, inspection records, and PM work orders per asset rather than per process line.
Electrode arms and graphite electrodes degrade per arc-on hour. Roof refractories accumulate thermal cycling damage. The transformer, bus bars, and short-net system require periodic inspection tied to campaign heat count rather than calendar date. Alloy addition hoppers, weight feedometers, and pneumatic conveying lines for wire feeding all carry individual PM intervals that must feed into the same work order queue as electrode and refractory tasks. Sign up for Oxmaint to track LF electrode consumption and roof PM.
Vessel lining brick — particularly in RH snorkel zones and VD bottom walls — erodes on a heat-cycle basis with accelerated wear from temperature excursions and oxygen lancing. Snorkel refractory requires individual campaign tracking per vessel. Mechanical systems — vacuum pumps, steam ejectors, exhaust ducts, and rotary valves — carry time- and cycle-based PM schedules that must align with vessel relining windows. Book a demo to see vacuum vessel PM scheduling.
The ladle turret is under constant rotational load from ladle weights exceeding 300 tonnes per arm. Slewing bearing condition, pinion and rack wear, and hydraulic slewing drive PM are all tied to accumulated rotation cycles rather than fixed calendar intervals. Transfer car rail systems, coupling mechanisms, and electrical festoon systems carry their own inspection schedules. Failures here interrupt ladle delivery to the caster and cascade through the entire casting bay. Sign up for Oxmaint to track turret bearing cycles and hydraulic drive PM.
Argon stirring plugs embedded in ladle bottoms deteriorate with cumulative gas flow hours and thermal cycling. Clogged or eroded plugs reduce stirring efficiency directly, affecting inclusion removal and temperature homogeneity. Wire feeding systems — guide tubes, straightening rolls, and drive units — require inspection and replacement based on wire tonnage throughput. All of these consumable systems track on heat-count or throughput metrics, not calendar date. Book a demo to see stirring plug and wire feeder tracking.
02Ladle Life Tracking and Slide Gate Monitoring
Every ladle in the fleet is a high-value, high-risk asset that carries its full maintenance history through every heat. Oxmaint assigns a permanent asset record to each ladle shell — tracking heat count, refractory campaign status, repair events, slide gate cycle count, and scheduled inspection milestones in a single digital record that travels with the ladle regardless of which shift or which production line it serves.
Each ladle shell receives a unique asset ID in Oxmaint with configurable thresholds for: maximum heats per campaign before mandatory inspection, maximum heats between bottom purge plug replacements, maximum slide gate actuator cycles before plate replacement, and refractory thickness remaining at last measurement. Heat increments update automatically from production data integration or manual entry at heat completion. Sign up for Oxmaint to register your ladle fleet and configure heat cycle thresholds.
When a ladle approaches its configured heat threshold — for example, 80% of maximum campaign heats — Oxmaint automatically generates a pre-campaign inspection work order assigned to the refractory inspection team. The work order carries the current heat count, last measured lining thickness, previous inspection findings, and recommended inspection points. The ladle is flagged for inspection before it is returned to service for the next campaign. Book a demo to see threshold-triggered work order generation for your campaign parameters.
Each slide gate mechanism on the ladle outlet accumulates actuator cycles that erode the refractory plate, collector nozzle, and upper tube. Oxmaint tracks cumulative cycles per gate assembly against the manufacturer's recommended replacement interval. When a gate approaches its cycle limit, a replacement work order is generated automatically — scheduling the repair during the next planned ladle offline window rather than responding to a steel runout at the strand. Sign up for Oxmaint to configure cycle-based slide gate PM for your gate types.
When a ladle enters the repair bay for relining, technicians record the condition of each refractory zone — bottom, lower barrel, upper barrel, and slag zone — with thickness measurements, visual condition scores, and repair actions taken. These records feed back into the asset history alongside the heat count that triggered the repair, building a per-ladle dataset that progressively refines campaign length predictions and identifies ladle shells with accelerated wear patterns. Book a demo to see brick-zone inspection recording in Oxmaint.
The ladle fleet dashboard shows every ladle's current heat count, percentage of campaign limit consumed, slide gate cycle status, and days since last inspection — visible to production planners, refractory engineers, and plant management simultaneously. Ladles approaching their thresholds appear as amber warnings; ladles at or beyond their limit appear as red holds requiring inspection before next use. No ladle returns to service past its limit without a documented decision. Sign up for Oxmaint to activate the ladle fleet status dashboard for your operation.
03Paper-Based Ladle Tracking vs Oxmaint CMMS
The consequence gap between managed and unmanaged ladle maintenance is not marginal — it is the difference between a planned offline window and a liquid steel breakout in the casting bay. These are the operational differences between paper tracking and a connected CMMS for secondary metallurgy assets.
04Oxmaint Capabilities for Secondary Metallurgy Maintenance
Oxmaint's secondary metallurgy maintenance module combines ladle life tracking, slide gate cycle monitoring, and refining system PM into a single connected platform — with configurable thresholds per asset class and automatic work order generation when any component approaches its service limit.
Per-ladle digital records tracking cumulative heat count, refractory campaign progress, purge plug gas hours, and slide gate cycle accumulation. Configurable warning thresholds at 80%, 90%, and 100% of campaign limits trigger inspection work orders automatically at each level — preventing any ladle from exceeding its safe service limit without a documented inspection decision. Production data integration updates heat counts automatically at cast completion. Sign up for Oxmaint to register your ladle fleet and configure campaign tracking.
Individual slide gate assembly records tracking plate cycles, collector nozzle replacements, and hydraulic actuator service events. Cycle limits configurable per gate model and steel grade — high-calcium grades accelerate wear and require shorter intervals. When a gate reaches its threshold, a replacement work order generates automatically and is scheduled for the next planned ladle offline window rather than the next steel runout. Book a demo to see slide gate PM configuration for your gate supplier's specifications.
Individual vessel records for RH, VD, and VOD units tracking snorkel refractory heat count, vessel bottom wear zone measurements, oxygen lance consumption, and mechanical system PM — pump overhauls, ejector steam valve inspections, and exhaust duct lining. Campaign end prediction based on measured wear rate trends rather than fixed intervals, with automatic work order scheduling for planned vessel offline windows that align with caster maintenance schedules. Sign up for Oxmaint to configure vacuum vessel campaign tracking.
Every inspection, repair, relining, and replacement event is timestamped and stored against the asset record with technician sign-off and photo evidence. When a ladle breakout or degasser vessel failure occurs, the complete heat history — campaign heats, last inspection date, slide gate cycle count, prior repair records — exports immediately for root cause analysis and regulatory reporting. ISO 9001 and IATF 16949 traceability requirements satisfied automatically as a byproduct of normal workflow. Book a demo to see audit trail export for your quality system requirements.
05What Steel Plants Measure After Secondary Metallurgy CMMS Deployment
The measurable improvement pattern after deploying Oxmaint for secondary metallurgy maintenance follows a consistent sequence: ladle breakout incidents drop in the first quarter as campaign limits are enforced digitally; slide gate reactive replacements convert to planned work within 60 days as cycle counting begins; and vacuum degasser availability improves as vessel relining aligns with planned outage windows rather than surprise failures.
We had the ladle campaign limits in a binder on the refractory engineer's desk. Nobody read that binder at 2 AM when the ladle was in the queue. After Oxmaint, every ladle has a heat counter the caster operator can see before the heat is accepted. We went eleven months without an unplanned breakout event. The previous record was four months.
06Frequently Asked Questions
Every Ladle Should Know Its Heat Count Before It Enters the Bay.
Ladle life tracking. Slide gate cycle monitoring. Vacuum vessel campaign management. Turret and stirring system PM. Full audit trail. Live in two weeks.