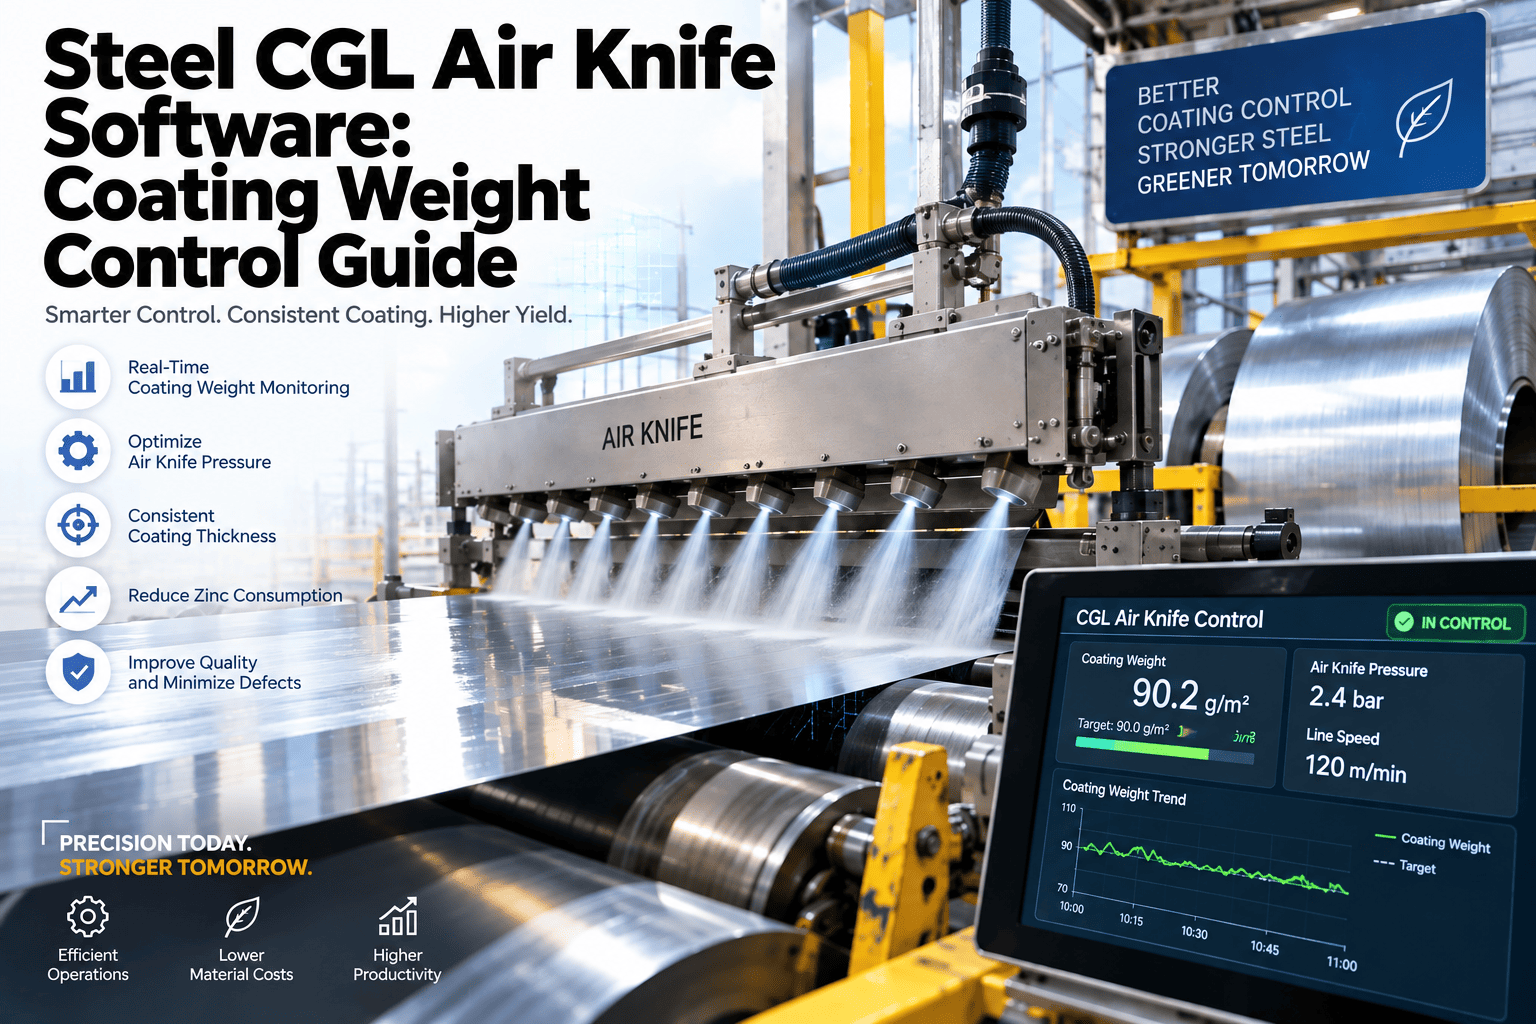
Automotive-grade galvanized sheet has almost no tolerance for coating weight error. Where a general industrial coating can run heavier without consequence, an automotive exposed panel spec often caps coating weight below 70 g/m² per side to keep spot-weldability and paint appearance within range, which means the pair of air knives sitting a few millimeters off the strip after the zinc bath are doing tolerance-critical work with almost no room for drift. A knife gap that has crept by a millimeter, or a pressure regulator that has drifted by a tenth of a bar, is enough to push an entire coil out of automotive spec while looking, on the line, exactly like every other coil that came before it.
Why Automotive Grades Leave No Margin
General galvanized product for construction or appliance use tolerates a coating weight range wide enough that normal air knife drift rarely causes a rejection. Automotive exposed panels are a different story: the coating has to be light enough for consistent spot-weld resistance and paint finish while still meeting corrosion protection minimums, which compresses the acceptable band on both ends. That narrow band means the four physical variables governing coating weight — knife gap, knife pressure, knife angle, and line speed — all have to hold within a tight window simultaneously, and a small drift in any one of them can be enough to move an automotive coil out of spec even while every other quality check on the line reads normal.
The Four Variables That Set Coating Weight
| Variable | Typical Range | Effect of Drift | Automotive-Spec Alert Trigger |
|---|---|---|---|
| Knife-to-strip gap | 8-15 mm | Increased gap raises coating weight non-linearly | ±1 mm positional drift |
| Knife pressure | 0.3-1.2 bar | Low pressure over-coats; over-pressure bares edges | ±0.05 bar from setpoint |
| Knife angle | 0-5° tilt | Asymmetric coating across strip width | Angle deviation greater than 0.5° |
| Line speed | 60-180 m/min | Speed increase thins coating at the same pressure setting | Coating weight gauge deviation beyond ±5 g/m² |
What Drives Each Variable Out of Spec
Why Coating Weight Drift Is Hard to Catch in Real Time
Most coating weight gauges sample after a measurement delay caused by the time-varying strip speed between the air knives and the gauge itself, which means the reading an operator sees can already lag the actual condition at the knife by a meaningful margin. On a fast-moving automotive line, that lag is enough for several meters of out-of-spec strip to pass before a correction takes effect. Catching drift before it reaches the gauge means monitoring the mechanical inputs — gap, pressure, and angle — directly, rather than waiting for the coating weight measurement to confirm a problem that started upstream. Start a free trial to build that mechanical monitoring layer on your own CGL, or book a demo to review your current gauge and alert configuration.
Reactive Knife Maintenance vs. Parameter-Tracked Control
Why Coating Weight Response Isn't Linear
The relationship between knife gap, knife pressure, and resulting coating weight is not a simple straight-line function — it follows a power relationship where line speed, gap, and pressure each carry different exponents in the prediction model most galvanizing lines use. That non-linearity matters operationally because a one-millimeter gap change near the tight end of the operating range can shift coating weight by a much larger margin than the same one-millimeter change near the wide end. Operators used to a linear mental model sometimes under-correct a small gap drift on the tight end of the range, assuming the effect will be proportionally small, when in practice that is exactly where the automotive coating weight ceiling is most likely to be crossed. Building alert thresholds around the actual measured response curve, rather than a flat percentage tolerance, catches this asymmetry that a simple linear rule would miss.
Cross-Width Coating Weight Variation
Average coating weight across a coil can sit comfortably inside the automotive ceiling while individual points across the strip width sit outside it, because knife angle, strip camber, and nozzle-to-strip distance all vary across the width even when the average reading looks clean. A coil that passes on an average reading but fails a spot check near one edge points to a cross-width problem that an average-only monitoring approach will never catch.
| Cross-Width Symptom | Likely Cause | Detection Method |
|---|---|---|
| One edge consistently heavier | Knife angle misalignment or uneven mounting | Multi-point gauge scan across strip width |
| Center of strip heavier than edges | Strip camber changing effective nozzle distance | Strip flatness monitoring paired with coating scan |
| Periodic streaking along strip length | Localized knife lip damage or nick | Visual inspection during scheduled knife lip PM |
| Gradual whole-width drift over a shift | Pressure regulator or gap position creep | Continuous parameter logging against setpoint |
Setting Tighter Tolerances Without Over-Alerting
Automotive-spec orders justify tighter alert thresholds than general product, but applying automotive-tight tolerances to every order on the line produces alert fatigue, where technicians start ignoring notifications because most of them fire on runs that never needed the tighter tolerance in the first place. The practical answer is order-aware tolerance switching: default thresholds for general product, and a tighter, automatically applied band whenever an automotive-spec order is active on the line. That switch has to be tied to the actual order running, not to a manual toggle a technician has to remember to set, because a missed manual switch on a high-volume line defeats the purpose of having tighter tolerances at all. Once the tolerance band is order-aware, alert volume on general product stays manageable while automotive runs get the scrutiny their spec actually requires.
How Oxmaint Supports Air Knife Coating Weight Control
Coordinating Air Knife Data With the Bath Chemistry Side
Coating weight is not purely a mechanical air knife question — bath temperature, aluminum content, and strip temperature entering the bath all interact with knife settings to determine the final result. A knife gap and pressure combination that produced spec-compliant coating weight yesterday can produce a different result today if bath aluminum content has drifted, even with every mechanical air knife parameter reading identical to the day before. Lines that track air knife parameters in isolation from bath chemistry data end up chasing coating weight problems that actually originate on the chemistry side, adjusting knife settings that were never the real cause. Reviewing both data sets on the same timeline, rather than in separate systems maintained by separate teams, shortens the path from a coating weight deviation to its actual root cause considerably.
Handling Coil Welds and Speed Transients
Every coil weld on a continuous galvanizing line forces a brief acceleration or deceleration as the line adjusts to the next coil's target speed, and unless knife pressure is compensated in step with that speed change, the section of strip passing the knives during the transient comes out at a different coating weight than the steady-state sections before and after it. On an automotive-spec run, that short transient section is exactly the kind of localized deviation that a whole-coil average reading can hide. Lines with automated speed-compensation logic built into the knife pressure control loop handle this automatically, but plants running older control systems without that logic often see a small, recurring coating weight anomaly at every weld that nobody has traced to its actual cause. Flagging weld locations against coating weight gauge data specifically, rather than reviewing the gauge trend as one continuous signal, makes this pattern visible where it would otherwise blend into normal readings.
Building Institutional Memory Around Knife Performance
Air knife pairs get swapped, reground, or replaced over a line's operating life, and without a persistent record tied to the physical knife rather than just the line position, hard-won knowledge about a particular knife's quirks disappears every time it is pulled for service. Logging performance history per knife identifier, not just per line, preserves that institutional memory across swaps and makes it easier to spot a knife that consistently underperforms regardless of which line position it is installed in.
Training New Operators on Knife Adjustment Judgment
Experienced operators often develop a feel for knife adjustment that new hires lack, especially for the subtle cross-width symptoms that a simple average reading won't show. Pairing that experience with a documented parameter history — showing exactly what gap, pressure, and angle change corrected a similar deviation in the past — shortens the learning curve considerably and reduces the odds that a new operator's correction accidentally overshoots into the opposite failure mode.