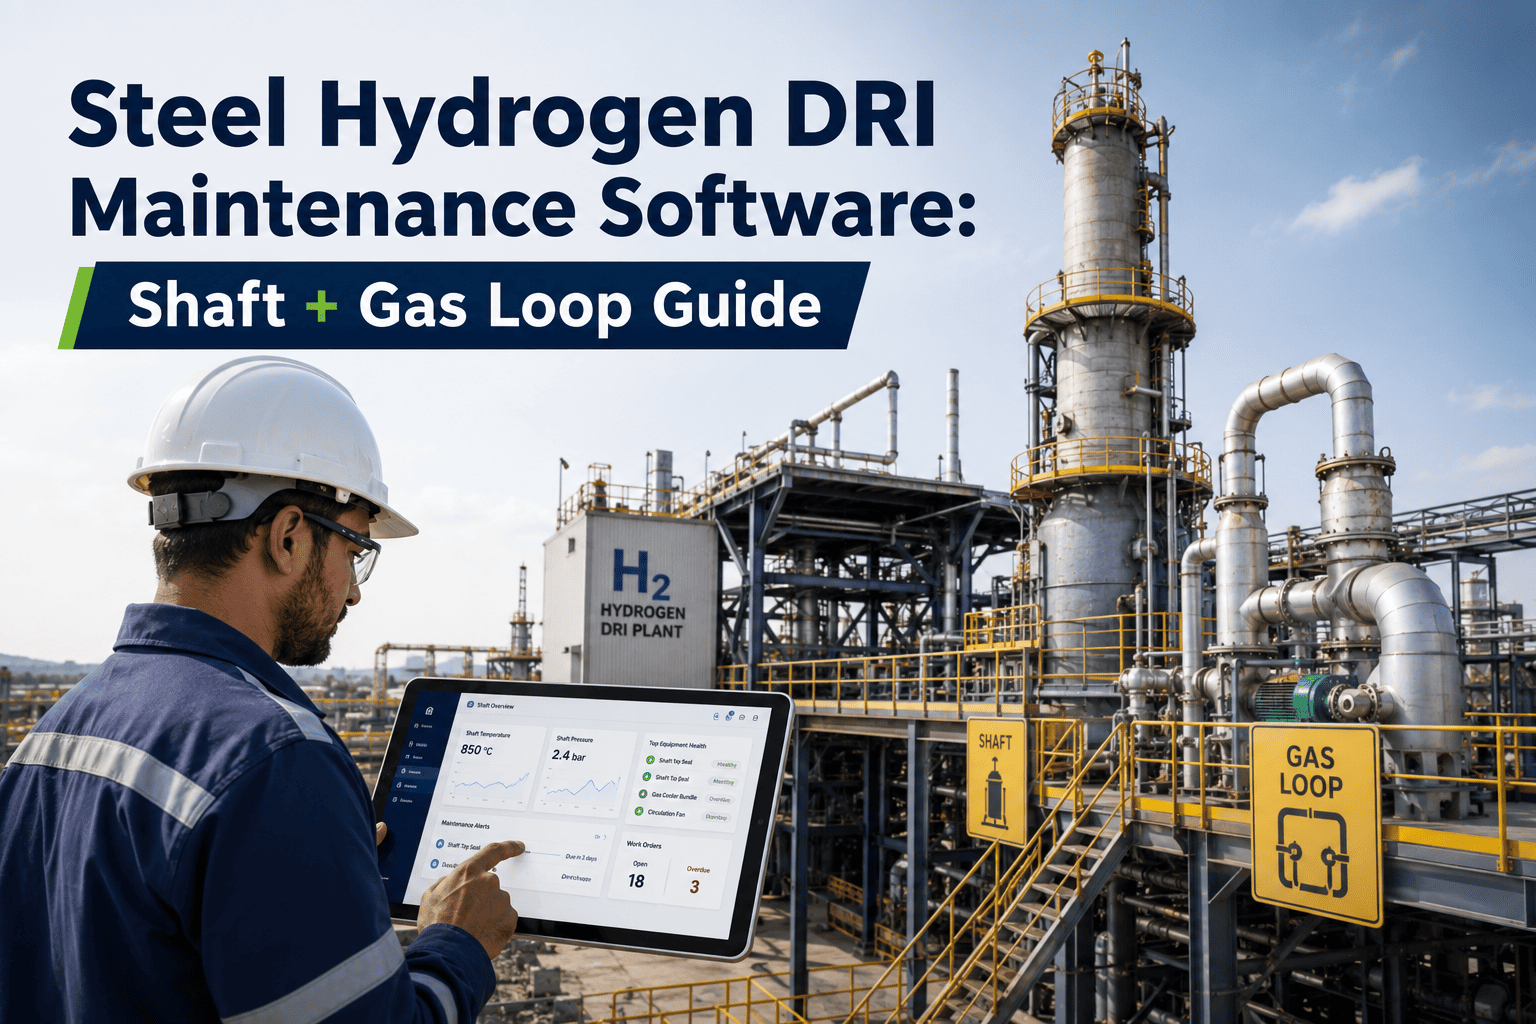
Hydrogen direct reduced iron production is moving from pilot projects to commercial-scale shaft furnaces across Europe, the Middle East, and North America, and the equipment inside that shaft behaves nothing like a natural gas DRI unit once hydrogen content climbs past 70 to 80 percent. Reduction chemistry that once produced iron and carbon dioxide now produces iron and large volumes of water vapor, which changes gas velocity, thermal profile, and condensation load through the entire recycle loop. Shaft refractory wears on a different curve, gas heaters run harder because hydrogen carries less energy per cubic meter than natural gas, and water knockout systems that were secondary equipment on a natural gas plant become mission-critical on a hydrogen plant. Maintenance teams that keep running natural gas DRI schedules on a hydrogen shaft are the ones who get surprised by fouled condensers and thermocouple drift within the first year of operation. This guide breaks down the shaft and gas loop maintenance discipline that hydrogen DRI actually demands, and where a connected maintenance platform such as Oxmaint keeps the inspection and compliance record straight.
Why Hydrogen Changes the Maintenance Equation
A natural gas DRI plant reduces iron ore with a hydrogen and carbon monoxide mixture generated by a reformer, and the byproduct stream is a blend of water vapor and carbon dioxide. A hydrogen shaft strips carbon out of the reducing gas almost entirely, which means every molecule of oxygen pulled off the iron ore leaves the furnace as water instead of being split between water and CO2. The result is a gas loop that has to move, cool, and condense far more water per tonne of metal than the natural gas process was ever designed for. Reformers and their catalyst beds disappear from the flow sheet in a pure hydrogen design, but that equipment is replaced by larger electric gas heaters, bigger condensers, and tighter control loops around dew point and recycle gas purity.
The Five Assets That Carry the Maintenance Load
The hydrogen gas loop is a closed circuit: gas leaves the top of the shaft carrying water and dust, gets cleaned and cooled, has water condensed out of it, gets reheated and boosted back to pressure, and re-enters the furnace through the bustle pipe. Every stage in that loop has a different failure signature, and lumping them into one generic preventive maintenance plan is how plants end up with unplanned gas loop outages.
Top Gas Scrubber
Removes dust and cools the off-gas before it reaches the condenser. Nozzle wear and scale buildup reduce cleaning efficiency and push particulate downstream into the heat exchanger.
Water Condenser
Strips water vapor from the recycle gas to protect reduction efficiency. Heat exchanger fouling at the temperature transition zone accelerates fastest here under high water loads.
Recycle Compressor
Restores gas pressure after cooling and condensation losses. Bearing temperature, vibration, and seal gas purity are the leading indicators of unplanned trips.
Gas Heater
Brings recycled and fresh hydrogen back up to bustle temperature. Duty cycles run harder than natural gas heaters because hydrogen has lower volumetric energy density.
Bustle Line and Distributor
Delivers heated gas into the shaft through the bustle pipe and center gas distributor. Uneven flow here shows up as hot spots and uneven metallization across the burden.
Shaft Refractory Shell
Absorbs the thermal cycling of the whole process. Shell thermocouple trending at fixed elevations is the primary tool for catching lining thinning before it becomes visible.
Put Shaft and Gas Loop PMs on One Schedule
Configure refractory checks, condenser fouling inspections, and gas heater PMs as one connected preventive maintenance program instead of six disconnected spreadsheets.
Shaft and Gas Loop PM Reference Table
These intervals are a starting reference point drawn from operating hydrogen and high-hydrogen-blend DRI plants. Every plant should tune frequency against its own OEM baseline, ore chemistry, and hydrogen purity, but the categories below rarely change.
| Component | Interval | Task | Signal to Watch |
|---|---|---|---|
| Shaft refractory shell | Continuous / annual outage | Thermocouple trend review, visual inspection at planned outage | Rising shell temperature at a fixed elevation |
| Water condenser bank | Monthly | Fouling check, differential pressure trend, tube cleaning | Rising delta-P across the exchanger |
| Gas heater elements | Quarterly | Element resistance test, insulation check, duty cycle review | Longer time to reach bustle setpoint |
| Recycle compressor | Weekly / continuous | Vibration monitoring, seal gas purity, bearing temperature | Vibration trend above baseline |
| Top gas scrubber | Monthly | Nozzle inspection, scale removal, spray coverage test | Reduced dust removal efficiency |
| Dew point sensors | Continuous with calibration quarterly | Calibration check against reference instrument | Drift versus manual sample results |
| Electrolyzer stack | Continuous with deep review quarterly | Stack voltage, membrane health, water purity check | Efficiency decline per stack module |
Why Water Is the Real Maintenance Driver
On a high-hydrogen shaft, water vapor production can reach roughly 540 kilograms per tonne of DRI produced, which is a dramatically higher load than the same furnace saw running on natural gas reducing gas. That water has to be pulled out of the recycle loop before the gas goes back into the furnace, or reduction efficiency drops and metallization suffers. The condenser and heat exchanger network is the equipment that carries this burden, and fouling at the temperature transition zone is the single most common cause of gas loop derates on hydrogen plants. Teams that track differential pressure trends across the condenser bank on a fixed schedule catch fouling weeks before it forces a rate cut, while teams that inspect on a calendar-only basis tend to find out about it during an unplanned shutdown.
Hydrogen-Specific Safety Requirements
Hydrogen introduces safety obligations that simply do not exist on a natural gas DRI plant, and they apply across the electrolyzer, the storage and distribution system, and the shaft itself. None of these are optional line items — they are the conditions under which insurers and regulators allow the plant to operate.
Hydrogen Embrittlement Inspection
High-pressure piping and vessels exposed to hydrogen require periodic embrittlement inspection, since hydrogen atoms can migrate into metal and reduce ductility over years of service.
ATEX and Area Classification
Zones around electrolyzers, storage, and the bustle line need documented hazardous area classification, with equipment rated for the zone it sits in and records kept current.
Continuous Leak Detection
Hydrogen burns with a nearly invisible flame and disperses fast, which makes fixed gas detection with logged calibration history a non-negotiable part of the safety case.
Hot DRI Handling
DRI charged hot at 600 to 700 degrees Celsius is pyrophoric on contact with air, so inert atmosphere control and transfer system integrity checks are safety-critical, not optional PMs.
Keep Every Hydrogen Safety Record Audit-Ready
Embrittlement inspections, gas detection calibration, and ATEX documentation stay linked to the asset and the technician who performed the work.
What a Hydrogen-Ready CMMS Actually Needs to Do
A maintenance platform built for coal-fired boilers or generic manufacturing plants was never designed for shaft thermocouple trending or condenser fouling curves. Hydrogen DRI plants need a system that understands the specific assets in this process and the specific failure signals that matter.
Shell Thermocouple Trending
Track shell temperature by elevation and zone, and get flagged automatically when a reading trends upward against its historical baseline.
Condenser Fouling Alerts
Log differential pressure readings across the water condenser bank and trigger a work order before fouling forces a production rate cut.
Electrolyzer Stack Health
Record stack voltage, membrane condition, and water purity per module so degrading stacks get flagged for maintenance before output drops.
Hydrogen-Specific PM Templates
Pre-built preventive maintenance schedules for gas heaters, compressors, dew point sensors, and embrittlement inspection intervals.
Safety Compliance Records
Keep ATEX documentation, gas detection calibration history, and technician certifications tied to the specific asset and inspection date.
Outage Planning Support
Plan refractory outages around measured lining thickness trends instead of a fixed calendar date, extending campaign life where the data supports it.
Frequently Asked Questions
How is hydrogen DRI shaft maintenance different from natural gas DRI?
How much water does a hydrogen shaft furnace actually produce?
What causes most unplanned gas loop outages on hydrogen DRI plants?
Do technicians need special certification to work on hydrogen DRI systems?
How does Oxmaint support hydrogen DRI shaft and gas loop maintenance?
Run Your Hydrogen DRI Shaft on Trend Data, Not Guesswork
Shell thermocouples, condenser fouling, electrolyzer health, and hydrogen safety compliance — tracked in one connected platform built for the process.