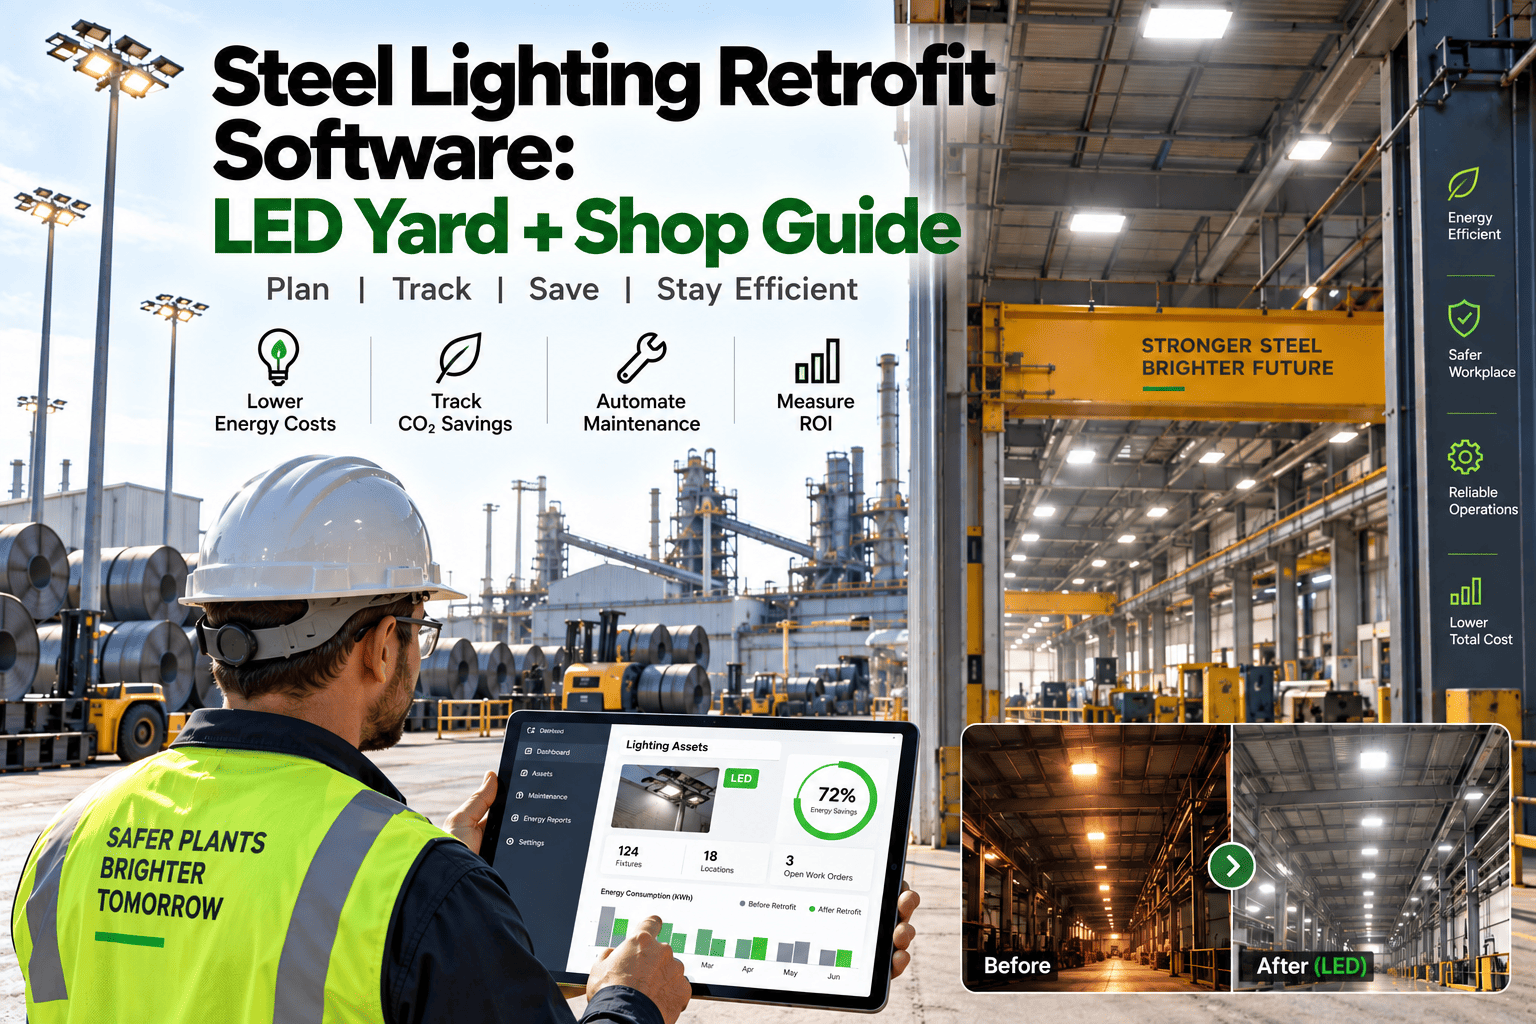
Steel plants are hard on lighting. Radiant heat gathers under melt-shop roofs, scale dust coats every lens, cranes shake fixtures loose, and the yards must stay bright all night. A steel lighting retrofit replaces metal halide, mercury vapour, and high-pressure sodium fixtures with LED, but the savings only last when the conversion is sequenced, recorded, and maintained. This guide explains how to plan it, and how Oxmaint maintenance management software keeps every fixture on record.
Steel Lighting Retrofit Software: LED Yard and Shop Conversion, Sequenced and Tracked
Why a Steel Plant LED Retrofit Is Not a Standard Fixture Swap
Office LED programmes are mostly about counting fixtures. A steel plant LED conversion is about surviving the environment. Fixtures hang where only a crane or lift can reach, so a failed unit in a hot bay may wait days for the next outage.
Before: legacy HID, unmanaged
- Mixed lamp types (metal halide, HPS, mercury vapour) with different spares
- Warm-up and restrike delay after every voltage dip
- Lamp and ballast changes that need cranes, lifts, or scaffolds
- Lighting on always-on circuits with little or no control
- No fixture-level history, so failures surface only when someone complains
After: LED, managed in a CMMS
- One or two standard fixture families per zone with matched spares
- Instant light after voltage dips
- Fewer height-access jobs, and the remaining ones are planned
- Zoning, dimming, or occupancy control where the process allows
- Every fixture tagged by location with install date, warranty, and work history
What the savings claim really depends on
LED retrofits are commonly reported to cut lighting energy by roughly half to two thirds against HID. The real figure depends on old system wattage, burn hours, and how much light each area actually needs. Meter a pilot before promising a number.
Zone-by-Zone Conditions and Specification Priorities
Each area of the plant stresses a fixture differently. Write a specification per zone rather than one plant-wide standard, and use the table below as a starting point for your own site survey.
| Zone | Dominant stress | Specification focus | Maintenance focus |
|---|---|---|---|
| Melt shop (EAF or BOF) | Radiant heat, dust, crane vibration, high mounting | Driver and LED temperature rating above the hottest measured ambient, vibration-rated mounts | Thermal checks, lens cleaning, early driver failure tracking |
| Ladle and caster area | Splash, steam, repeated heat cycles | Sealed housings with high ingress protection, strong surge protection | Seal inspection, moisture checks, failed unit log |
| Hot strip and bar mills | Scale dust, vibration, moving machinery | Flicker-free drivers, verified stroboscopic behaviour near rotating parts | Cleaning rounds, mounting checks, lux spot readings |
| Cold mill, pickling, coating lines | Chemical vapour, humidity, visual inspection tasks | Corrosion-resistant housings, colour rendering suited to surface inspection | Corrosion checks, lens condition, inspection-area light levels |
| Stockyards and scrap yards | Long night hours, weather, lightning, vehicle traffic | Mast or pole optics with glare control, surge protection, photocell or timer control | Photocell checks, pole and bracket inspection, outage response time |
| Control rooms and pulpits | Screen glare, operator fatigue | Low-glare optics, dimming, colour temperature suited to long shifts | Operator feedback, control settings review |
| Substations and MCC rooms | Safety, emergency egress | Emergency lighting integration, easy replacement | Emergency lighting tests, battery backup records |
The Seven-Step Retrofit Sequence
A retrofit that starts with purchasing usually ends with surprises. This sequence puts data first, proves the specification in a pilot, and turns every install into a documented job.
- Baseline the installed fixturesWalk each bay and record location, lamp type, wattage, mounting height, and working condition. Create one asset record per fixture or per circuit group.
- Measure burn hours and light levelsLog how many hours each zone is lit and take lux readings at working height. Some areas are over-lit and others under-lit, and both change the design.
- Rank areas by benefit, risk, and access costScore each zone on kWh saved, maintenance labour avoided, and difficulty of access. Let easy, high-burn areas prove the specification first.
- Pilot one bay per zone typeInstall a trial in a representative bay and watch it through a hot period and a full production cycle before approving volume orders.
- Write zone specificationsDefine temperature rating, ingress protection, surge protection, flicker performance, optics, and spare policy for each zone type. State what the supplier must document.
- Schedule installs into outage windowsAttach each install to a work order with crew, lift or crane booking, permits, and isolation steps, so nobody works over live equipment.
- Close out with as-built recordsUpdate asset records, attach commissioning lux readings, record warranty dates, and hand the zone over to the routine preventive maintenance plan.
Put Every Fixture on a Work Order Before the First Lift
Payback Arithmetic and Fixture Life
A defensible business case uses arithmetic that anyone can check. The example below is an illustration, not a measured result. Replace the inputs with your own metered data.
Illustration: one high-bay position, continuous operation
Rated life versus calendar life
LED life is rated in hours at a reference temperature, so hot bays can shorten it. Convert rated hours into years using real burn time for each zone.
| Rated life (hours) | Years at 8,760 h per year | Years at 4,000 h per year |
|---|---|---|
| 50,000 | About 5.7 | About 12.5 |
| 60,000 | About 6.8 | About 15 |
| 70,000 | About 8.0 | About 17.5 |
That arithmetic is where a 5 to 8 year planning range comes from in continuous-operation areas. Treat it as a budgeting figure, then let failure data from your own work orders correct it.
Building the Business Case Beyond Energy
Energy is the visible saving, but in a steel plant it is rarely the only one. A fair business case counts each cost bucket separately and names where the data will come from.
| Cost bucket | What to measure | Data source |
|---|---|---|
| Energy | kWh before and after per zone, at the real tariff | Sub-meters, utility bills, pilot readings |
| Lamp and ballast labour | Replacement jobs and hours per year, by zone | Historic work orders and stores issues |
| Access equipment and outage time | Crane hours, lift hire, and scaffolding used for lighting jobs | Maintenance and contractor records |
| Spares inventory | Number of lamp and ballast types held, and their stock value | Stores records |
| Light quality and safety | Lux compliance and lighting-related incident reports | Inspection readings, safety system |
| Incentives | Utility or government efficiency programmes, where they exist | Confirm locally before counting them |
Do not count a saving twice, and do not count an incentive until it is confirmed. Reviewers trust a smaller number that traces back to plant records.
Report it after the retrofit
Run the same calculation six and twelve months after each wave. When actual kWh, failure counts, and labour hours are compared with the plan, the next wave becomes easier to approve.
Maintenance After the Retrofit
LED reduces lamp changes, not maintenance. Dust, heat, and vibration still act on every fixture, so the routine shifts from replacing lamps to cleaning, inspecting, and trending failures.
Routine rounds
- Clean lenses where dust cuts light output; set the interval from inspection results
- Spot dark or flickering fixtures
- Log outages against the location tag
Periodic inspection
- Thermal scan of drivers and housings in hot bays
- Check mounting hardware, safety cables, and fixture tilt
- Verify photocells, timers, and sensors
- Compare lux spot checks with commissioning readings
After events
- Inspect after crane impacts, wash-downs, and lightning storms
- Check surge protectors after electrical faults
- Review warranty terms before repairing a failed unit
Controls, Sensors, and Dimming After the Conversion
LED fixtures switch on instantly and dim smoothly, which HID lamps cannot do. That opens control strategies that were impractical before, but every sensor, timer, and driver added to a circuit is another item to maintain.
| Area | Control strategy | Watch-out |
|---|---|---|
| Yards and outdoor areas | Photocell or astronomical timer, with reduced output after the last shift | Dirty photocells and timers that reset after a power loss leave lights burning by day or dark at night |
| Substations and MCC rooms | Occupancy sensing with a safe minimum level | Never leave an access route unlit, and keep emergency lighting independent |
| Storage and warehouse bays | Zoned switching and schedules | Fork truck and crane traffic still needs adequate light |
| Melt shop and mills | Usually constant output for safety; dim only where the process and risk assessment allow | Heat and dust shorten sensor life, so inspect controls with the fixtures |
| Pulpits and offices | Dimming and daylight response | Balance screen glare against operator comfort |
Controls need their own maintenance
Add sensors, photocells, and control gear to the asset register as separate items. Give them their own inspection tasks and test dates, so a failed sensor is not mistaken for a failed fixture.
The Fixture Register: What to Record and How Oxmaint Uses It
A retrofit without records repeats the old problem. Capture the same fields for every fixture or circuit group so reports can compare zones and suppliers fairly.
- Location tag
- Bay, column line, mounting height, circuit, and panel reference
- Fixture family
- Model, wattage, optic, driver type, and ingress rating
- Environment class
- Hot, dusty, corrosive, outdoor, or clean, so failures can be compared by condition
- Control method
- Always on, timer, photocell, sensor, or dimming schedule
- Lifecycle dates
- Install date, warranty end, and last cleaning or inspection
- Spares link
- Part numbers for matching drivers and fixtures held in stores
Where the maintenance software fits
- Asset management: fixture and circuit-group records with location, type, wattage, and install date.
- Work orders: retrofit jobs with crew, access equipment, permits, and checklists.
- Preventive maintenance: recurring cleaning, thermal, and lux-check tasks by zone.
- Mobile inspections: technicians log dark fixtures and findings from the bay.
- Inventory: spare drivers and fixtures by family with reorder points.
- Reporting and dashboards: failed-fixture trend by zone, PM completion, and retrofit progress.
Scoreboard: Six Measures That Prove the Retrofit
Track a small set of measures from day one. They show whether the savings are real and whether the new fixtures are staying reliable.
Common Retrofit Mistakes and Their Fixes
Most failed conversions share the same handful of causes. Check your plan against each pair before ordering fixtures.
Risks to Manage During Conversion
Confirm illuminance targets against the standards that apply in your region, such as IES recommended practice, EN 12464, or local factory regulations, and keep commissioning readings on file for audits.
- HighHeat derating. Drivers rated below the real ambient fail early. Measure the hottest bay temperature during summer operation before specifying.
- HighFlicker and stroboscopic effect. Poorly driven LEDs can make rotating parts look stationary. Test near rolls, shafts, and couplings before approval.
- HighWorking at height. Falls and dropped objects are the largest personal risk. Use permits, isolation, and planned access.
- MediumElectrical disturbance. Furnace and drive harmonics and switching transients stress drivers. Specify surge protection and review power quality.
- MediumGlare and comfort. Over-bright fixtures cause glare on screens and for crane operators. Specify optics and dimming.
- MediumMixed spares. Many fixture models multiply stock. Limit the number of models per zone.
Frequently Asked Questions
How much energy does a steel plant LED retrofit save?
Savings are commonly reported around 50 to 70 percent against HID, but the result depends on old wattage, burn hours, and target light levels. Meter a pilot bay first, then track results in Oxmaint.
Which area should be retrofitted first?
Many plants start with yards and outdoor areas because burn hours are high and access is easy. Shops follow in outage windows. Rank areas by savings, risk, and access cost.
Do LED fixtures survive melt shop heat?
Only if they are specified for it. Compare driver and LED temperature ratings with measured ambient temperature, and pilot before placing volume orders.
What should a fixture record contain?
Location, fixture family, environment class, control method, install and warranty dates, and linked spares. These fields let you compare failures by zone and supplier.
How can a CMMS support the conversion?
It holds fixture records, schedules retrofit work orders, and runs the cleaning and inspection routine afterwards. You can book a demo to see the workflow.