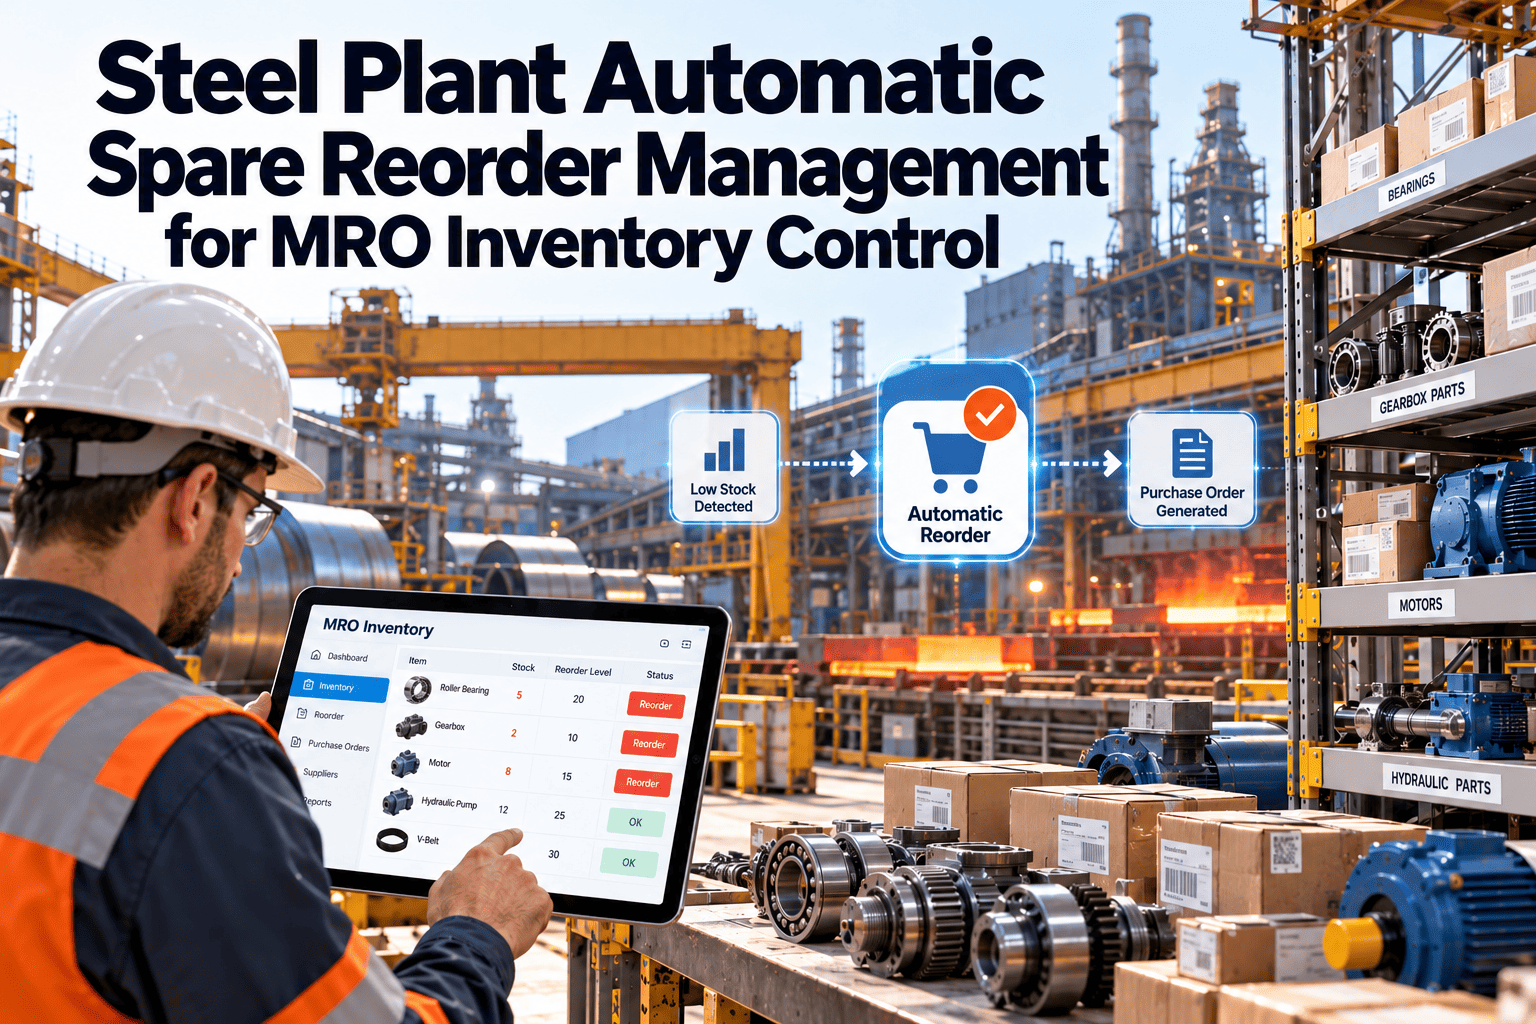
A steel plant can lose a full shift of production because a single bearing, a hydraulic valve or a set of slide gate plates was not on the shelf when the failure happened. At the same time, the same storeroom may hold years of slow-moving stock that nobody dares to write off. Automatic spare reorder management replaces memory and spreadsheets with rules tied to consumption, lead time and equipment criticality, and a connected maintenance management platform keeps those rules linked to real work orders and asset records.
Automatic spare reorder management that keeps critical steel plant parts on the shelf
Set reorder points by criticality, lead time and consumption, then let work orders, stock movements and approvals trigger replenishment before a stockout stops a melt shop, caster or rolling mill.
Steel plant MRO inventory fails in two directions at once
Most plants do not have a single inventory problem. They have a shortage problem on the parts that matter and an excess problem on the parts that do not.
When the part is missing
- A breakdown on a caster segment, mill stand or ladle crane waits for an emergency purchase or a cannibalised part.
- Expediting, air freight and premium supplier pricing replace planned procurement.
- Planned shutdown work slips because kits were never completed.
- Technicians lose trust in the store and begin hoarding parts in lockers and workshops.
- Production planning absorbs the delay as lost tonnage or missed delivery commitments.
When the shelf is overfull
- Capital is tied up in parts for equipment that has been upgraded, rebuilt or decommissioned.
- Duplicate part numbers hide true stock, because the same item is held under several descriptions.
- Rubber, seals, lubricants and electronic items age on the shelf and lose usable life.
- Storeroom space fills with obsolete items, making genuine stock harder to find.
- Annual stock counts reveal large variances that nobody can explain.
How an automatic reorder actually works
Automation is not a single switch. It is a chain of data points that must stay accurate for the reorder to be trusted.
Clean item master
One record per part, with manufacturer number, unit of measure, alternates and the equipment it serves.
Rules per item
Minimum, maximum, reorder point and order quantity based on criticality and lead time.
Live stock movement
Every issue to a work order and every receipt updates on-hand quantity immediately.
Trigger and review
When stock crosses the reorder point, a requisition or alert is raised for approval.
Receipt and feedback
Delivery times and actual usage feed back so the rules are adjusted instead of guessed.
Why issue discipline decides everything
- If technicians take parts without a work order reference, consumption history is wrong and every reorder point is wrong with it.
- If receipts are booked days late, the system reorders parts that are already sitting at the dock.
- If returned parts are not booked back, stock appears lower than it really is.
Classify spares before you automate them
A single reorder policy applied to every item is how plants end up with full shelves and empty critical bins. Combine value, criticality and usage to decide how each group is managed.
| Spare group | Typical items | Reorder approach | Review rhythm |
|---|---|---|---|
| Vital, long lead time | Gearbox assemblies, mould oscillation parts, large motors, specialised drives | Hold minimum insurance stock, reorder immediately after any use, track supplier lead time closely | Monthly, with maintenance and procurement together |
| Vital, short lead time | Proximity switches, relays, hydraulic fittings, standard bearings | Min and max with automatic requisition when stock hits the reorder point | Quarterly |
| Consumed with each campaign | Slide gate plates, nozzles, ladle shroud parts, rollers | Link demand to planned campaigns and heat counts rather than past averages | Per campaign plan |
| High usage, low value | Fasteners, filters, gaskets, lubricants, gloves | Simple min and max, supplier-managed or bin-based replenishment | Semiannual |
| Slow-moving or obsolete risk | Parts for retired lines, duplicate items, single-use project spares | No automatic reorder; review for disposal, return or consignment | Annual |
Building reorder points that reflect steel plant reality
The core logic is simple. The difficulty is feeding it honest numbers.
Demand during lead time
Average daily or weekly consumption multiplied by the supplier lead time, including transport, customs and inspection.
Safety stock
A buffer sized to the consequence of failure and the variability of both demand and delivery, not a fixed percentage.
Order quantity
Balances ordering effort, minimum supplier quantities, shelf life and storage space.
Inputs that change the calculation in a steel plant
- Planned versus random demand. Parts replaced on a schedule can be forecast from the maintenance plan, while breakdown spares need statistical history.
- Campaign-driven consumption. Refractory shapes, slide gate parts and rolls follow production campaigns, so heat counts and tonnage are better predictors than calendar time.
- Supplier lead time variability. Imported items and made-to-order components should use observed delivery times, not the quoted ones.
- Repairable versus consumable. Rebuildable items such as gearboxes and pumps need a repair loop, with stock counted as serviceable, in repair and scrap.
- Shared parts across units. A bearing used on several lines needs one combined reorder point, not separate ones per department.
Reorder logic by plant area
Different areas of an integrated or mini-mill steel plant consume spares in different patterns. Matching the trigger to the pattern keeps the rules meaningful.
Melt shop and ladle handling
Wear-driven items such as gate plates, nozzles and lining shapes should be reordered from heat counts and campaign plans, and critical crane and hydraulic spares need protected safety stock.
Continuous casting
Segment rolls, bearings, spray nozzles and mould parts combine scheduled replacement with failure risk, so both a maintenance-plan trigger and a minimum level are useful.
Rolling mills
Guides, bearings, couplings and gearbox components follow tonnage and roll changes, and long-lead drive parts belong in the vital group.
Utilities and water systems
Pumps, valves, seals and instrumentation are often shared across many users and suit min and max rules with repair-loop tracking.
Raw material handling
Conveyor belts, idlers, chutes liners and drive components wear in dusty, abrasive conditions and respond well to consumption-based triggers.
Three triggers that should work together
Reliable replenishment rarely depends on one signal. Strong programmes combine three.
Preventive maintenance demand
Upcoming preventive tasks list the parts they need, so the system can reserve stock and flag shortages weeks ahead.
Min and max levels
Actual issues against work orders pull stock down, and the reorder point raises a requisition automatically.
Inspection and monitoring findings
A vibration trend, oil analysis result or inspection defect can create a work order and a reservation before failure.
From manual ordering to controlled replenishment
The change is visible in how daily storeroom and planning work feels.
- Storekeeper memory decides when to reorder.
- Parts are requested only after a technician finds the bin empty.
- Safety stock is a guess carried over from years ago.
- Planners discover shortages on the day of the shutdown.
- Purchase history is scattered across emails and files.
- Reorder points are visible and reviewed by criticality.
- Requisitions appear before the bin reaches zero.
- Safety stock reflects lead time and failure impact.
- Planners see part availability against every scheduled job.
- Supplier performance and consumption history sit in one record.
Governance checklist for sustainable reorder control
Automation drifts without ownership. These checks keep the rules honest.
Item master hygiene
Merge duplicates, standardise descriptions and link every part to the equipment it supports.
Criticality review
Reassess classes after equipment upgrades, new lines or major failures.
Cycle counting
Count fast-moving and vital items frequently instead of waiting for annual stock takes.
Approval limits
Define who may approve automatic requisitions by value and by item class.
Supplier lead time audit
Compare quoted and actual delivery times and update reorder points accordingly.
Obsolescence review
Flag parts with no movement and decide on return, sale, disposal or retention.
Measures that show whether reordering is working
Track a small set of indicators and review them with maintenance, stores and procurement together.
| Indicator | What it tells you | Warning sign |
|---|---|---|
| Stockout rate on critical items | How often a vital part was needed and unavailable | Repeated stockouts on the same item point to a wrong reorder point or lead time |
| Service level of the store | Share of part requests filled from stock | Falling fill rate with rising inventory value suggests the wrong parts are stocked |
| Inventory turnover by class | How quickly stock is consumed | Very low turnover outside the vital group signals overstock |
| Emergency purchase share | Portion of purchases raised under urgency | High share means automatic triggers are not catching demand early enough |
| Inventory record accuracy | Match between system and physical counts | Variances show weak issue and receipt discipline |
| Kit completeness before shutdown | Parts ready ahead of planned jobs | Missing items close to start date indicate late planning |
How to read these measures together
- Falling stockouts with rising inventory value means safety stock is probably too generous on non-critical items.
- Rising emergency purchases with stable stock value points to weak planning visibility, not weak reorder points.
- Good record accuracy with poor kit completeness suggests parts exist but are not being reserved against scheduled jobs early enough.
- Review each indicator by plant area, because a healthy plant-wide average can hide a failing caster or mill store.
Reorder mistakes that quietly create stockouts
Most failed automation projects share the same handful of causes, and almost all are data or process problems rather than software problems.
Using averages for lumpy demand
A part that is used rarely but fails with serious consequences needs insurance stock, not an average that rounds demand down to zero.
Ignoring repair turnaround
Rebuildable assemblies are not consumed, they cycle through repair. Without tracking the repair loop, the plant either overbuys or discovers that no serviceable unit exists.
Setting levels once and never revisiting them
Equipment upgrades, new steel grades, changed lining practice and new suppliers all shift consumption and lead time. Reorder points need a review date.
Letting parts leave the store without a record
Informal withdrawals during breakdowns are understandable, but they must be booked afterwards or every later calculation is built on missing data.
Treating procurement and maintenance as separate systems
When buyers cannot see the maintenance plan and planners cannot see open purchase orders, both sides work with half the picture.
A phased path to automatic replenishment
Plants that try to automate the whole storeroom at once usually stall. A phased approach builds trust in the data before automation is switched on.
Clean and classify
Remove duplicates, link parts to assets and classify items by criticality, usage and lead time. Start with the equipment whose failure stops production first.
Enforce issue discipline
Require a work order reference for every issue and book returns and receipts the same day. Allow a few weeks of clean history to build up.
Set levels and alerts
Configure minimum and maximum levels for the vital and high-usage groups, with alerts first and automatic requisitions after the numbers prove reliable.
Review and refine
Hold a regular review of stockouts, emergency purchases and slow movers, and adjust rules using actual lead times and consumption.
Questions to ask before switching on automatic requisitions
- Is the part number unique, and are alternates and supersessions recorded?
- Does the supplier lead time in the system match the last several deliveries?
- Is consumption history based on work order issues rather than informal withdrawals?
- Who approves the requisition, and how quickly must they respond for a critical item?
- What happens when the supplier cannot deliver, and is an alternate source recorded?
Practical habits for storekeepers and planners
- Reserve parts against scheduled work orders as soon as the job plan is approved, so shortages appear weeks before the job.
- Keep a short list of critical items with their current stock, open orders and expected delivery dates in front of the weekly maintenance meeting.
- Record the reason for every manual stock adjustment, since unexplained adjustments are the quickest way to lose trust in the numbers.
- Review items that were reordered more than once in a short period, because repeated reorders often point to a wrong order quantity or an unrecorded failure.
- Tag shared spares clearly and record which department holds them, so borrowed parts are returned and counted.
Where Oxmaint fits in the spare reorder workflow
Spare control works best when inventory sits in the same system as assets, work orders and maintenance plans.
Spare reorder management: frequently asked questions
What is automatic spare reorder management?
It is a rule-based process where stock levels, lead times and criticality trigger purchase requisitions without manual checking. Teams review and approve rather than hunt for shortages.
Should every spare part have a reorder point?
No. Obsolete, project-specific and very slow-moving items are better managed by review and disposal rules than by automatic reorder.
How do we set safety stock for critical spares?
Base it on the production consequence of failure, supplier lead time variability and whether a repair or alternate part exists, not on a flat percentage.
Can reorder rules follow refractory and campaign demand?
Yes, wear-driven parts should be forecast from campaign plans and heat counts. You can schedule a demo to see how this fits your plant.
What is the first step to improve MRO control?
Clean the item master and enforce parts issue against work orders. You can sign up to start with your most critical assets.
Put critical spares under rules, not memory
Connect parts, assets and work orders so your steel plant reorders what matters before the shelf runs empty.