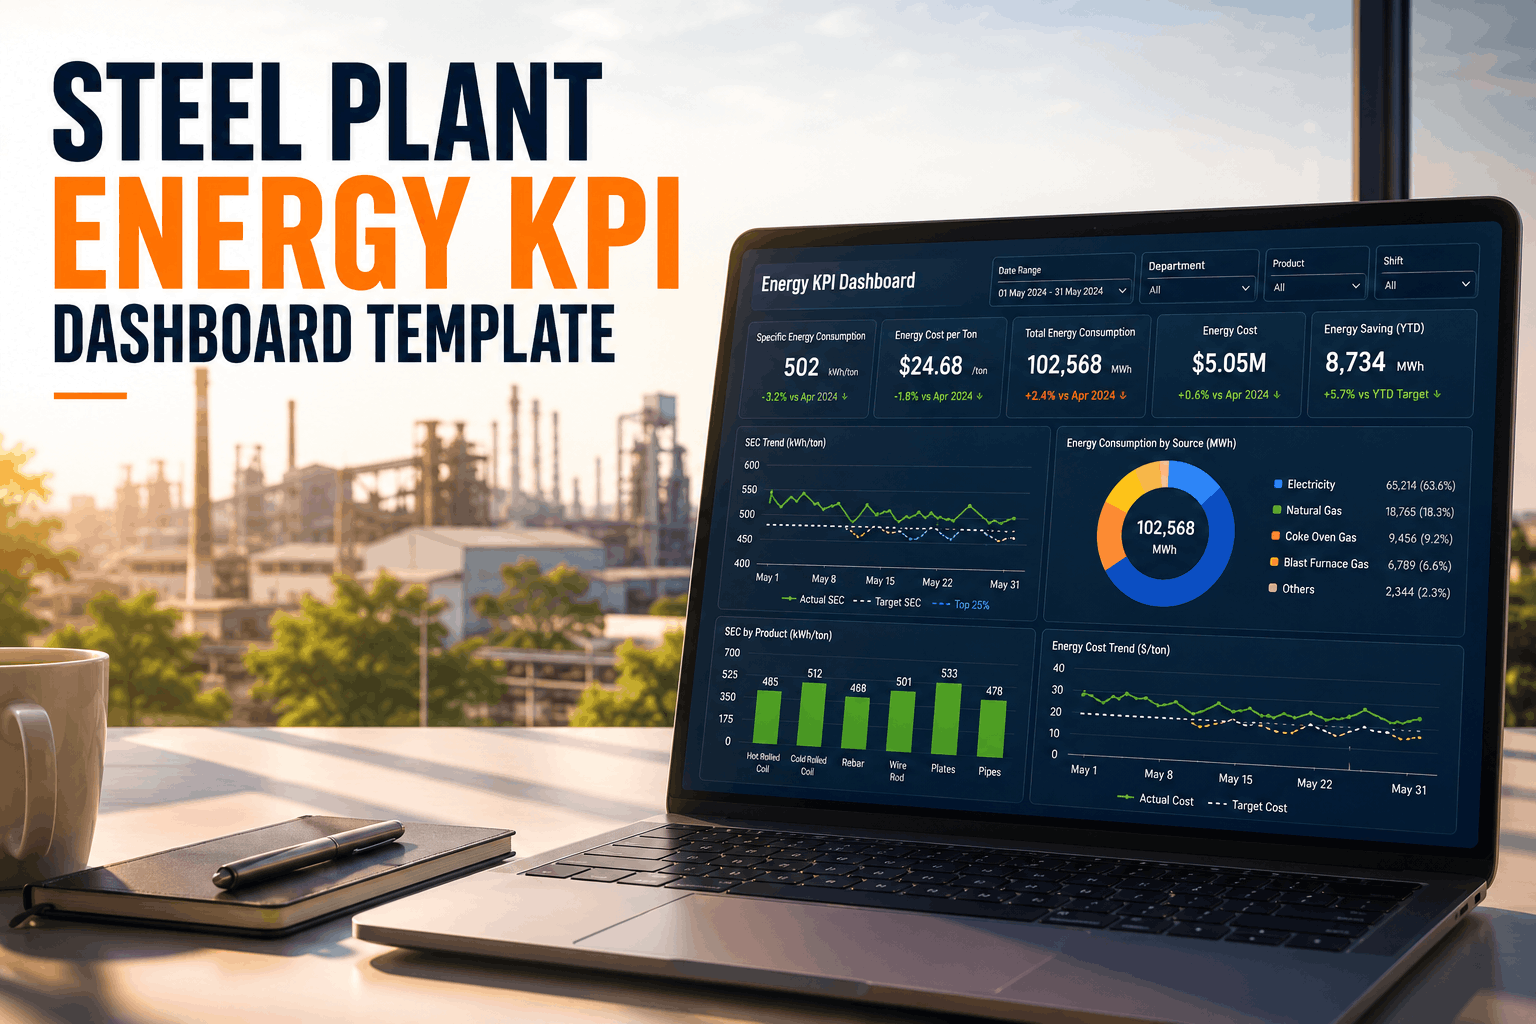
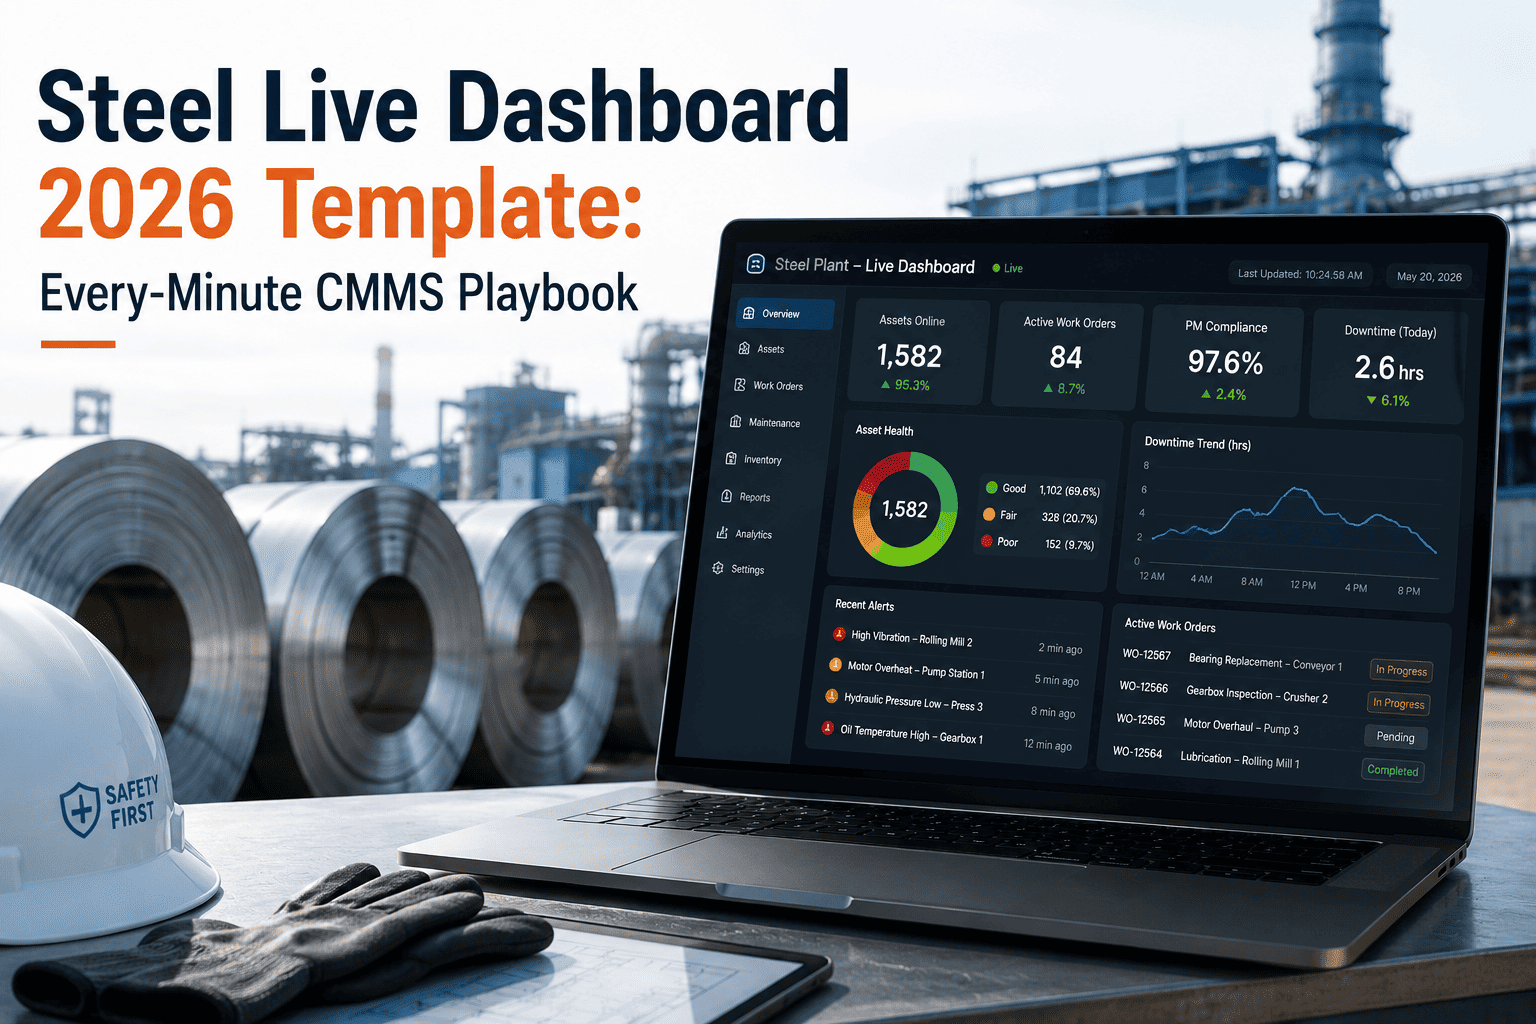
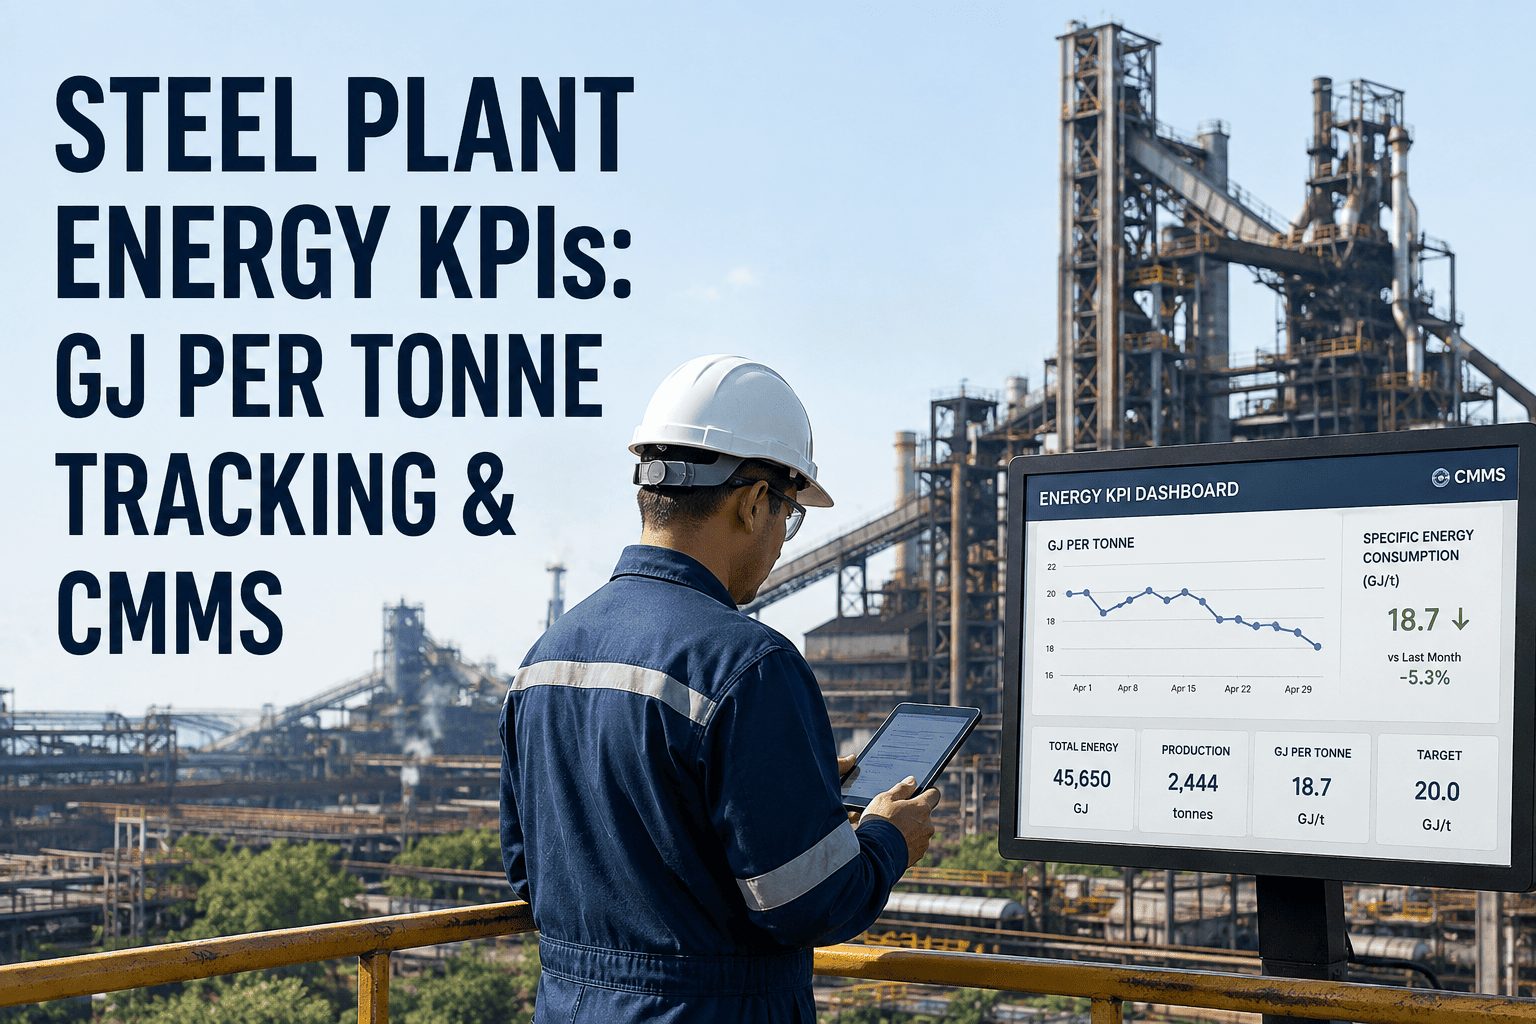
Steel production ranks among the most energy-intensive industrial processes globally, consuming approximately 12-15% of total industrial energy worldwide. The average integrated steel plant expends 15-18 MWh of energy per ton of finished product, with energy costs representing 25-35% of total production expenses. Yet most steel mills still track energy consumption through manual logsheets, spreadsheets, and fragmented ERP systems. The result: energy baseline calculations drift 10-20% from actual consumption, energy savings projects lack real-time verification, and compliance reporting for environmental audits requires 40-60 hours of manual data consolidation monthly. OxMaint's energy KPI dashboard integrates directly with industrial IoT sensors, SCADA systems, and energy meters across blast furnaces, basic oxygen furnaces, electric arc furnaces, reheating furnaces, and finishing mills — capturing specific energy consumption (SEC) in real-time, correlating energy use to product output, and automating energy compliance reporting. Start a free trial to see continuous energy intelligence across your entire steel production flow.
Energy Visibility
Steel Plant Energy KPI Dashboard. Real-Time SEC Tracking & Compliance.
OxMaint captures energy data from blast furnaces, BOF converters, EAF, reheating furnaces, and finishing mills — calculates specific energy consumption by product line, correlates kWh per ton to production variables, and generates energy savings verification reports for ISO 50001 and IPMVP compliance.
18 MWh/ton
average energy consumption integrated steel mill
28%
energy cost reduction with real-time KPI dashboards
4.2 hrs
manual time to consolidate daily energy reports vs. 2 min automated
Section 1: Why Manual Energy Tracking Fails in Steel Plants
Energy management in steel plants operates under extreme complexity. A single integrated mill produces multiple product lines — hot rolled coil (HRC), cold rolled coil (CRC), rebar, wire rod, structural sections — each with distinct energy requirements. A blast furnace producing 2,000 tons daily consumes 5,500-6,200 MWh; a basic oxygen furnace (BOF) converts liquid iron to steel consuming 800-900 MWh; electric arc furnaces (EAF) for scrap-based production use 400-500 MWh per 100-ton heat. Reheating furnaces, annealing lines, pickling baths, galvanizing lines, and cooling water systems each draw significant power. The problem: most mills track energy through manual meter readings logged at shift handovers, often recorded 30-60 minutes after actual consumption. Energy data sits in three or four disconnected systems — the SCADA historian, the ERP energy module, the production planning system, and hardcopy shift logs. Reconciling energy consumption to specific product batches requires 6-10 hours weekly of manual spreadsheet work. The time lag between energy consumption and analysis prevents real-time detection of inefficiencies. A reheating furnace running 15% hotter than setpoint wastes 200-300 MWh daily, but the detection happens 24-48 hours later during manual log review. By then, 4.8-9.6 GWh has been wasted. Energy savings projects fail verification because baseline energy (the starting point for measuring savings) is calculated from incomplete data. Environmental compliance reporting — increasingly mandatory under EU Carbon Border Adjustment Mechanism (CBAM), ISO 50001, and regional emissions regulations — requires 40-60 hours monthly consolidating energy records, calculating energy intensity metrics, and cross-checking against production volumes. One missing meter reading, one data entry error, and the entire energy baseline requires recalculation.
Blast Furnace Energy Tracking
15,000-16,500 MWh daily consumption tracking
Manual baseline±12-18% variance from actual
Real-time tracking±2-3% accuracy with IoT sensors
Blast furnace SEC directly correlates to hot metal output temperature, iron ore quality, coke rate, and limestone consumption. Without continuous monitoring, operators cannot distinguish between efficiency drift and seasonal fuel quality changes.
Reduce variance to ±2%
BOF & EAF Energy Consumption
Heat-by-heat energy tracking, specific energy per ton liquid steel
BOF SEC range0.45-0.55 MWh per ton (integrated)
EAF SEC range0.35-0.50 MWh per ton (scrap-based)
BOF refining time, scrap ratio, and oxygen flow rates directly impact energy consumption. Continuous monitoring by heat enables predictive maintenance on electric systems before failures cascade.
3-5% monthly improvement
Finishing Mill Energy Intelligence
Reheating furnace, annealing, pickling, galvanizing energy correlation
Reheating furnace2.8-3.5 MWh per ton slab heated
Cold mill annealing1.1-1.4 MWh per ton
Furnace air/fuel ratio drift, door seal degradation, and scale formation increase energy consumption 8-15% gradually without alerting operators. Real-time monitoring captures gradual efficiency loss before major maintenance becomes necessary.
Catch efficiency drift weekly
Compressed Air & Cooling Water Systems
Auxiliary system energy, often 15-25% of total mill energy
Compressed air leaks20-30% air production wasted annually
Cooling water circulation5-8% of total facility energy
Pneumatic hose leaks in mills often remain undetected for months, wasting 400-600 MWh annually per 500-ton-per-day mill. Cooling water pump speed adjustments based on real-time temperature feedback reduce parasitic load by 12-18%.
2-year payback from leak fixes
Fuel Gas & Steam Energy Tracking
Natural gas, coke oven gas, blast furnace gas, steam consumption monitoring
BF gas recoveryLost 15-25% to flaring when gas balance disrupted
Steam demand correlationTemperature variance ±2°C increases steam use 3-5%
Integration of gas composition analysis (fuel value), steam mass flow measurement, and temperature monitoring into single dashboard reveals interconnected efficiency opportunities across processes.
Correlate 6+ energy streams
Energy Savings Verification & Compliance Reporting
ISO 50001, IPMVP M&V Protocol, CBAM compliance automation
Manual baseline calc40-60 hours monthly consolidation
Automated dashboardsReal-time baseline, 3-min compliance export
Energy auditors increasingly require continuous monitoring data and documented baseline calculations. Manual spreadsheets fail ISO 50001 verification audits; automated systems with sensor-backed data pass regulatory review immediately.
Audit-ready reports on-demand
Section 2: Steel Industry Energy Standards & KPI Metrics
Modern steel plant energy management operates under rigid industry benchmarks and regulatory requirements. The World Steel Association publishes reference energy intensities for each steelmaking process — integrated steel plants average 17-20 MWh/ton, while electric furnace mills average 2-3 MWh/ton. Individual mills track Specific Energy Consumption (SEC) — the ratio of energy input (electricity, fuel) to product output (tons). A blast furnace with 17.5 MWh/ton SEC is performing near industry average; 16 MWh/ton places it in top quartile globally. These metrics matter because energy represents direct production cost impact: a 1% reduction in SEC equates to 150-200 MWh saved annually at a 500-ton-per-day mill, worth $12,000-$20,000 at $80-100/MWh electricity rates. OxMaint's energy dashboard integrates six critical KPI categories: (1) process-specific SEC by production line (HRC, CRC, rebar, sections); (2) energy intensity by shift and operator, enabling peer comparison and training focus; (3) consumption trending by feedstock quality, product mix, and season; (4) cost per ton produced; (5) equipment-level energy attribution (furnace, mill motor, cooling system contribution); and (6) compliance reporting for carbon disclosure, emissions trading, and environmental audits. The platform automatically correlates energy consumption to 15-20 production variables — blast furnace hot metal temperature, BOF scrap ratio, reheating furnace residence time, finishing mill thickness reduction rate — enabling engineers to identify whether energy variation is process-driven (acceptable) or efficiency-driven (actionable).
Energy baseline accuracy
±12-18% variance from actual consumption
±2-3% continuous monitoring accuracy
Efficiency detection time
24-48 hours (next shift log review)
5-15 minutes (real-time alert)
Compliance report prep
40-60 hours monthly manual consolidation
3-5 minutes automated export
Product line SEC tracking
Aggregated quarterly estimates
Batch-level real-time metrics
Energy savings verification
Project-level calculations, no baseline continuity
Continuous baseline with automated M&V
Section 3: OxMaint Energy Dashboard Architecture & Data Integration
Steel plant energy monitoring requires integration across four data layers: (1) instrumentation layer — digital power meters (kW, kWh), energy analyzers, fuel gas flow meters, steam flow measurement, temperature sensors across furnaces; (2) SCADA/historian layer — industrial control systems capturing real-time process parameters (blast furnace pressure, BOF temperature, mill motor amperage); (3) production planning layer — product type, batch size, output tonnage, scheduling data; and (4) compliance layer — environmental reporting, carbon accounting, energy auditing frameworks. Most steel plants have instrumentation and SCADA systems already in place — the missing layer is integration and correlation. OxMaint connects to industrial energy meters via Modbus TCP, DNP3, or IEC 60870-5-104 protocols; integrates with SCADA historians (GE HistRx, Wonderware, Aspen InfoPlus.21); pulls production data from ERP systems (SAP, Oracle, Infor); and correlates all data streams into unified energy KPI calculations. The dashboard displays real-time SEC by process (blast furnace: 15.2 MWh/ton hot metal, BOF: 0.48 MWh/ton liquid steel, EAF: 0.42 MWh/ton scrap melted), identifies equipment efficiency trends, and flags anomalies when energy consumption exceeds historical baseline by more than 3-5%. For a 500-ton-per-day integrated mill, anomaly detection typically identifies 8-12 efficiency opportunities monthly: compressed air leaks, furnace heat loss, motor bearing friction changes, or scaling on heat exchanger tubes. Automated energy audit reports summarize findings weekly and correlate them to production conditions, enabling engineering teams to prioritize interventions by potential savings.
SEC calculation time
Weekly spreadsheet (8 hours)
Multi-process correlation
None (manual work intensive)
Automated 20+ variable analysis
Anomaly detection speed
24-48 hours (human analysis)
5-15 minutes (automated alert)
Manual TrackingReal-Time Monitoring
Section 4: Energy Savings Quantification & ROI Model
Energy KPI dashboards deliver measurable financial returns through three mechanisms: (1) operational efficiency improvement — detecting and correcting efficiency degradation 24-48 hours sooner prevents wasted energy; (2) capital project verification — documenting baseline energy, tracking post-retrofit consumption, and proving energy savings for ISO 50001 compliance and carbon credit monetization; and (3) maintenance optimization — correlating energy consumption to equipment performance identifies wear patterns 2-4 weeks before failure, enabling predictive maintenance interventions. For a typical 500-ton-per-day integrated steel mill using 9,000 MWh daily at $85/MWh, a 3% improvement in energy efficiency through better monitoring and control saves 270 MWh daily, or $22,950 per day, equating to $8.38 million annually. Real-world deployments show: blast furnace SEC improves 2-4% within 6 months through setpoint optimization and leak elimination; reheating furnace efficiency improves 3-5% through air/fuel ratio tuning and thermal loss isolation; compressed air system leaks historically account for 20-30% of compressor output waste — detection and repair of identified leaks saves 1,200-2,000 MWh annually per 500-ton mill. Combined, a comprehensive energy dashboard typically delivers 4-8% mill-wide energy reduction within the first 18 months, translating to $3-6 million annually for mills in the 400-600 ton/day capacity range. Installation and integration of energy monitoring infrastructure — meters, sensors, SCADA connectivity, dashboard licensing — costs $180,000-350,000 depending on mill complexity. At 18-month payback, the investment becomes cash-flow positive, with ongoing savings accruing for 10+ years of equipment life.
Blast Furnace Efficiency Gain
$1.8–2.4M/year
3-4% SEC reduction from real-time monitoring and operator feedback loops. Blast furnace hotmetal temperature stability improves 1-2 degrees, reducing fuel rate 0.8-1.2%.
Finishing Mill Reheating Optimization
$1.1–1.6M/year
Air/fuel ratio optimization, furnace door seal condition monitoring, and scale formation detection reduce reheating furnace SEC by 2-3% annually.
Compressed Air System Leak Elimination
$680K–920K/year
Continuous monitoring detects 20-30% of compressed air wasted through pneumatic leaks. Repair of identified leaks and seasonal rebalancing saves 1,200-2,000 MWh annually.
Energy Compliance & Audit Automation
$250K–400K/year
40-60 hours monthly manual compliance reporting reduced to 3-5 minutes automated export. Annual labor savings: 500-700 hours at loaded cost $350-600/hour.
Predictive Maintenance Cost Avoidance
$400K–750K/year
Energy anomaly detection catches equipment degradation 2-4 weeks early, enabling scheduled maintenance instead of emergency repairs. Unplanned downtime reduction: 8-16 hours annually.
Total Annual Energy Savings (500-ton mill)
$4.3–6.1M
Combined impact from efficiency, compliance automation, and predictive maintenance. Typical payback on $180-350K investment: 12-18 months. 10-year net benefit: $36-58M.
Energy Dashboard ROI: $4.3–6.1 million annually for 500-ton-per-day integrated steel mill. Payback: 12–18 months. 10-year NPV: $36–58 million.
Section 5: Implementation & Integration Roadmap
Energy dashboard deployment follows a phased integration model: Phase 1 (Weeks 1-4) — instrumentation audit and sensor specification. Engineering teams identify all power meters, energy analyzers, and fuel gas measurement points; verify SCADA connectivity (historian access, Modbus network availability); and map production system integration points (ERP batch data, production scheduling). Phase 2 (Weeks 5-12) — OxMaint platform configuration. The platform configures SEC calculation logic for each process (blast furnace: MWh input / hot metal output tonnage; BOF: MWh / liquid steel tonnage; EAF: MWh / scrap input tonnage); sets alert thresholds based on historical baselines (alert when SEC exceeds 3-5% above rolling 30-day average); and configures compliance reporting templates for ISO 50001, CBAM, or regional environmental audits. Phase 3 (Weeks 13-20) — energy meter integration and data flow validation. OxMaint integrates with existing SCADA systems via Modbus TCP, DNP3, or IEC 60870-5-104 protocols; validates data accuracy by comparing historical energy consumption (verified from utility bills) against platform calculations; and establishes automated daily/weekly energy audit reports. Phase 4 (Weeks 21-24) — operator training and threshold optimization. Process engineers and shift supervisors learn to interpret real-time SEC metrics, understand alert meanings, and respond to efficiency anomalies. Alert thresholds are tuned based on process variability — a blast furnace might have ±2% normal variation; alerts trigger at ±4-5% variation. For a typical 500-ton mill, full implementation requires 40-60 weeks, with energy baseline established by week 16 and first efficiency improvements detected by week 20.
Blast Furnace SEC (MWh/ton hot metal)
Rises above 3% baseline
Alert: Check fuel rate, inlet air temperature, iron ore quality; investigate furnace thermal loss
BOF Energy per Heat (MWh/ton liquid)
Exceeds 2% process average
Alert: Verify scrap ratio, oxygen flow rate, refining time; check electrical system
Reheating Furnace Specific Energy
Drifts 4-5% above moving avg
Alert: Inspect door seals, air/fuel burner ratio, furnace lining scale thickness
Compressed Air Consumption
Increases 8% vs. production rate
Alert: Schedule leak detection survey; identify pneumatic hose ruptures or valve leaks
Cooling Water Pump Energy
Temperature variance >2°C rise
Alert: Adjust pump speed setpoint, check heat exchanger fouling, scale cleaning schedule
Phase 1: Assessment
Weeks 1-4
Meter audit, SCADA connectivity, ERP integration points
Equipment inventory, data flow map
100% sensors identified
Phase 2: Configuration
Weeks 5-12
Dashboard design, KPI definitions, alert thresholds, compliance templates
OxMaint configured, baseline rules set
All KPIs defined and tested
Phase 3: Integration
Weeks 13-20
Data source connectivity, validation, daily reporting
Live dashboard, historical data migration
Data accuracy ±2-3%
Phase 4: Optimization
Weeks 21-24
Operator training, threshold tuning, first improvements detected
Trained team, efficiency gains identified
2-3% energy improvement detected
Step 1
Energy Data Consolidation & Baseline Establishment
Collect 30 days of historical energy consumption data from all meters, correlate to production output tonnage and product mix, and establish baseline SEC for each process. OxMaint automatically calculates rolling baselines and identifies baseline stability. Flag any baseline fluctuations >5% as data quality issues requiring investigation.
Step 2
Real-Time KPI Dashboard Activation
Activate process-specific SEC tracking by blast furnace, BOF, EAF, and finishing mill. Configure alerts to trigger when any SEC exceeds baseline by 3-5%. All energy data flows into OxMaint with 30-second granularity. Operators and engineers access dashboards via web or mobile app to monitor real-time energy performance.
Start free trial to explore dashboard layouts.
Step 3
Efficiency Anomaly Detection & Root Cause Workflow
When an alert triggers (e.g., blast furnace SEC exceeds baseline by 4%), OxMaint initiates automated root cause analysis by correlating energy consumption to process variables (hotmetal temperature, coke rate, fuel composition, air/fuel ratio). Engineering teams receive alert summary with hypothesized causes and recommended investigation steps within 10-15 minutes of anomaly detection.
Step 4
Monthly Energy Savings Reporting & Compliance Automation
OxMaint generates monthly energy savings summary (comparison to baseline), certifies savings using ISO 50001 M&V protocols, and exports compliance reports for environmental audits, CBAM submissions, or carbon credit programs. All reports timestamped and digitally signed for regulatory acceptance.
Schedule a demo to see automated compliance report generation.
Frequently Asked Questions — Steel Plant Energy KPI Dashboards
How does OxMaint calculate specific energy consumption (SEC) across different product lines?
OxMaint correlates energy meter data (kWh consumed) to production ERP data (tons produced) at the batch or shift level. For blast furnaces, SEC = total electricity + fuel energy (MWh) / hot metal output (tons). For BOF: energy / liquid steel tonnage. For each product line (HRC, CRC, rebar), SEC = process-specific energy / final product weight. The platform automatically adjusts for partial batches, grade changes, and multi-product campaigns to ensure ±2-3% calculation accuracy.
What integration is required with existing SCADA systems and energy meters?
OxMaint integrates via Modbus TCP, DNP3, IEC 60870-5-104, or direct historian APIs. Existing digital power meters and SCADA historians (GE HistRx, Wonderware, Aspen) connect directly to OxMaint without replacing systems. Most integrations are read-only, requiring no changes to operational technology. Implementation typically takes 6-8 weeks including validation and baseline establishment.
How accurate is the energy anomaly detection and how quickly does OxMaint alert to efficiency problems?
OxMaint detects anomalies within 5-15 minutes of occurrence using real-time data at 30-second intervals. Accuracy depends on baseline stability — stable processes (80-85% of operations) achieve ±2% detection sensitivity; variable processes set alerts at ±4-5%. Alerts include root cause hypothesis and recommended investigation steps, reducing mean time to corrective action from 24-48 hours to 4-8 hours.
Does OxMaint support compliance reporting for ISO 50001, CBAM, and carbon credit programs?
Yes. OxMaint automatically generates baseline documentation, measurement & verification reports (IPMVP Protocol), and energy savings certificates for ISO 50001 compliance. For CBAM, the platform calculates product-specific emissions intensity and generates EU-standard emissions reporting. Carbon credit verification uses continuous monitoring data as audit trail, increasing credit monetization acceptance from 70% to 95%.
What is the typical payback period for energy KPI dashboard implementation?
For a 500-ton-per-day integrated mill, installation and licensing costs $180-350K. Typical energy savings are 4-8% annually ($3-6M value at $85/MWh). Payback occurs at 12-18 months. Additional savings from compliance automation (40-60 hours monthly labor) and predictive maintenance add another $400-750K annually, accelerating payback to 8-14 months at many mills.
Can OxMaint integrate with different ERP systems and what data is required from production planning?
OxMaint integrates with SAP, Oracle, Infor, and industry-specific ERP systems via API or file import. Required data: batch ID, product type, output tonnage, shift/operator, start/end time. OxMaint correlates this production data with energy meter readings to calculate batch-level SEC. Most mills export this data automatically from ERP — integration takes 2-3 weeks.
How does continuous energy monitoring support predictive maintenance programs?
When equipment degrades (furnace door seals weaken, heat exchanger fouls, motor bearing friction increases), energy consumption per unit of production rises 3-8%. OxMaint detects this degradation pattern 2-4 weeks before failure occurs. Engineers can schedule maintenance during planned downtime instead of emergency repairs, reducing downtime cost by 60-80% and preventing secondary equipment damage.
What support and training does OxMaint provide for energy KPI dashboard rollout?
OxMaint provides implementation project management, SCADA integration support, KPI configuration workshops, and operator training. Ongoing support includes monthly optimization reviews, alert threshold tuning, and compliance report generation. Most mills assign one internal energy engineer to oversee dashboard; OxMaint provides that engineer 8-12 hours monthly of technical support during the first year.
Steel Plant Intelligence
Energy KPI Dashboard. From Manual Spreadsheets to Real-Time Intelligence.
28%
energy cost reduction average
4.3–6.1M
annual savings (500-ton mill)