Maintenance plans in many steel plants grow by habit. A task is added after a breakdown, an interval is copied from a vendor manual, and nobody can say which failure each task is meant to prevent. Failure mode and effects analysis fixes that by tying every task to a specific way an asset can fail and a consequence that matters. This guide shows how to build an FMEA-based maintenance strategy for steel assets, and how a steel plant CMMS carries the results into daily work.
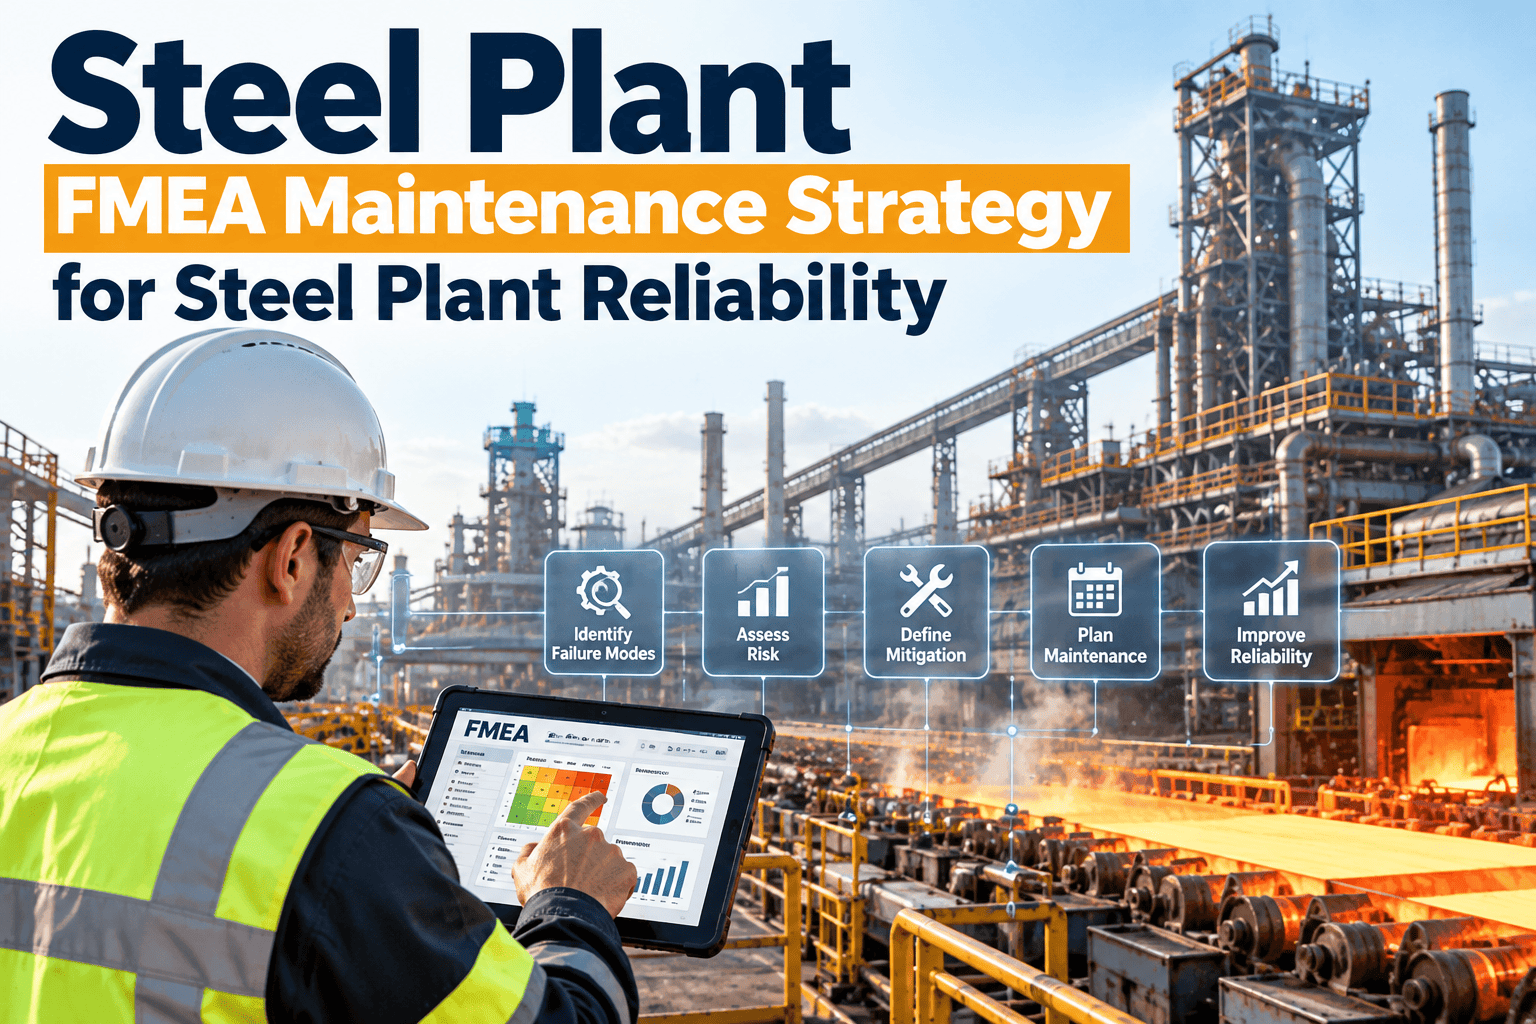
Steel Plant FMEA Maintenance Strategy for Steel Plant Reliability
FMEA links failure modes, effects and criticality to the inspections, preventive tasks and monitoring that actually protect production. Oxmaint puts the resulting plan to work.
Why Steel Plants Need Failure-Based Maintenance Planning
Steel production is continuous, hot and heavily interlocked. One failed hydraulic unit or cooling pump can stop a caster, and the real loss is the production and quality impact, not the part.
- Tasks copied from old plans
- Same interval for every similar asset
- Over-maintenance of low-risk items
- Gaps on hidden failure modes
- Little link to downtime cost
- Every task tied to a failure mode
- Intervals set by risk and failure pattern
- Effort focused on critical assets
- Hidden failures get tested
- Plan reviewed against real failure data
FMEA, RCM and Root Cause Analysis: How They Fit Together
These methods are often confused. They work best as a sequence, not as rivals.
| Method | Main question | When to use it | Output |
|---|---|---|---|
| FMEA | How can this asset fail, and what happens then? | Planning new or existing strategies | Ranked failure modes with effects and causes |
| RCM | What task, if any, is worth doing for each failure mode? | Selecting maintenance policy | Task type, interval and ownership decisions |
| RCA | Why did this specific failure happen? | After a significant failure | Verified causes and corrective actions |
| Criticality analysis | Which assets matter most? | Before FMEA, to choose scope | Ranked asset list |
Building the Steel Plant FMEA, Step by Step
Scoring Failure Modes
The traditional risk priority number multiplies severity, occurrence and detection. It is simple, but identical scores can hide very different risks.
A high-severity safety mode should get action even if its multiplied score looks modest. Many teams now rank by severity first or use action-priority tables instead of relying on a single number.
Illustrative Worksheet: Cooling Water Pump
The example below is illustrative only. Real scores must come from your asset, duty and failure history.
| Failure mode | Effect | Likely cause | Current control | Selected task |
|---|---|---|---|---|
| Bearing seizure | Pump trips, cooling flow drops, standby must start | Lubrication loss, misalignment, contamination | Operator rounds | Vibration and temperature trend, scheduled lubrication, alignment check |
| Seal leakage | Water loss, wet motor area, reduced pressure | Seal wear, shaft damage, dry running | Visual check | Seal inspection route, replace at condition limit |
| Impeller wear | Lower flow and head | Abrasion, cavitation | Occasional flow reading | Performance test, planned inspection at outage |
| Standby fails to start | No backup when duty pump trips | Hidden fault, control or breaker issue | None | Scheduled functional test and changeover |
Turn Your FMEA into Scheduled, Trackable Work
Oxmaint holds failure-based tasks, intervals and history against each asset, so the strategy reaches the shop floor.
Matching Failure Modes to the Right Task
Not every failure mode deserves a preventive task. The failure pattern and the warning time decide what works.
Steel Assets That Reward an FMEA
- Ladle and process cranes: Brakes, hoist ropes, limit switches and structural wear carry safety and production risk.
- Caster hydraulics and rolls: Seal failures, bearing wear and contamination affect quality and uptime.
- Rolling mill drives and gearboxes: Lubrication, alignment and load cycles drive wear.
- Fans and dedusting systems: Imbalance, buildup and bearing faults affect environmental compliance.
- Cooling water systems: Pump, valve and strainer failures can force process stops.
- Raw material conveyors: Pulleys, belts and idlers fail from abrasion and misalignment.
Keeping the FMEA Alive
A worksheet filed after a workshop goes stale. The strategy improves only when real failure data comes back into it.
Common Mistakes to Avoid
- Analyzing too many assets at once and finishing none.
- Running the workshop without operators and technicians who know the failures.
- Treating scores as precise and ignoring severity for safety issues.
- Writing generic tasks such as "inspect pump" with no failure mode or acceptance criteria.
- Skipping hidden failures on protective devices and standby equipment.
- Never reviewing the plan against actual work order history.
Measures of Strategy Effectiveness
How Oxmaint Supports an FMEA-Based Strategy
Oxmaint does not replace the engineering analysis. It makes the output executable and measurable.
- Asset hierarchy and criticality: Organize equipment and flag the assets the analysis ranks highest.
- Preventive maintenance: Schedule inspection, lubrication and replacement tasks with checklists.
- Condition-based workflows: Raise work from readings and inspection findings.
- Work orders and failure history: Capture cause and remedy to feed the next FMEA review.
- Inventory: Link critical spares to the failure modes that need them.
- Reporting: Track repeat failures, backlog and compliance.
Frequently Asked Questions
Put Your Reliability Strategy to Work on the Shop Floor
Connect criticality, failure modes, tasks and history in one maintenance system built for steel plant reliability teams.