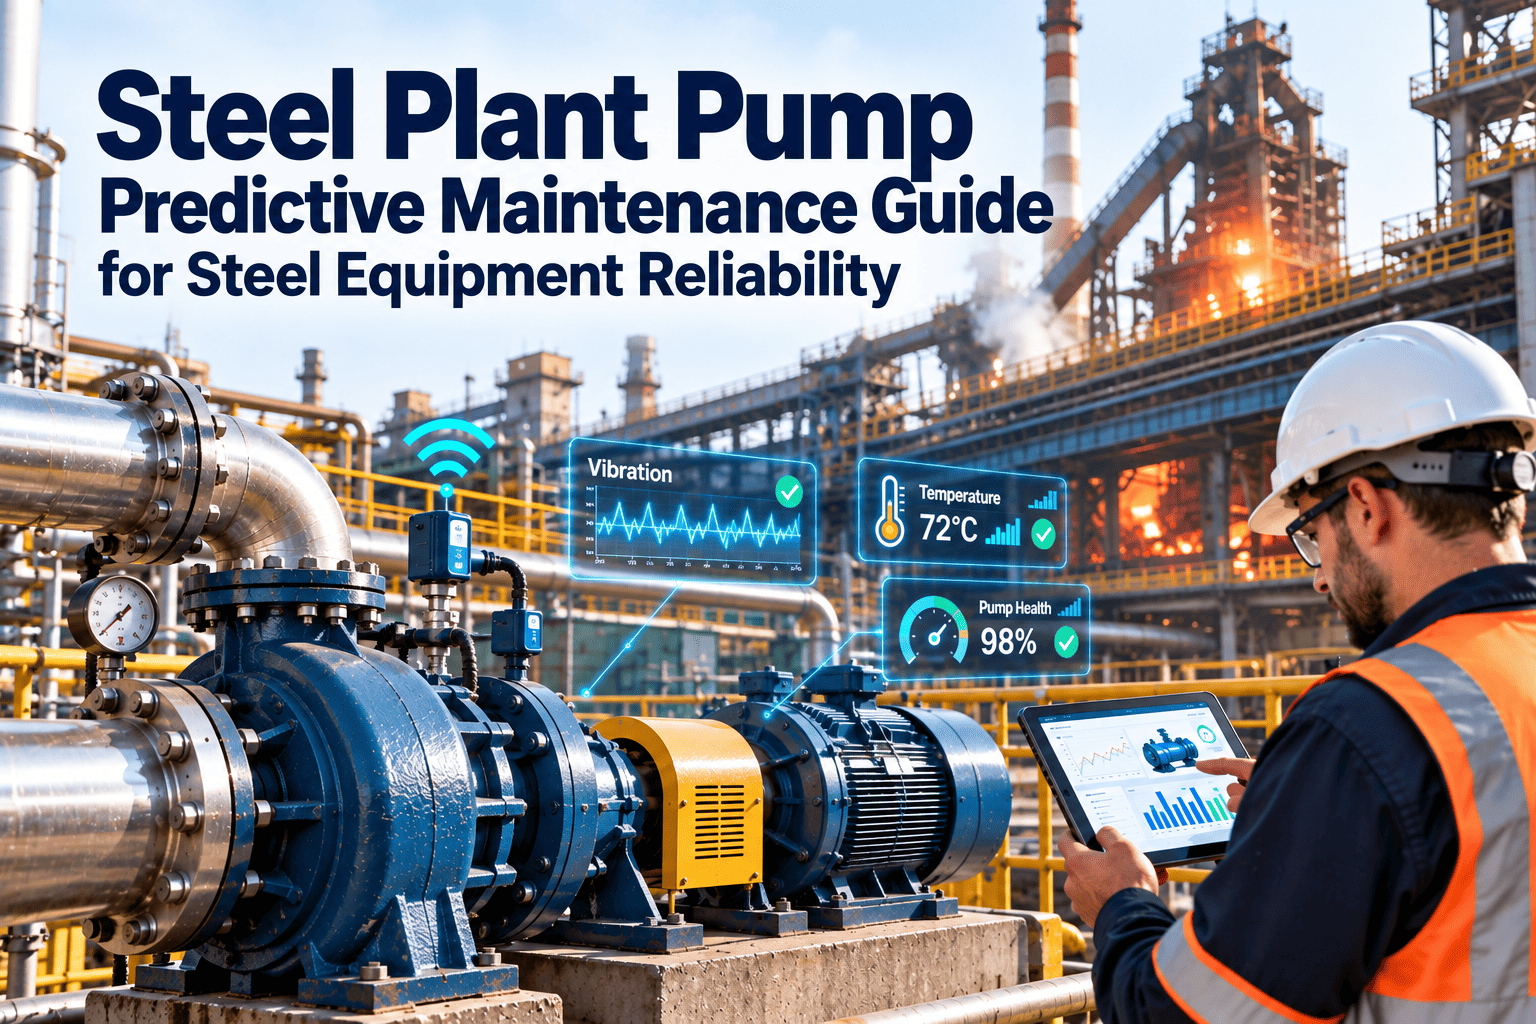
Pumps are the quiet workhorses of a steel plant. They push cooling water through furnace panels and casting equipment, feed descaling headers, circulate emulsions, move slurry from scrubbers and keep fire water ready. When one fails, the effect is rarely limited to the pump itself, because cooling loss or pressure loss can slow or stop the process it supports. Steel plant pump predictive maintenance uses vibration, temperature, current, pressure and flow data to catch bearing, seal, cavitation and motor problems while there is still time to plan the repair. The sections below show how to build that routine and track it in Oxmaint maintenance management software.
Steel Plant Pump Predictive Maintenance Guide for Steel Equipment Reliability
Predict pump bearing, seal, cavitation, vibration, motor and flow problems across cooling, water and process systems before they interrupt production.
- 1Healthy operation with a recorded baseline
- 2Early wear visible to ultrasound or oil analysis
- 3Vibration and current drift, the best planning window
- 4Noise, heat, seal weeping or flow loss
- 5Functional failure and unplanned stop
The pump systems a steel plant cannot afford to lose
Criticality varies by service. Rank pumps by what stops, not by how large the pump is.
Cooling water circuits
Supply cooling to furnace panels, casting equipment and rolling mill stands. Loss of flow can force a rapid shutdown.
High-pressure descaling
Feeds descaling headers on hot mills. Pressure drop can affect surface quality and mill rhythm.
Emulsion and lubrication
Circulates fluid for cold mills and bearing systems. Contamination and wear raise failure risk.
Scrubber and slurry
Handles abrasive solids that erode impellers and seals, with environmental performance at stake.
Boiler feed and process water
Supports steam and treated water supply to the wider plant.
Fire water
Standby pumps must start and perform on demand, so test records matter as much as condition data.
Common pump failures and how they announce themselves
Most pump failures leave a trail in measurable signals. The table pairs each mode with its cause and best early indicator.
| Failure mode | Typical cause | Early sign | Best detection |
|---|---|---|---|
| Bearing wear | Lubricant contamination, misalignment, overload | Rising high-frequency vibration, warmer housing | Vibration and temperature trend |
| Mechanical seal leakage | Dry running, abrasive solids, shaft movement | Weeping at the seal face, seal pot level change | Round checks and seal system readings |
| Cavitation | Low suction pressure, blocked strainer, high flow | Crackling noise, erratic pressure, vibration | Ultrasound, pressure and vibration |
| Impeller wear or erosion | Abrasive solids, scale, corrosion | Falling head and flow at the same power | Performance trend against the pump curve |
| Misalignment or looseness | Soft foot, pipe strain, worn coupling | Vibration at running speed and harmonics | Vibration spectrum |
| Dry running | Lost suction, closed valve, empty sump | Sudden heat, seal damage, low current | Motor current and suction pressure |
| Motor bearing or winding issues | Heat, contamination, electrical stress | Motor temperature rise, current imbalance | Temperature and current monitoring |
| Partial blockage | Scale, debris, clogged strainer | Higher differential pressure, lower flow | Pressure and flow readings |
Put every pump on a condition-based schedule
Record baselines, trend the readings and turn each alert into a work order with the right parts reserved.
Which measurements reveal which pump problems
No single signal covers every fault. A small set, chosen by pump criticality, gives better coverage than one expensive sensor.
| Signal | Faults it can reveal | Practical note |
|---|---|---|
| Vibration (velocity and high-frequency) | Bearing wear, misalignment, imbalance, looseness, cavitation | Compare against vibration severity guidance such as the ISO 20816 series and your own baseline |
| Bearing and housing temperature | Lubrication problems, overload, bearing damage | Read with ambient temperature and load |
| Motor current | Dry running, blockage, wear, electrical imbalance | Useful where vibration sensors are hard to fit |
| Suction and discharge pressure | Cavitation risk, blockage, wear, valve problems | Differential pressure shows performance loss |
| Flow | Operating point drift, internal wear | Plot against the pump curve |
| Oil analysis | Contamination, wear particles, oil degradation | Best for larger oil-lubricated machines |
| Ultrasound | Cavitation, lubrication need, early bearing defects | Handheld tools suit regular routes |
A pump far from its best efficiency point wears faster
Pumps are designed to run near their best efficiency point. Drifting far from it changes loads on bearings, seals and the impeller.
Low flow side
Recirculation, heat build-up, shaft deflection and seal stress become more likely.
Near best efficiency
Lowest hydraulic loading and generally the longest component life.
High flow side
Higher suction demand raises cavitation risk and can overload the motor.
When cooling demand changes with production, check whether pumps are throttled or running more units than needed. Fixing the operating point often extends seal and bearing life.
From a drifting reading to a planned repair
- Confirm the reading.Repeat the measurement and compare it with the baseline and with the same pump last week.
- Check operating conditions.Look at flow, suction pressure and strainer status before blaming the pump.
- Classify the likely cause.Use the failure mode table to choose between bearing, seal, hydraulic or electrical causes.
- Rank by consequence.A drifting standby pump and a drifting duty pump on a cooling loop do not get the same urgency.
- Create the work order.Attach readings, reserve the seal kit or bearings and book a window with operations.
- Verify after repair.Take new readings and update the baseline.
Not every pump deserves the same programme
| Pump tier | Example duty | Suggested strategy |
|---|---|---|
| Tier 1: process critical, no spare | Primary cooling or descaling pump | Continuous or frequent condition monitoring plus planned overhauls |
| Tier 2: critical with installed spare | Duty and standby cooling pair | Route-based readings, rotation of duty and standby, preventive tasks |
| Tier 3: important but buffered | Transfer pumps with a tank buffer | Periodic checks and inspection-driven repairs |
| Tier 4: low consequence | Sump or drain pumps | Basic preventive tasks or run to failure with spares on hand |
Standby pumps need attention too. A spare that has not been run or tested may fail the moment it is needed.
A pump round checklist that supports prediction
Operator rounds provide the human signal that sensors may miss. Keep the list short and consistent.
- Listen for changes in sound, such as crackling, grinding or knocking.
- Check the seal area for weeping or leakage and record the finding.
- Read suction and discharge pressure gauges and note any drift.
- Check the bearing housings and motor for unusual heat using the approved tool.
- Check oil level and condition, and grease points where fitted.
- Inspect strainers, couplings guards and base bolts.
- Note any leaks, corrosion or pipe strain.
How a CMMS holds the programme together
Oxmaint maintenance management software links the pump, its readings and its repair history.
KPIs that show whether pump reliability is improving
Mistakes that undermine pump predictive maintenance
- Collecting readings without baselines, so nothing can be compared.
- Monitoring only the duty pump and neglecting standby units.
- Replacing seals repeatedly without checking operating point, flushing or alignment.
- Ignoring strainers, suction conditions and valve positions.
- Leaving alerts in a spreadsheet instead of turning them into work orders.
- Skipping verification readings after the repair.
A phased start across the utilities area
Register and rank
List pumps by system, record nameplate data and assign criticality tiers.
Baseline
Capture healthy readings for Tier 1 and Tier 2 pumps.
Routes and work orders
Launch mobile rounds and connect alerts to corrective work.
Review and extend
Study repeat failures and widen coverage to lower tiers.
Steel plant pump maintenance questions
What is pump predictive maintenance?
It uses condition data such as vibration, temperature and flow to plan repairs before a pump fails.
Which pumps should be monitored first?
Start with pumps whose failure stops production or has no installed spare, such as cooling and descaling duties.
How can I detect cavitation early?
Watch suction pressure, strainer condition, noise and high-frequency vibration together. Ultrasound can help confirm it.
Can a CMMS trigger pump work orders?
Yes, readings and inspections can raise work orders. Start free to try it on one system.
What data do we need to begin?
A pump list, criticality tiers and recent failure history are enough. Book a demo to map your setup.
Keep cooling, descaling and process water running
Combine pump condition data, operator rounds, spare parts and repair history so every alert becomes planned work.