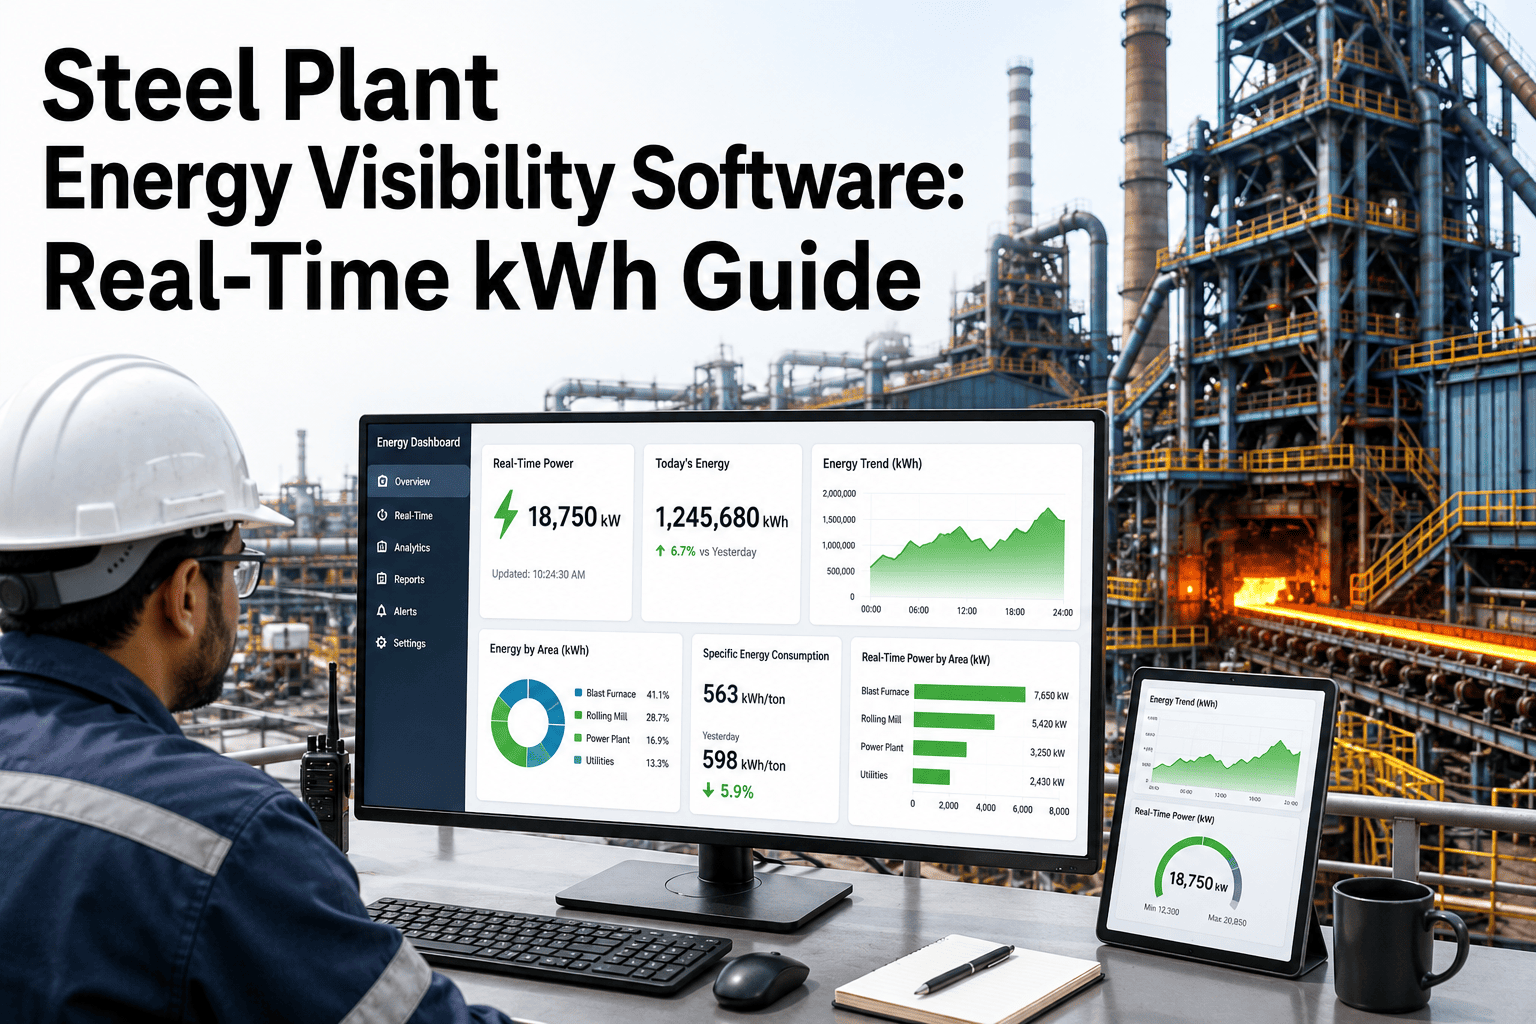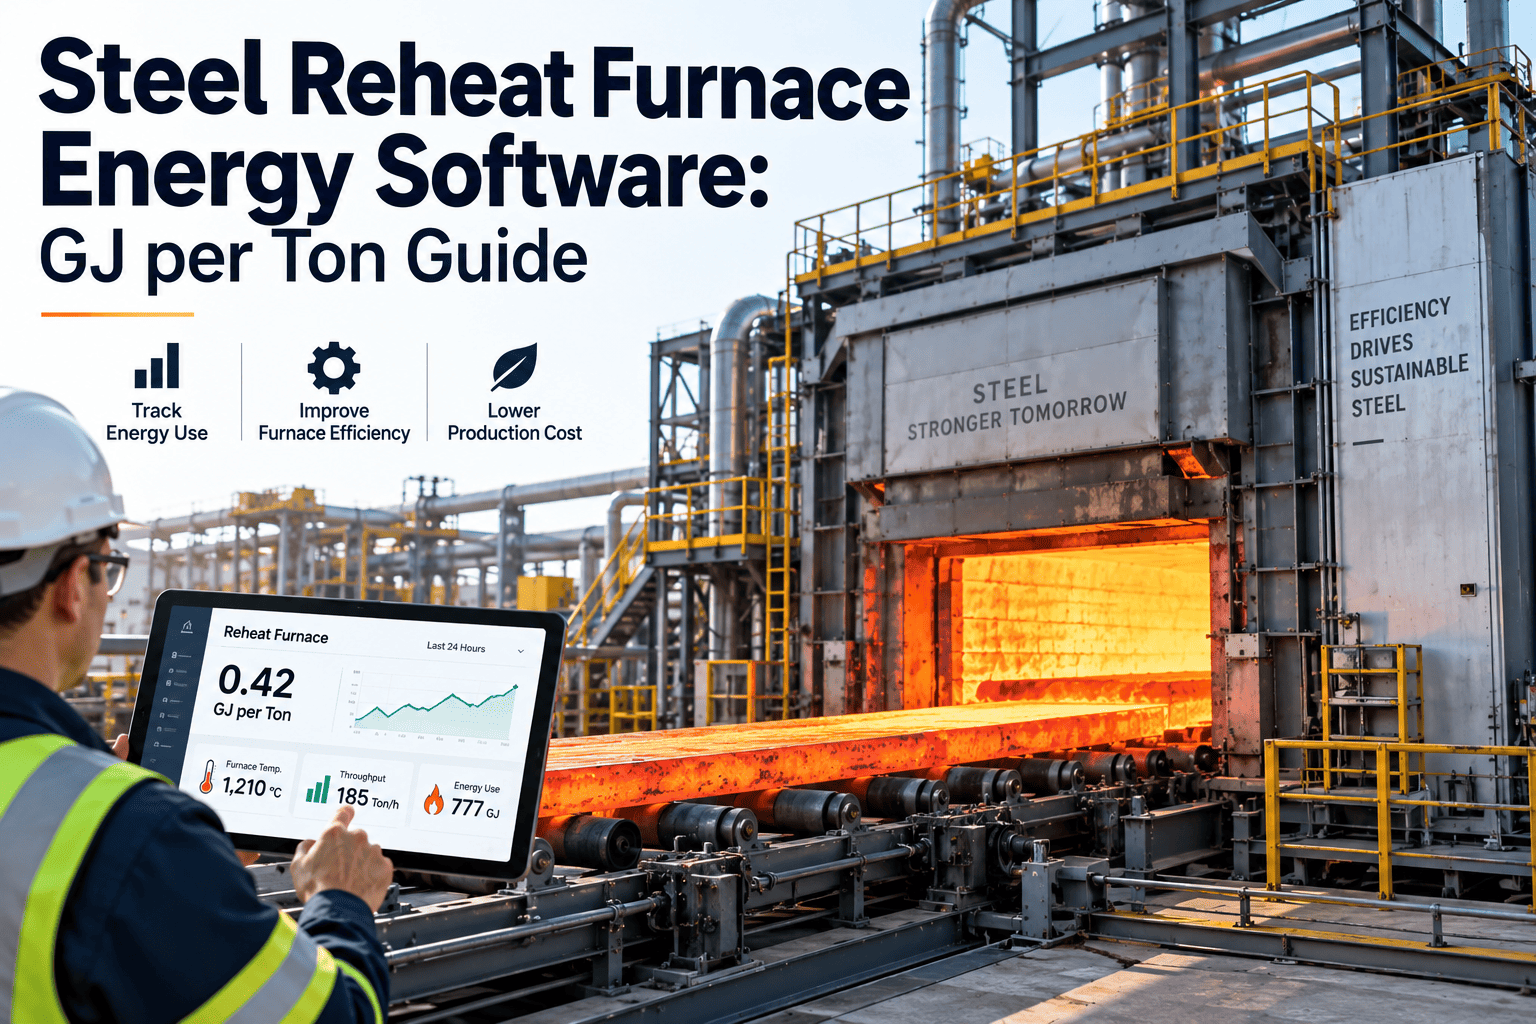
Steel reheat furnaces decide the economics of a rolling mill long before a single billet reaches the stand, and the gap between a well-run furnace and a drifting one shows up as GJ per ton — the number every plant manager gets asked to defend in the monthly review. A furnace running just 15% above its target specific fuel consumption can add several hundred thousand dollars a year in gas cost on a mid-size mill, and the cause is almost always traceable to burner drift, a leaking skid pipe, or a refractory gap that maintenance caught weeks too late. Combustion efficiency, skid cooling loss, and wall heat loss do not act alone — they compound against each other the longer a furnace runs without structured inspection, and most teams still calculate GJ per ton from a spreadsheet built long after the fuel has already been burned. Oxmaint's maintenance management software for steel plants connects reheat furnace inspection and repair activity directly to energy outcome, so GJ per ton stops being a monthly surprise and becomes a number the maintenance team actively manages against a target.
See Your Furnace's GJ Per Ton in Real Time, Not Next Month
Oxmaint links burner, skid, and refractory maintenance records to live fuel consumption per ton — so deviations from your energy baseline become a work order, not a line item in next quarter's report.
What GJ Per Ton Actually Measures — And Why It Moves
GJ per ton is the total fuel energy consumed by the reheat furnace divided by the tonnage of steel actually reheated in that period. It sounds like a simple ratio, but it is sensitive to almost everything happening inside the furnace shell: burner tuning and air-fuel ratio, skid pipe insulation condition, door and seal integrity, refractory thickness, charge temperature, and how consistently the furnace runs at rated throughput rather than starting and stopping. Two furnaces of identical design and age can post very different GJ per ton numbers purely because one has a maintenance programme that catches drift early and the other does not. The tiers below reflect where reheat furnace fuel rate typically lands depending on furnace condition and operating discipline, using specific fuel consumption as the primary comparison metric across plants of different sizes.
Where the Energy Actually Goes Inside a Reheat Furnace
Roughly a third of the fuel energy fed into a typical reheat furnace never ends up heating the steel at all — it leaves through the stack, the skid system, the walls, or an open door. None of these losses are visible from the control room without dedicated monitoring, which is exactly why they persist for months once they start. Flue gas carries away the largest single share because exhaust temperatures at the charge end routinely sit well above ambient. Water-cooled skid pipes that support the billets or slabs are the second-largest loss path, and the loss grows sharply once insulation around the skid rails degrades or fails, since the cooling water is now absorbing heat that should have gone into the steel. Wall and roof losses climb as refractory thins and cracks with age, while door and opening losses spike whenever seals are damaged or charge/discharge openings run larger than the process requires. Scale formation adds a further, easily overlooked loss — every percentage point of oxidation scale represents steel and heat that never reaches the rolling mill.
Reheat Furnace Benchmarks by Operating Condition
Fuel consumption for the same furnace can swing by 30% or more purely based on whether steel enters hot from continuous casting or cold after full cooldown, and by how consistently the furnace runs at design throughput rather than idling and restarting. The table below lines up the ranges plant teams typically use to sanity-check their own numbers against comparable reheat furnace operations.
| Operating Condition | Typical Fuel Rate | Primary Driver | Maintenance Lever |
|---|---|---|---|
| Hot charge (slab/billet direct from caster) | 0.9 – 1.0 GJ/t | Retained casting heat reduces reheat duty | Charge conveyor uptime, transfer speed |
| Cold charge, well-maintained furnace | 1.0 – 1.3 GJ/t | Burner tuning, skid insulation intact | Burner PM, O2 trim calibration |
| Cold charge, monthly plant average | 1.3 – 1.6 GJ/t | Mixed hot/cold charge ratio | Hot charge ratio tracking |
| Degraded furnace, deferred maintenance | 1.6 – 1.8+ GJ/t | Skid leaks, seal gaps, refractory loss | Skid inspection, door seal replacement |
| Furnace after 12-month energy-linked PM programme | ~1.1 GJ/t (from 1.42 GJ/t baseline) | Sustained burner and skid maintenance | Continuous OBD-style condition monitoring |
Turn Your Reheat Furnace's Energy Gap Into a Work Order
Oxmaint's steel plant maintenance software ties burner inspection, skid pipe condition, and refractory checks to a live GJ-per-ton dashboard, so the gap between your baseline and your actual fuel rate is visible before it costs you a quarter of overspend.
Common Reasons Reheat Furnaces Miss Their Energy Target
Burner Drift and O2 Trim Neglect
Burners that run rich or lean of their optimal air-fuel ratio waste fuel every single hour the furnace operates, yet the drift is gradual enough that operators rarely notice without instrumentation. Routine nozzle cleaning and flame pattern checks alone typically recover 3–6% of fuel use, and O2 trim sensor calibration keeps that gain from silently reversing over the following weeks.
Skid Pipe Insulation Failure
Skid rails support every billet or slab passing through the furnace, and their water-cooling system is meant to be shielded by refractory insulation. Once that insulation cracks or falls away, the cooling water begins pulling heat directly out of the furnace atmosphere, and the loss keeps growing until the skid system is physically inspected and relined.
Refractory and Door Seal Degradation
Thinning refractory and worn charge/discharge door seals both raise wall and opening losses at the same time, and the two are frequently missed together because neither triggers an alarm on its own. A scheduled refractory thickness check paired with door seal inspection closes both gaps before they show up as a sustained rise in GJ per ton.
Hot Charge Ratio Not Tracked
Charging slabs or billets while they still retain heat from casting can save roughly 0.55 GJ per ton compared with fully cooled cold charge, but only if the transfer conveyor and charge scheduling are reliable enough to sustain a high hot-charge ratio. Conveyor downtime that goes unaddressed quietly erodes this saving month after month.
Turning Furnace Condition Data Into a Maintenance Action
The single biggest shift in reheat furnace energy management is not a better burner or a thicker refractory lining — it is connecting real-time furnace condition data to the maintenance work order system so that an efficiency deviation becomes a scheduled task instead of a line in a monthly report nobody reads until the quarter is already over. Continuous monitoring of stack temperature, O2 trim, skid water return temperature, and burner run hours reveals exactly which asset is driving a GJ-per-ton increase, days or weeks before the fuel bill confirms it. A digital maintenance record per furnace zone also means every burner service, refractory patch, and skid inspection is tied to the specific energy trend it affects, so plant teams can prove which maintenance actions actually moved the number rather than guessing.
We were chasing our reheat furnace fuel numbers a full month after they'd already gone wrong. With maintenance-linked energy monitoring in place, our RHF specific fuel consumption moved from 1.42 GJ per ton down to 1.11 GJ per ton over twelve months, and we can now point to the exact burner and skid work that got us there.
Rolling This Out Across a Steel Plant's Furnace Fleet
Most integrated and mini-mill plants run more than one reheat furnace, often alongside soaking pits, annealing furnaces, and ladle preheaters that draw on the same fuel supply and the same maintenance crew. Tracking GJ per ton on a single furnace is useful, but the real value shows up once every thermal asset reports into the same maintenance and energy system, because that is when a plant manager can see which furnace is dragging the whole plant's average up and prioritise the crew accordingly. A furnace-by-furnace view also makes it possible to compare two units of similar design side by side and settle arguments about whether a fuel rate gap is a burner problem, a skid problem, or simply a difference in charge mix — rather than relying on whichever engineer last walked the shop floor. Rolling out furnace-level energy tracking does not require replacing existing instrumentation; most plants connect their current combustion control and temperature sensors into the maintenance platform and start seeing a live GJ-per-ton trend within the first reporting cycle, with historical baselines built from whatever fuel metering data the plant already collects.
Frequently Asked Questions
What is a good GJ per ton target for a steel reheat furnace?
Below 1.0 GJ/t is considered world class, 1.0–1.3 GJ/t is good practice, and 1.3–1.6 GJ/t is a typical mixed-charge plant average. Above 1.6 GJ/t usually points to skid insulation loss, burner drift, or deferred refractory work. Oxmaint tracks your furnace's live fuel rate against these tiers automatically.
How much fuel does hot charging actually save?
Hot charging steel that retains heat from continuous casting typically saves around 0.55 GJ per ton compared with fully cooled cold charge, along with a meaningful gain in furnace throughput. The saving depends entirely on how consistently the transfer conveyor keeps charge temperature high.
What causes the biggest heat losses in a reheat furnace?
Flue gas and stack losses are usually the largest single share of wasted energy, followed closely by skid pipe cooling losses once insulation around the skid rails degrades. Wall, door, and scale-related losses add up further if refractory and seals are not inspected on a set schedule.
How often should burners and skid pipes be inspected?
Burner nozzle cleaning and flame pattern checks are typically scheduled on run-hour intervals, since drift accumulates with operating time rather than calendar days. Skid pipe insulation should be inspected on a fixed calendar cycle, since deterioration continues even during planned furnace downtime.
How does a CMMS help lower reheat furnace GJ per ton?
A CMMS ties burner, skid, refractory, and door seal maintenance directly to a live energy dashboard, so a rising fuel rate points straight to the asset responsible instead of triggering a plant-wide audit. Book a demo to see Oxmaint's furnace energy tracking on your own GJ-per-ton numbers.
Stop Losing GJ Per Ton to Maintenance You Can't See
Oxmaint gives steel plants one system for reheat furnace burner PM, skid and refractory inspection, and live energy tracking — so every GJ saved is backed by a maintenance record you can defend in the next review.