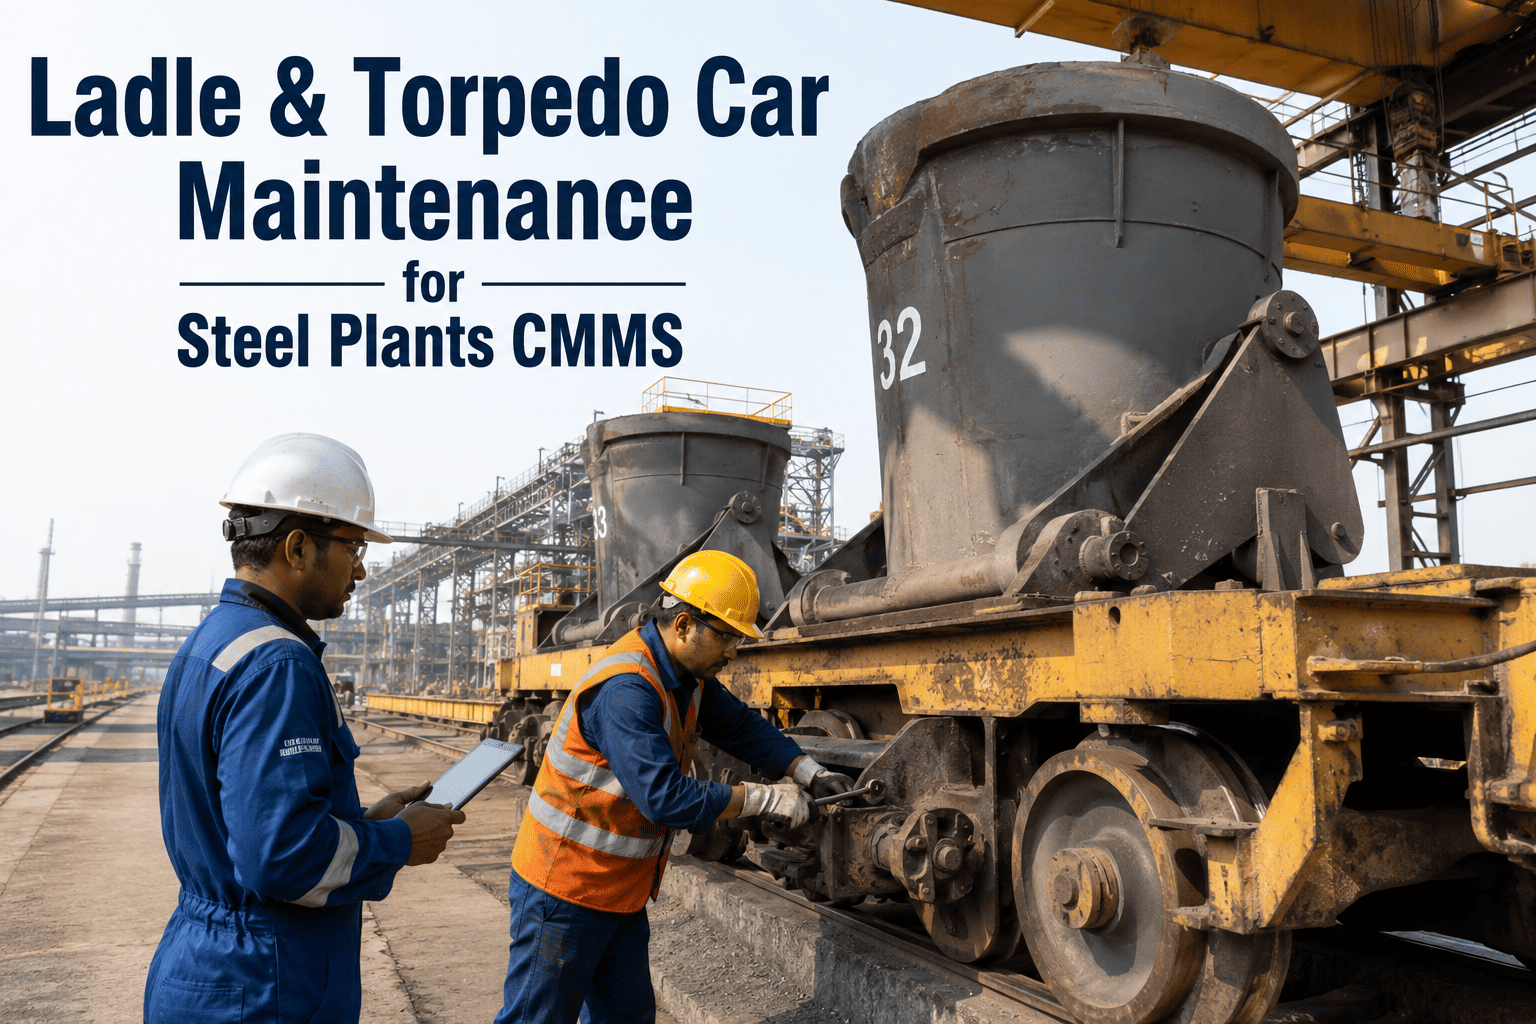
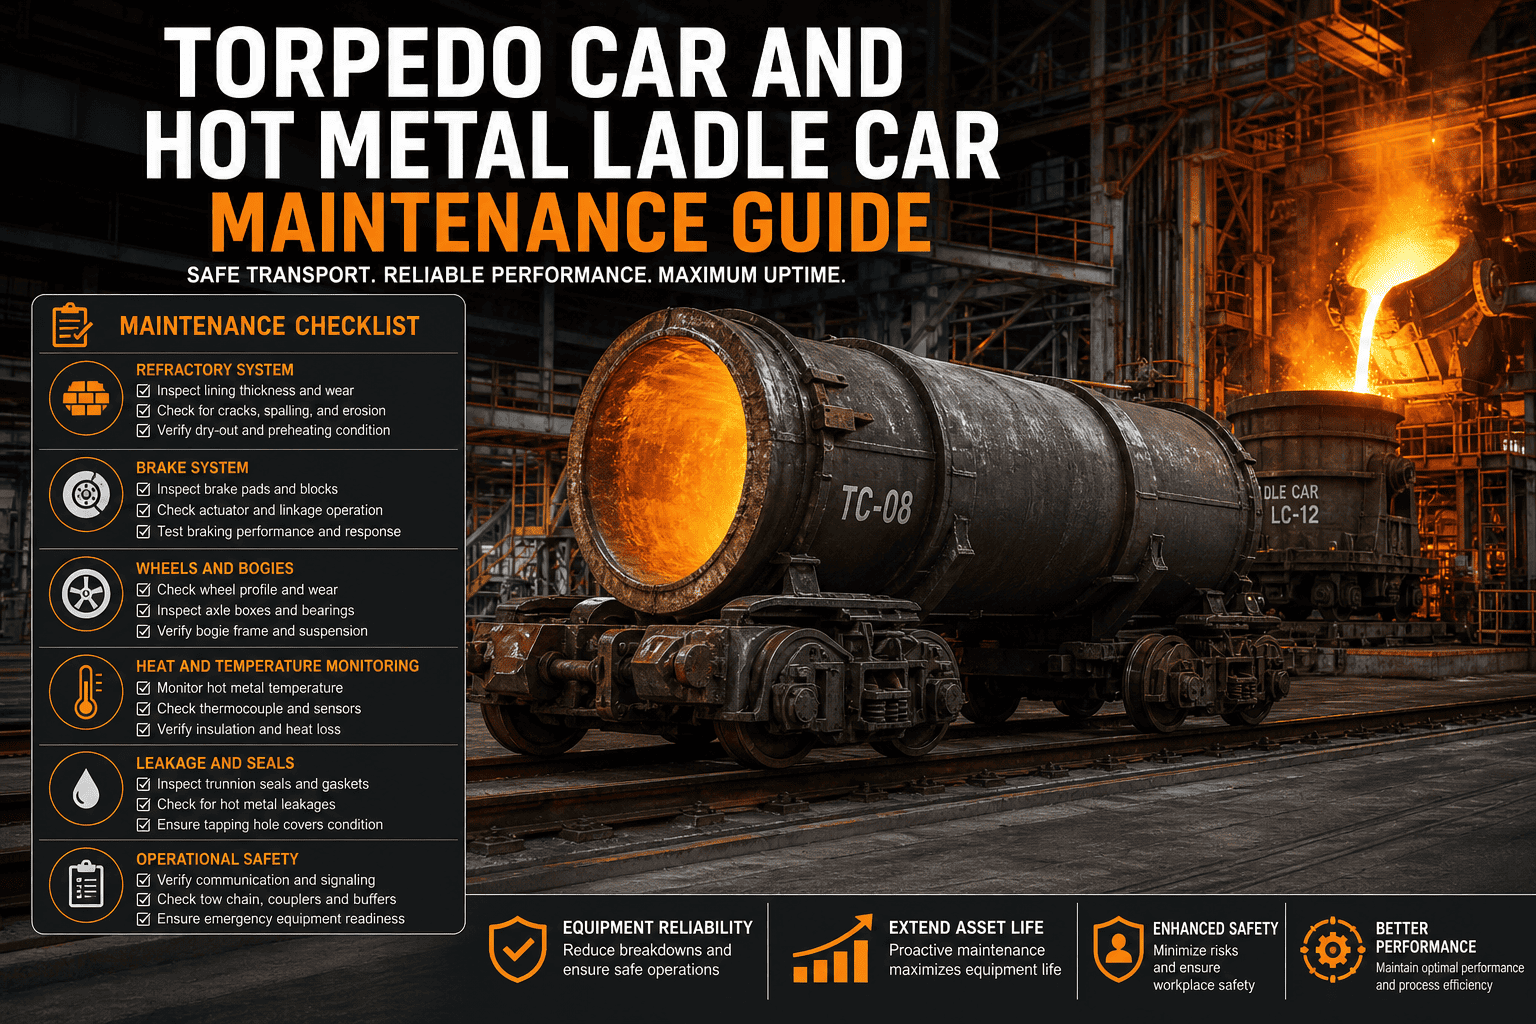
Torpedo cars transport molten iron at 1,400-1,500°C from blast furnaces to steelmaking vessels across kilometres of rail track. A single refractory breakthrough or brake failure at operating speed can release catastrophic quantities of liquid metal in uncontained areas, creating permanent safety hazards to personnel, neighbouring equipment, and facilities. The USA alone operates 3,200+ torpedo cars in active service at integrated steel plants. Each car carries 100-250 tonnes of liquid iron — failure consequences include fatalities, multi-million-dollar facility damage, environmental contamination, and regulatory shutdowns. Daily inspection of torpedo car refractory condition, traversing motor function, tilting mechanism, brake performance, and wheel flange condition is the first line of defense against these failure modes. Yet fewer than 35% of North American steel plants conduct documented daily torpedo car inspections before the car is released for operation.
Torpedo Car Daily Hot Metal Transport Inspection
Refractory integrity, traversing motor, tilting mechanism, brake system, and wheel flange daily pre-trip inspection with CMMS safety sign-off.
Why Torpedo Car Refractory Breakthroughs Happen
Torpedo cars operate on a heat cycle — each car is preheated before loading, filled with 1,400°C iron, transported to the steelmaking area, and then cooled during idle time waiting for processing. This repetitive thermal cycling stresses the refractory brick that lines the interior — each cycle expands and contracts the ceramic material, opening small cracks that grow over time. By the time thermal imaging detects a hotspot (a shell temperature rise indicating brick damage), the refractory has already been significantly compromised. The real prevention happens 4-8 weeks earlier, when slag-line wear becomes visible during daily inspection or when heat-count tracking shows a car approaching its maximum safe cycle limit.
Daily Torpedo Car Inspection Checklist Protocol
Refractory condition assessment requires two complementary methods: (1) Daily visual inspection of the slag line — the horizontal wear mark visible where liquid iron sits. Slag-line wear rate is the most sensitive early-stage indicator of refractory degradation. Measure slag-line erosion depth (typically 5-20mm per cycle for active service) and compare to baseline from previous inspection — accelerating erosion signals imminent brick failure. (2) Weekly thermal imaging of the shell surface. Normal shell temperature should be uniform around the circumference. A hotspot (>5-10°C above surrounding area) indicates a void or crack in the refractory underneath — a sign that brick fatigue is advanced. Record IR images and slag-line photos in CMMS with heat-count number of the car. Track erosion rate — if slag-line erosion exceeds 1.5x the car's normal rate, schedule major reline inspection within 2 weeks.
Every heat cycle (one fill-and-empty cycle) puts stress on the refractory. Manufacturer specifications define a heat-count limit — typically 350-500 heats before brick fatigue requires reline. Daily inspection must log the heat count for each torpedo car trip. CMMS calculates remaining cycles and alerts when the car approaches 80% of its heat-count limit. At that threshold, schedule a major refractory inspection and reline planning meeting — the car may be able to continue for 20-30 more heats if slag-line wear and thermal imaging show acceptable condition, or it may need immediate reline. Track cumulative heat count in CMMS asset record. This prevents the common failure where a car exceeds its design heat limit without anyone noticing.
Torpedo cars are moved on rail by a traversing motor — typically a direct-drive electric motor geared to the wheels. Daily mechanical assessment: (1) Start the traversing motor and listen for unusual sounds (grinding, squealing, chattering) indicating bearing wear; (2) Move the car slowly 20-30 feet forward and back — motion should be smooth with no hesitation, jerking, or binding; (3) Check the motor cooling fan is operating and the motor housing is not excessively hot (>60°C is a warning sign); (4) Verify the gearing is not leaking oil (check for oil spray on wheels or rails); (5) Inspect the motor mounting bolts for looseness; (6) Ensure the emergency stop mechanism on the traversing control is accessible and responsive. If motor motion is jerky, gears are grinding, or motor overheats, remove the car from service and schedule motor/drivetrain inspection before next use.
Torpedo cars tilt to pour molten iron into the steelmaking vessel — the tilting mechanism must operate smoothly and hold the car at tilt angle during the pour (which can last 2-3 minutes with 250 tonnes of liquid metal inside). Daily tilting system test (performed with empty car only): (1) Engage the tilting hydraulic system and slowly raise the car to its tilt angle (typically 25-35 degrees from vertical). (2) Observe motion for smoothness — no jerking, binding, or unusual pressure sounds. (3) Hold the car at tilt angle for 30 seconds — if hydraulic pressure drops and the car drifts back to horizontal, the tilt system is losing pressure and must be serviced. (4) Slowly lower the car back to horizontal. (5) Check hydraulic fluid level in the tilt system reservoir. Any pressure loss, jerky motion, or fluid leakage requires hydraulic system repair before loaded operation. Record tilt system pressure readings in CMMS if instrumentation is available.
Torpedo car brakes support 220 tonnes of car plus 100-250 tonnes of liquid iron — total weight exceeds 350 tonnes. Brake failure at speed could result in uncontrolled car motion and collision with furnace or blocking position, releasing liquid metal. Daily brake assessment: (1) With the car empty, apply full brakes and attempt to move the car manually — brakes should lock wheels immediately and prevent any motion. (2) Drive car at normal speed (typically 4-6 mph) and apply brakes — car should stop within 10 feet. Any longer stopping distance or brake slippage indicates pad wear. (3) On a grade (if available), apply brakes with the car empty and verify the car does not roll. (4) Check brake pedal or control feel — pedal should be firm and responsive. Soft, spongy, or non-responsive brakes indicate air in the hydraulic system or worn pads. (5) Inspect wheel brake pads visually — pads should show minimum 5-10mm thickness. Document brake performance in CMMS. If brakes slip, don't hold, or pads are worn thin, remove car from service and schedule brake reline immediately.
Torpedo car wheels have a flange (a raised lip on the wheel inside edge) that grips the rail and prevents the car from sliding sideways or jumping track. Under the weight of loaded operation, flange wear accelerates — excessive wear can reduce the flange thickness to a point where the wheel climbs the rail on a curve, causing derailment or collision. Daily wheel inspection: (1) Visually inspect the wheel flange on all four wheels — look for visible groove-wear pattern on the rail-facing surface; (2) Measure flange thickness with caliper at one point per wheel (record in CMMS). Baseline flange thickness is typically 40-50mm new — when worn to <20mm, risk of climb-out increases significantly; (3) Check for cracks in the wheel center or flange (look for radial or circumferential cracks); (4) Inspect the rail head for edge corrosion or wear that would reduce the flange's grip. If flange thickness is <20mm or cracks are visible, remove the car and schedule wheel replacement before next trip.
Torpedo Car Safety Compliance Transformation
Torpedo Car CMMS Daily Inspection Automation
Torpedo cars are mobile assets that spend time in blast furnace yards, on railway tracks, at steelmaking areas, and in maintenance bays — tracking daily inspection across locations requires a CMMS that works offline (in areas with no mobile signal) and syncs data when the car returns to connected areas. Oxmaint's torpedo car module tracks heat cycles, refractory condition, brake performance, and wheel wear in a single location-independent database. Alerts automatically flag when cars approach reline intervals or when inspection findings suggest imminent maintenance needs.
Torpedo Car Daily Inspection FAQs
What is the typical heat-count limit for torpedo car refractory before reline is required?
How do I measure slag-line erosion and interpret the wear rate trend?
What brake pad thickness is the minimum safe thickness for torpedo car operation?
How do I detect wheel flange wear before it becomes a derailment risk?
What is the correct procedure for daily tilting mechanism test with empty car?
When should I use thermal imaging vs. visual slag-line inspection for refractory assessment?
What does "normal" traversing motor sound like and what unusual sounds indicate bearing wear?
Prevent Refractory Failures Before They Happen
Torpedo car refractory breakthroughs are catastrophic events — 250 tonnes of 1,400°C liquid metal released in uncontained areas creates immediate safety hazards to personnel and facility infrastructure. Yet 88% of refractory failures are preventable through daily slag-line inspection and heat-count tracking. Oxmaint's torpedo car module automates heat-count calculation, slag-line erosion trending, and reline planning — converting refractory failures from emergencies to scheduled maintenance. Start a free trial with your torpedo car fleet specifications, or contact our transport safety expert to review daily inspection protocols specific to your operation.