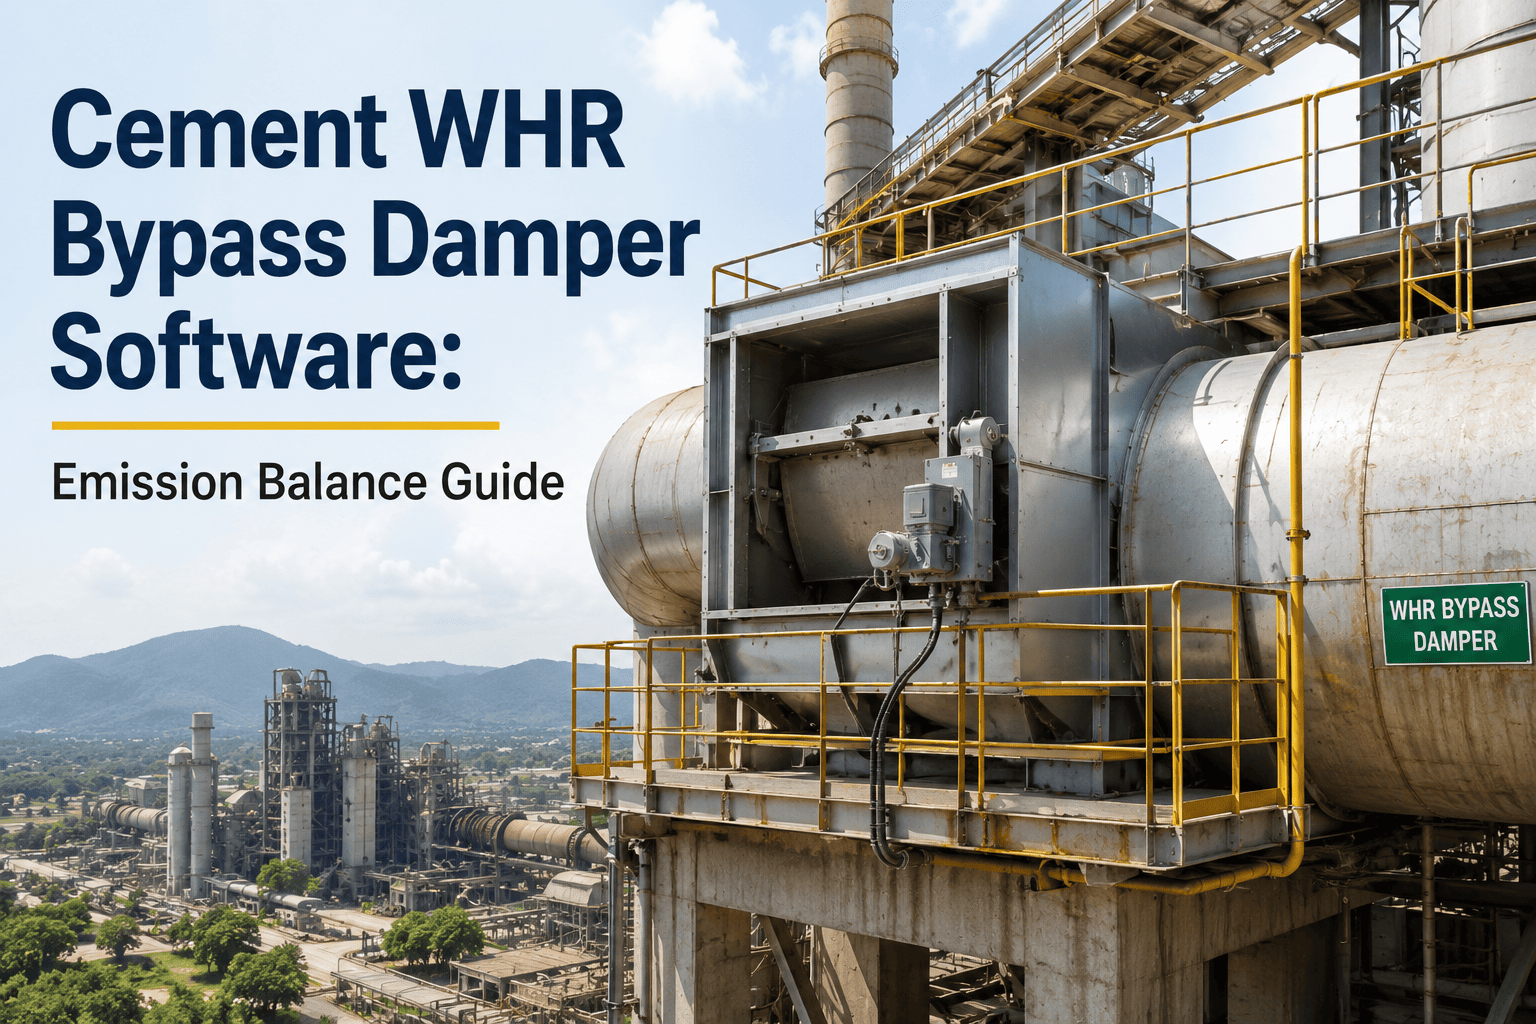
Every WHR-equipped cement kiln is running two systems that fight for the same hot gas at the same time. The waste heat recovery boiler wants as much preheater and cooler exhaust as it can get, because more gas volume and higher gas temperature mean more steam and more power generated on site. The bypass damper wants a slice of that same gas pulled away and quenched, because kiln gas loaded with volatile alkali chlorides has to be extracted before it condenses inside the preheater and starts building rings, coating collapses, and blocked risers. Push too much gas toward the WHR duct and chloride recirculation climbs until skinning forces an unplanned kiln stop. Open the bypass too wide to protect the kiln and WHR steam output drops, corrosion risk rises inside the quench and cooling ducts, and the power savings the WHR system was built to deliver quietly disappear.
Book a demo
to see how OxMaint tracks damper position, gas temperature, and bypass ratio side by side, so this trade-off is measured every shift instead of guessed once a quarter.
Cement WHR Bypass Damper Software · Emission Balance · OxMaint CMMS
Stop Choosing Between Kiln Stability and WHR Output. Track Bypass Damper Position, Gas Temperature, and Heat Recovery Together — In One Screen.
OxMaint gives cement plants a single, structured record of bypass damper position, actuator health, kiln gas temperature at every take-off point, and WHR boiler feed conditions — so the balance between chloride control and heat recovery is a data-driven setpoint, not a rotating operator's guess.
3–15%
of total kiln gas volume is typically diverted through the bypass duct on kilns burning alkali-rich or chloride-rich raw materials and fuels
~970°C
approximate gas temperature at the kiln inlet take-off point before quench cooling — the temperature window where dampers and refractory wear fastest
30%
electrical operational savings some WHR installations can deliver at a kiln when the system runs at design gas volume and temperature without interruption
2
A bypass damper is not a valve you set once — it is a moving trade-off between two operating goals that pull against each other every hour of the campaign. Every degree of extra bypass gas protects the preheater from chloride skinning but pulls heat away from the WHR boiler. Every reduction in bypass ratio protects WHR output but raises the risk of coating buildup, blocked cyclones, and an unplanned stop that costs far more than the power the WHR system saved that week. OxMaint gives reliability and process teams a shared, timestamped record of where that trade-off sits at any moment — and an alert before it drifts somewhere nobody chose on purpose.
Four Things OxMaint Tracks to Keep WHR Output and Kiln Stack Emission Control in Balance
DAMP — Damper Position & Actuator Health
Bypass Damper Position Logging and Actuator Wear Tracking
A bypass damper that sticks partway open — or partway closed — rarely announces itself. It shows up weeks later as a chloride trend that will not explain itself, or as a WHR output drop nobody can trace to a single cause. OxMaint logs commanded position against actual measured position at every reading, tracks actuator run-hours and torque trend, and flags drift between commanded and actual position before the gap becomes a stuck damper found only during a shutdown inspection. Every actuator gets its own maintenance history — seal condition, linkage wear, response time — instead of being buried in a general kiln auxiliaries work order.
Key Damper Parameters OxMaint Tracks
Commanded position vs measured position — logged at each control cycle reading
Actuator run-hours and torque trend — per damper, per campaign
Response lag — time between command and confirmed position change
Seal and linkage inspection history — with photos and technician notes
Damper Failures OxMaint Catches Early
Silent position drift — commanded and actual position diverge without alarm
Actuator torque climbing — early sign of linkage binding or seal fouling
No inspection record — damper condition unknown between planned shutdowns
TEMP — Gas Temperature & Chloride Threshold
Take-Off Gas Temperature and Chloride Trend Monitoring
Bypass gas leaves the kiln inlet extremely hot and has to be quenched fast, before dust and alkali chloride vapour condense onto duct walls and cause acid corrosion or blockage. Run the quench too aggressively and you lose recoverable heat that could have gone to the WHR boiler feed; run it too gently and you risk fouling downstream equipment. OxMaint records gas temperature at the take-off point, after quench, and at WHR boiler inlet for every shift, trends chloride concentration readings from lab results against bypass ratio, and flags when the relationship between the two starts drifting away from the plant's established operating band.
Key Temperature Parameters OxMaint Tracks
Take-off gas temperature — recorded per shift at the kiln inlet extraction point
Post-quench temperature — verified against the target cooling window
Chloride/alkali lab result trend — plotted against bypass ratio over time
WHR boiler inlet temperature — the figure that determines recoverable heat
Temperature Failures OxMaint Catches Early
Over-cooling — quench set too low, acid condensation risk rises unnoticed
Under-cooling — dust and chloride carryover risk to downstream ductwork
No chloride correlation — bypass ratio changed without checking lab trend
RATIO — Bypass Ratio vs WHR Output
Bypass Ratio and WHR Steam Output Correlation Analytics
Process teams often adjust bypass ratio to solve a kiln stability problem without a clear view of what that change costs the WHR boiler downstream, and power teams often push for lower bypass without visibility into the chloride trend that decision creates. OxMaint puts both readings on the same timeline — bypass ratio percentage against WHR steam output and generated power — so every adjustment is visible to both teams, and the plant can see, in numbers, what a one-percent bypass change actually costs or saves across a full production week.
Key Ratio Parameters OxMaint Tracks
Bypass ratio — percentage of total kiln gas diverted, logged per shift
WHR steam output and generated power — recorded on the same shift timeline
Ratio change log — who adjusted it, when, and the stated reason
Weekly heat-loss estimate — recoverable heat diverted through the bypass
Ratio Coordination Failures OxMaint Prevents
Unlogged ratio changes — adjustment made with no reason or owner recorded
Process and power teams working from different numbers on the same shift
No weekly view — bypass cost only visible after the monthly report is closed
DUST — Dust Extraction & Corrosion Risk
Bypass Dust Handling and Duct Corrosion Inspection Scheduling
Bypass dust carries a high concentration of alkali chlorides and needs its own extraction, cooling, and handling path — one that is prone to buildup, blockage, and acid corrosion where cooled gas meets duct steel. Left unscheduled, duct inspection becomes reactive: a pressure drop climbs, a fan trips, or a leak is found during a walk-through that should have been caught weeks earlier. OxMaint schedules duct and dust-handling inspections on a fixed interval tied to bypass run-hours, tracks wall-thickness and corrosion readings by duct section, and opens a work order automatically when a section is due or a reading crosses the plant's wear limit.
Key Dust & Duct Parameters OxMaint Tracks
Duct wall-thickness readings — by section, trended across inspection cycles
Dust collector pressure drop — logged against bypass ratio and run-hours
Fan and conveyor condition — for the dedicated bypass dust handling line
Inspection due dates — tied to cumulative bypass run-hours, not calendar only
Dust & Corrosion Failures OxMaint Prevents
Inspection interval missed — duct wear found only after a leak or trip
Pressure drop rising unnoticed — early collector fouling not investigated
No wall-thickness trend — corrosion rate unknown until a section fails
OxMaint · Cement Plant CMMS
Damper Position Logged. Gas Temperature Trended. Bypass Ratio Tied to WHR Output. One Record Both Teams Can Read.
OxMaint turns bypass damper operation from a set-and-forget valve into a tracked, trended, and shared operating parameter — so the plant can defend every ratio change with data instead of a shift log entry.
Three Ways OxMaint AI Keeps the Bypass-vs-WHR Balance From Drifting
Capability · Drift Detection
Damper-vs-Chloride Correlation Alerts
OxMaint compares recent bypass ratio changes against the chloride lab trend and flags the moments where the two stop moving together — the earliest sign that a damper is not doing what its position readout claims, or that a ratio change is not achieving its intended effect.
Outcome: chloride drift investigated within the shift it starts, not the week it is noticed
Capability · Output Impact
WHR Output Loss Estimator
Each time bypass ratio is increased to manage a process condition, OxMaint estimates the associated WHR steam and power loss against recent baseline output — giving process and power teams a shared, immediate figure instead of a debate resolved after the monthly energy report.
Outcome: every stability-driven ratio change comes with its power cost attached
Capability · Maintenance Scheduling
Run-Hour Based Inspection Scheduling
Damper actuators, quench nozzles, and dust-handling ducts wear according to bypass run-hours, not the calendar. OxMaint schedules inspection and maintenance work orders against cumulative run-hours per component, so wear-driven parts are checked when they are actually due.
Outcome: inspection timing matches actual wear exposure, not a fixed monthly date
Bypass Operation Risk Register — Where Drift Between Emission Control and WHR Output Costs the Most
High — Kiln Stability
Bypass Ratio Too Low for Raw Mix Alkali Load
When bypass ratio is trimmed to protect WHR output without checking the current raw mix chloride load, alkali chlorides recirculate through the preheater faster than the bypass can remove them, building coating and skinning risk that ends in an unplanned kiln stop.
High — Corrosion
Quench Temperature Set Too Low for Extended Periods
Over-quenching bypass gas to protect downstream equipment can push duct wall temperature into the range where acid condensation accelerates corrosion — a slow failure mode that is invisible until a wall-thickness reading or an unplanned leak reveals it.
High — Actuator
Damper Position Drift Uncaught Between Inspections
A damper reporting a commanded position that no longer matches its actual position can leave the plant operating well outside its intended bypass ratio for days, with process and power teams both working from an incorrect assumption of current state.
Elevated — Coordination
Ratio Changes Made Without a Logged Reason
When bypass ratio is adjusted informally, with no recorded reason or owner, later analysis of a chloride excursion or a WHR output dip cannot separate a deliberate operating decision from an unexplained equipment issue.
Elevated — Dust Handling
Dust Collector Pressure Drop Rising Gradually
A slow rise in bypass dust collector pressure drop is easy to miss shift to shift, but it signals fouling that eventually forces a fan to work harder, raises trip risk, and can push the plant to trim bypass ratio for the wrong reason.
Elevated — Reporting
Process and Power Teams Reading Different Numbers
Without a shared timeline of bypass ratio against WHR output, process and power teams frequently work from different, informally kept figures — slowing root-cause analysis whenever output or emission control both need explaining at once.
Bypass Damper Operating Parameters — What OxMaint Records at Each Reading
| Parameter | Where It Is Measured | Why It Matters | OxMaint Tracking |
|---|---|---|---|
| Damper position | Kiln inlet bypass take-off | Sets the actual bypass gas volume against the commanded setpoint | Logged per cycle, drift alert |
| Gas temperature | Take-off, post-quench, WHR inlet | Determines corrosion risk and recoverable heat available to WHR | Trended by shift and location |
| Chloride/alkali content | Lab result from bypass dust or gas sample | Direct indicator of skinning and preheater coating risk | Correlated against bypass ratio |
| WHR steam output | WHR boiler feed and turbine | Shows the power-generation cost of any bypass ratio increase | Plotted on shared shift timeline |
| Duct wall thickness | Bypass duct sections, dust handling line | Tracks corrosion progression before a leak or failure occurs | Scheduled by run-hour interval |
| Collector pressure drop | Bypass dust collector | Early signal of fouling before a fan trip or blockage | Trended against bypass run-hours |
1 Screen
where damper position, gas temperature, chloride trend, and WHR output all sit on the same shift timeline, instead of four separate logs across two teams
Run-Hour
based inspection scheduling for dampers, quench nozzles, and ducts — matching maintenance timing to actual bypass wear exposure, not a fixed calendar date
Shared
ratio-change log that records who adjusted bypass position, when, and why — so later analysis can separate a deliberate decision from an equipment fault
3–15%
typical bypass gas volume range across kilns, depending on raw mix and fuel alkali and chloride load
750°C
approximate target range some plants quench bypass gas toward before it reaches boiler or filtration equipment
2 Teams
process and power generation groups that both need visibility into the same bypass ratio decision, on the same timeline
Run-Hours
the unit OxMaint uses to schedule bypass component inspection, since wear tracks operating exposure, not the calendar
Our process team would trim the bypass to chase a coating problem and the power team would only find out from the shift report the next morning, after output had already dropped. We were not disagreeing about the physics, we just did not have one place where both readings lived. Since we started logging damper position, gas temperature, and WHR output together in OxMaint, ratio changes get discussed before they happen instead of explained after. Two teams reading the same number changed the conversation completely.
— Plant Reliability Engineer, WHR-Equipped Cement Plant, OxMaint user
Frequently Asked Questions — Cement WHR Bypass Damper Software
What does a WHR bypass damper actually control in a cement kiln?
It sets how much hot kiln gas is diverted away from the main preheater and WHR path to be quenched and filtered, removing alkali chlorides before they recirculate and cause coating or ring formation inside the kiln system. Sign in to OxMaint to see damper tracking set up for your kiln.
Why does increasing bypass ratio reduce WHR output?
Gas diverted through the bypass duct is quenched and removed from the process rather than passed through the WHR boiler feed, so the heat and volume that could have generated steam is instead used to protect the kiln from chloride buildup.
How does OxMaint help balance emission control against WHR power output?
OxMaint logs damper position, gas temperature, chloride trend, and WHR steam output on one shared timeline, so any ratio change is visible to both process and power teams with its likely output cost attached. Book a demo to see this in your plant's data.
How often should bypass damper actuators and ducts be inspected?
Wear tracks operating exposure more closely than calendar time, so OxMaint schedules inspections against cumulative bypass run-hours for each component rather than a fixed monthly or annual date alone.
Can OxMaint be used across multiple kilns with different bypass configurations?
Yes. Each kiln's bypass system, take-off points, and operating bands are configured independently, while reporting and inspection scheduling stay on one shared platform. Sign in to OxMaint to configure bypass tracking per kiln line.
The Bypass-vs-WHR Trade-Off Will Not Stop Happening. It Just Needs to Be Visible to Both Teams Before It Costs a Kiln Stop or a Week of Lost Power.
Damper position and actuator health. Gas temperature and chloride trend. Bypass ratio against WHR output. Run-hour based inspection scheduling. OxMaint puts every part of the balance on one record, so the next ratio change is a decision, not a guess.