Compressed air leak management in manufacturing facilities is one of the highest-impact maintenance priorities plant teams can act on today. Undetected leaks silently drain compressed air systems of 20 to 30 percent of total output — driving up energy costs, reducing system pressure, accelerating compressor wear, and masking the true reliability picture of your production environment. With Sign Up Free on Oxmaint, plant maintenance teams can build a structured leak detection and repair program backed by automated work orders, asset-linked inspection records, and real-time KPI tracking across every facility.
Why Compressed Air Leaks Are a Major Manufacturing Cost Driver
Compressed air is the fourth utility in most manufacturing plants — and the least monitored. Unlike electricity or water, compressed air leaks produce no visible spillage and cause no immediate alarm. Yet a single 1/8-inch leak at 100 PSI wastes over 25 CFM continuously. Multiplied across dozens of fittings, hose connections, valves, and tool couplings across a typical plant floor, the cumulative energy waste reaches tens of thousands of dollars annually. Book a Demo to see how Oxmaint centralizes leak detection workflows across multi-site manufacturing portfolios.
Compressed Air Leak Detection Methods for Manufacturing Plants
Effective leak detection requires a combination of ultrasonic detection tools, scheduled inspection routes, and documented repair workflows. The method you choose determines how quickly leaks are found and how reliably they are eliminated before re-emerging during the next production cycle. Sign Up Free to build digital inspection routes and auto-assign repair work orders when leaks are confirmed.
Ultrasonic detectors convert high-frequency leak noise into audible signals, allowing technicians to locate leaks in pressurized systems while production is running. Effective across noisy plant environments where soapy water tests are impractical. Oxmaint inspection checklists can be assigned to each ultrasonic survey route with QR-coded asset scan points for precise location tagging.
Oxmaint's AI Vision Camera, powered by NVIDIA technology, continuously monitors compressed air systems for thermal anomalies and pressure differential indicators that precede visible leak symptoms. Persistent camera coverage of high-leak-probability zones eliminates dependence on periodic manual walkthroughs for critical supply lines and distribution headers.
Tracking system pressure at multiple points across the distribution network during non-production hours establishes a leak rate baseline. Rising pressure loss between surveys signals increasing aggregate leak volume before individual leak locations are identified. Oxmaint's analytics dashboard displays pressure KPI trends over time, flagging deterioration automatically.
Structured inspection rounds using Oxmaint's mobile app allow technicians to log leak findings by asset, location, severity, and estimated flow rate directly from the plant floor. Each finding auto-generates a corrective work order with priority assignment, parts requirements, and estimated repair cost — no paper forms, no missed follow-ups.
Compressed Air Leak Repair Prioritization Framework
Not all leaks carry equal urgency. A prioritization framework that scores leaks by flow rate, location criticality, and repair difficulty allows maintenance teams to maximize energy savings per repair hour and avoid diverting resources to low-impact fixes while high-waste leaks continue running. Book a Demo to see how Oxmaint's work order priority matrix supports structured leak repair scheduling.
| Leak Severity | Estimated Flow Loss | Common Locations | Repair Priority | Oxmaint Action |
|---|---|---|---|---|
| Critical | > 20 CFM | Header joints, regulator outlets | Same-day | Auto-generated P1 work order |
| High | 10–20 CFM | Valve packing, flex hoses | Within 48 hours | P2 work order with parts alert |
| Medium | 3–10 CFM | Tool couplings, fittings | Next scheduled PM | Batched into PM work order |
| Low | < 3 CFM | Thread connections, gauges | Monthly round | Logged for trend monitoring |
Building a Compressed Air Leak Management Program with Oxmaint CMMS
Asset Registry and System Mapping
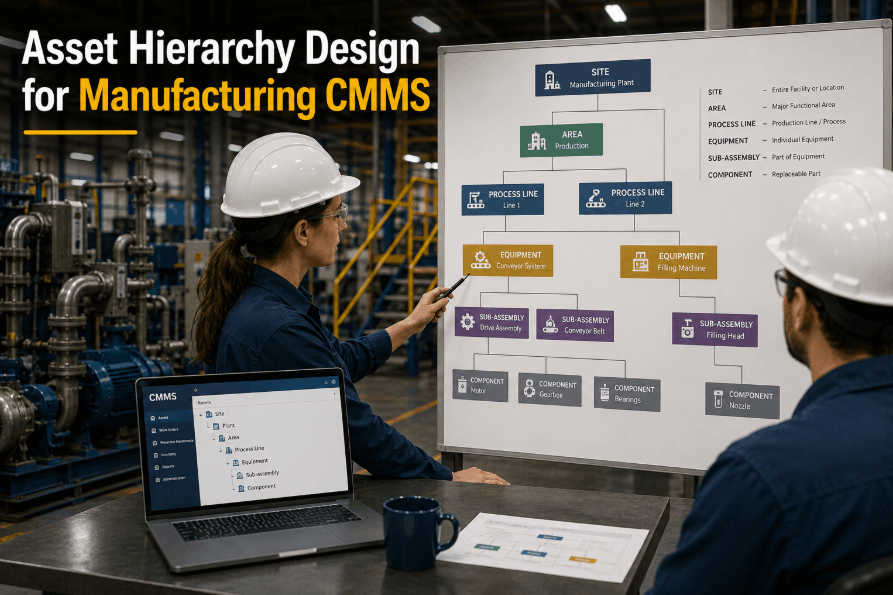
Register every compressed air asset in Oxmaint — compressors, dryers, receivers, distribution headers, drop legs, and end-use connections. Assign QR codes to each node so inspection findings are tied to precise asset locations. A complete asset map is the foundation of a repeatable leak detection program and the starting point for energy cost attribution by zone.
Inspection Schedule and Checklist Configuration
Configure recurring inspection routes in Oxmaint with pre-built compressed air checklists covering visual inspection, ultrasonic survey, pressure reading, and fitting condition. Set inspection frequency by zone risk level — high-pressure headers monthly, distribution drops quarterly. Automated reminders and mobile-first checklists eliminate scheduling gaps that allow leaks to accumulate undetected.
Automated Work Order Generation on Leak Detection
When a technician logs a leak finding during an Oxmaint inspection, the platform automatically generates a corrective work order with pre-populated asset data, leak severity classification, and parts recommendations drawn from inventory. This eliminates the gap between detection and repair that causes most leak programs to stall after the initial survey.
Repair Verification and Energy Savings Tracking
Oxmaint's work order completion workflow requires technicians to document post-repair pressure readings and confirm leak elimination before closing the order. This verification data feeds directly into the analytics dashboard, where cumulative CFM recovered and estimated energy cost savings are calculated automatically — providing the documentation needed to justify ongoing program investment to plant leadership.
Recurrence Monitoring and Predictive Pattern Analysis
Oxmaint's predictive maintenance module tracks which asset locations experience repeat leaks and identifies failure patterns tied to operating conditions, maintenance history, or component age. Locations with high recurrence frequency trigger automatic escalation to engineering review — enabling root cause resolution rather than repeated patch repairs that consume technician time without solving the underlying failure mode.
Compressed Air Leak Management KPIs to Track in Your CMMS
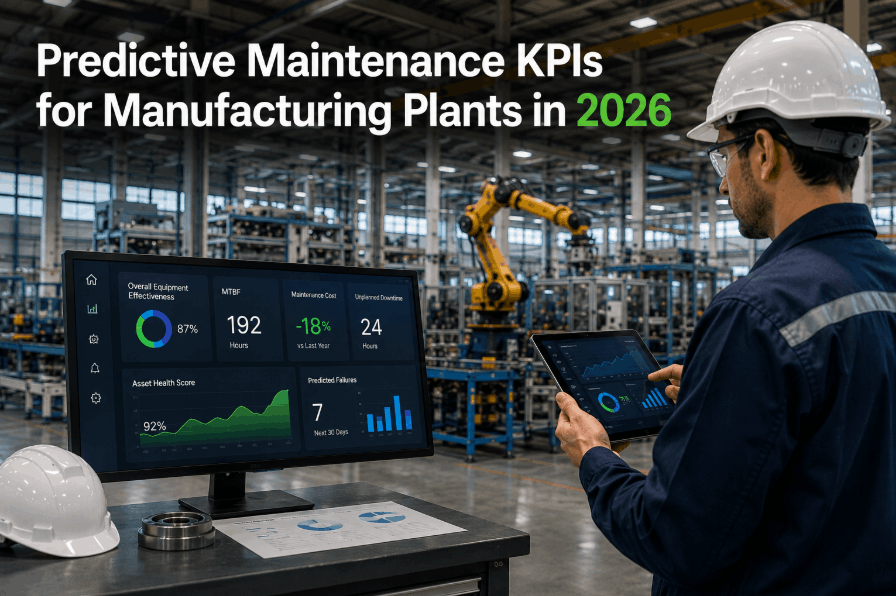
Measuring program performance with the right KPIs gives plant managers the data needed to demonstrate ROI, identify declining system integrity, and benchmark performance across shifts, departments, or facilities. Sign Up Free to access Oxmaint's live maintenance KPI dashboards pre-configured for manufacturing plants.
Tracks leaks identified per inspection round. A declining LDR following repair completion confirms program effectiveness; a rising LDR indicates system deterioration requiring frequency adjustment.
Measures the average time from leak detection to confirmed repair completion. Long MTTR on high-flow leaks directly translates to measurable energy cost that accumulates between detection and fix.
High recurrence on specific assets signals inadequate repair quality, incorrect component selection, or a systemic operating pressure issue that requires engineering-level resolution beyond routine maintenance.
Cumulative airflow recovered through completed repairs quantifies the direct output of the leak management program and feeds the energy cost savings calculation used in capital budget justification.
Rising compressor runtime without corresponding production demand increase is the leading system-level indicator of aggregate leak growth — detectable through Oxmaint's equipment runtime analytics before pressure symptoms appear at the point of use.
Tracks whether scheduled leak detection inspection rounds are completed on time. Compliance below 85% is the single strongest predictor of accumulated undetected leak volume entering the following quarter.