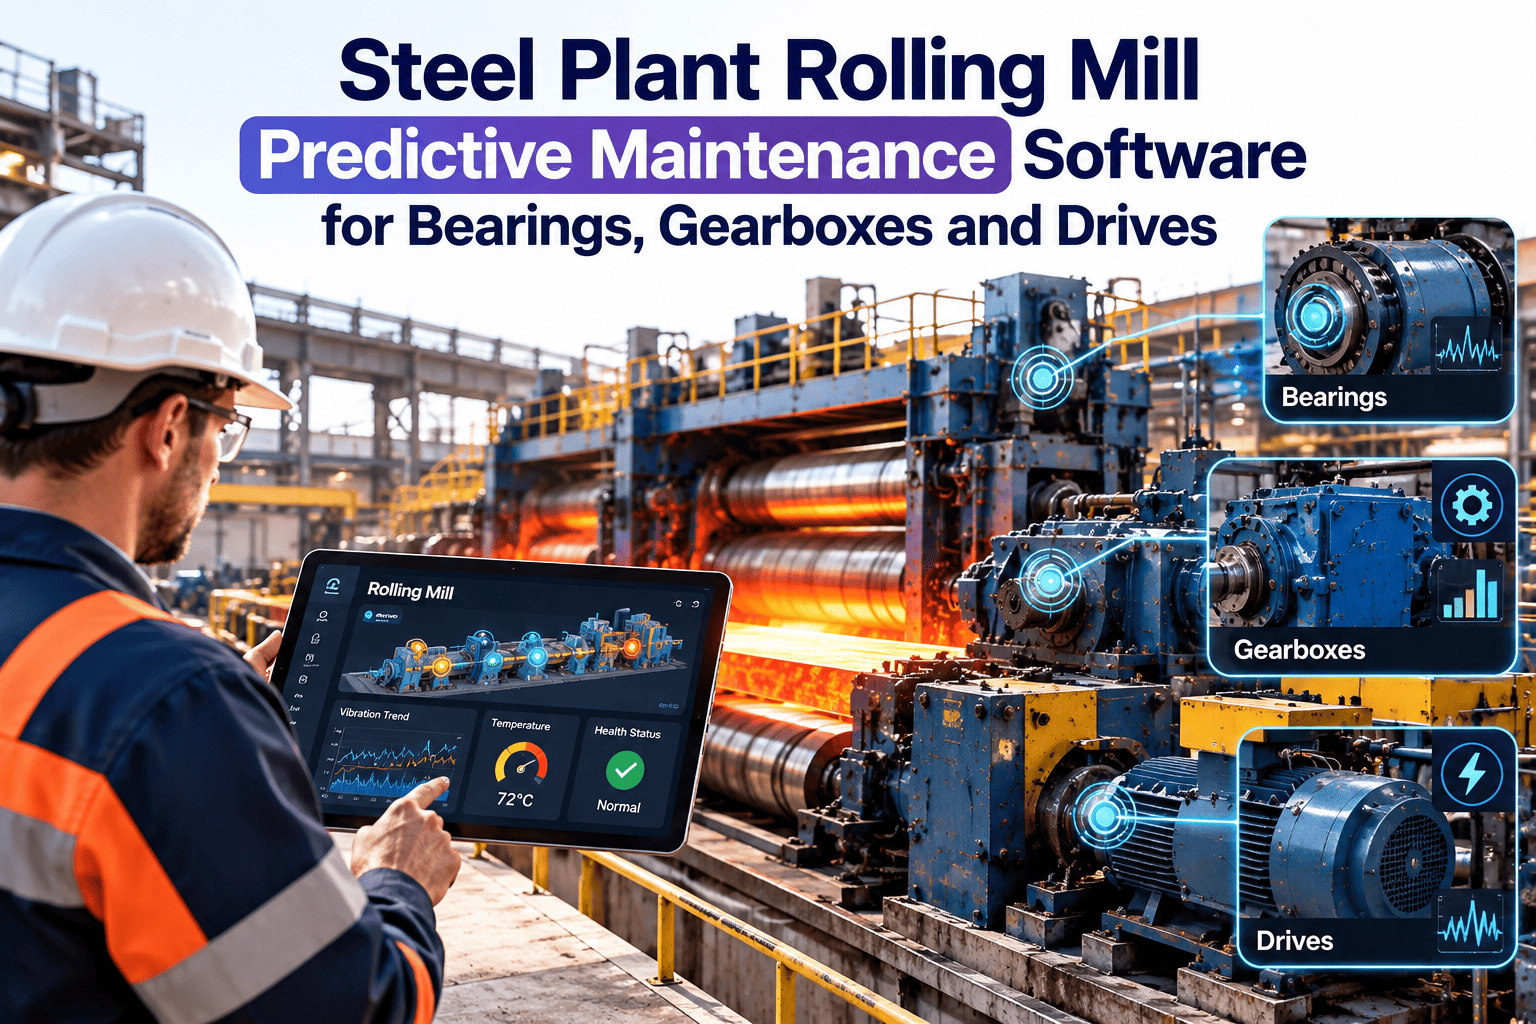
A rolling mill stops production the moment one bearing seizes, one gearbox loses its oil film, or one drive trips under load. The cost is rarely the part itself. It is the cold slab waiting in the furnace, the coil schedule that collapses, and the shutdown nobody planned for. Most of these failures announce themselves days or weeks earlier through heat, vibration, noise, and oil condition, but the signals sit in separate systems and notebooks. This guide shows how to turn those signals into a controlled response for bearings, gearboxes, and drives, and you can book a demo to see how Oxmaint connects condition data to work orders.
Rolling Mill Predictive Maintenance Software for Bearings, Gearboxes and Drives
Link vibration, temperature, and oil condition from the mill drive train to automated work orders, so the plant fixes the weak component in a planned window instead of a forced stop.
Why Mill Failures Surprise Plants That Already Collect Data
Predictive maintenance software does not replace condition monitoring hardware. It sits behind it, receives the readings, applies rules, and turns each meaningful change into a tracked job with an owner and a due date.
Reading the Warning Signs on Mill Gearboxes and Bearings
Industry guidance on rolling mill gearboxes consistently points to the same early signs: rising housing or oil temperature, changes in noise, new vibration, and oil that looks or smells wrong. The table links each sign to a likely cause and a sensible first response.
| What is observed | Likely cause | First response | Urgency |
|---|---|---|---|
| Rising oil or housing temperature | Low oil level, degraded oil, overload, blocked cooling | Check level and cooler, compare with baseline load | High if rapid |
| Grinding noise | Gear wear, damaged teeth, debris in oil | Sample oil, inspect magnetic plug, plan inspection | High |
| Knocking | Loose internals, broken bearing cage, cracked tooth | Reduce load and arrange immediate inspection | Critical |
| High-pitched whine | Gear mesh problem or lubrication starvation | Check lubrication supply and mesh pattern | Medium to high |
| Rattle in housing or coupling | Loose mounting, foundation bolts, misalignment | Verify bolt torque and alignment at next stop | Medium |
| Vibration rising with noise and heat together | Advanced component damage | Treat as imminent failure and escalate | Critical |
| Seal leaks or smoking breather | Seal wear, thermal expansion, pressure buildup | Repair seal, check oil contamination | Medium |
Root Causes Worth Designing Around
- Lubrication faults: wrong grade, low level, degraded oil, or contamination from scale, dust, and water.
- Misalignment: even small shaft offsets can drive heavy vibration, and soft foot makes it worse.
- Overload: operating beyond rated capacity damages teeth and shortens bearing life.
- Seal failure: contaminants enter, oil leaks out, and the unit can run dry.
- Imbalance in shafts and couplings that gradually loads bearings.
Give Every Mill Alarm an Owner, a Task, and a Deadline
Oxmaint turns condition readings into work orders with assignment, parts, and scheduling, so a rising trend becomes a planned repair.
Four Monitoring Tiers, From Daily Rounds to Shutdown Checks
Vibration readings are usually judged against severity guidance such as the ISO 20816 series, which supersedes the older ISO 10816 series. Use the standard as a reference, then tune alert levels to each machine's own baseline.
A Three-Level Response Ladder for Condition Alerts
Why Two Signals Beat One
A single sensor can mislead. A rise in oil temperature during a heavy rolling schedule may be normal, while the same rise with new vibration is not. Rules that require agreement between signals reduce false alarms and build trust with the crew.
From Sensor Reading to Closed Work Order
What to Monitor on Each Class of Mill Asset
| Asset | Typical signals | Typical work order | Planning note |
|---|---|---|---|
| Roll chock bearings | Bearing temperature, seal condition, grease or oil state | Bearing inspection or replacement at roll change | Align with roll change cycles |
| Mill gearbox | Vibration spectrum, oil temperature, debris, noise | Oil change, mesh inspection, bearing replacement | Needs a long planned window |
| Main drive motor | Winding and bearing temperature, vibration, current | Cleaning, bearing service, insulation check | Coordinate with electrical team |
| Spindles and couplings | Backlash, vibration, lubrication condition | Re-lubrication, joint replacement, alignment | Inspect at every major stop |
| Hydraulic and lubrication units | Pressure, filter condition, oil cleanliness | Filter change, pump service | Failure here damages bearings downstream |
| Cooling water systems | Flow, temperature, quality | Cleaning, valve and pump repair | Poor cooling raises bearing and roll temperature |
Condition Data Used Reactively and Predictively
- Alarms acknowledged but not followed by a task
- Oil results filed and rarely compared over time
- Parts ordered after the failure
- Repairs forced into unplanned stops
- Failure cause recorded in a few words, if at all
- Every meaningful alert becomes a work order
- Oil and vibration trends sit on the asset record
- Parts reserved when the trend crosses a limit
- Repairs placed in planned windows
- Findings feed back into limits and checklists
How Oxmaint Fits the Predictive Workflow
Oxmaint is the maintenance management layer. It does not replace sensors or analyzers. It receives condition information, links it to assets, and manages the response. Integration with your existing monitoring systems should be scoped in a walkthrough.
Protecting Bearings and Gears Before They Show Symptoms
Many mill bearing and gear failures begin with lubricant that is degraded, contaminated, or simply too low. Scale, dust, and cooling water are constant threats in a rolling environment, so lubrication discipline is a predictive measure in its own right.
| Lubrication issue | What it does to the asset | Preventive task to schedule |
|---|---|---|
| Low oil level | Starves gears and bearings, raises temperature | Daily sight glass check recorded on a round |
| Wrong grade or mixed oil | Loses film strength under load | Controlled top-up with the approved grade only |
| Water or scale contamination | Pits bearing surfaces and accelerates wear | Seal inspection and scheduled oil sampling |
| Degraded or oxidized oil | Reduces protection and carries debris | Oil change based on analysis, not only hours |
| Blocked breather or cooler | Traps heat and pressure, damages seals | Cleaning task tied to temperature trend |
| Grease starvation or over-greasing | Overheats chock bearings or blows seals | Defined quantity and interval per bearing |
Checks Worth Recording Every Round
- Oil level, colour, foaming, and any water separation in the sight glass.
- Housing temperature by infrared reading, with the load condition noted.
- New or changed noise compared with the recorded baseline sound.
- Seal leaks, smoking breathers, and oil on the floor around the drive.
- Coupling guard and foundation bolt condition.
Planning the Repair Window and the Parts Behind It
Prediction only pays off if the plant can act on it. That means knowing which stops are available, how long each repair needs, and which spares have long lead times.
| Planning question | Why it matters | What to record |
|---|---|---|
| How long does the repair need? | Decides whether a short stop is enough or a major outage is required | Standard duration and crew size per task |
| Is the spare on site? | A missing bearing turns a planned job into an emergency | Stock level, location, and supplier lead time |
| Is a rebuilt unit available? | Swapping a gearbox can shorten downtime | Spare unit status and last overhaul date |
| Which stop is next? | Jobs should be matched to real windows | Planned stop calendar and open jobs |
| What else is due on the same asset? | Bundling jobs saves stops | Related preventive tasks and open defects |
When a condition trend reaches the planning level, the work order should already list the parts, the estimated duration, and the stop it is aimed at. That is the difference between a warning and a plan.
Roles in a Working Predictive Programme
| Role | Daily responsibility | Review responsibility |
|---|---|---|
| Mill operator | Reports unusual noise, heat, or vibration through the round checklist | Confirms that reported issues were actioned |
| Maintenance technician | Completes rounds, records readings, and executes work orders | Flags noisy alerts and missing steps |
| Condition monitoring engineer | Reviews trends and sets limits | Tunes thresholds and validates findings |
| Maintenance planner | Places jobs into stops and reserves parts | Reports planned versus forced stops |
| Mill manager | Approves stop windows and priorities | Reviews downtime and reliability trends |
Mistakes That Undermine Condition-Based Programmes
- Setting alarm limits from a generic table and never adjusting them to the machine.
- Closing an alert without recording what was found, which erases the learning.
- Monitoring a gearbox but ignoring the lubrication and cooling systems feeding it.
- Treating every alert as urgent, which trains the crew to ignore them all.
- Keeping oil analysis results in a separate folder from the asset record.
Turning Open Condition Jobs Into a Shutdown Scope
When condition work orders accumulate in one place, shutdown planning starts from evidence. Review them before each major stop so the scope reflects what the machines have been reporting.
- List every open condition job by asset, with its trend and the date it crossed the planning level.
- Confirm parts are on site or have confirmed delivery dates before the stop begins.
- Bundle alignment checks, bolt torque verification, and lubrication tasks with the major repairs.
- Assign crews and estimated durations so the critical path is visible.
- After the stop, record findings and compare them with the predicted condition.
How to Tell the Program Is Working
A Practical Start on One Mill Line
Rolling Mill Predictive Maintenance Questions
Not necessarily. Daily rounds and existing readings can feed the workflow first, and you can sign up to set up inspection routes.
Start with assets whose failure stops the line and whose spares take longest to obtain, usually main gearboxes, drives, and chock bearings.
Require two agreeing signals for higher levels and review false alerts monthly. Tuning limits to each machine's baseline matters most.
No, it manages the response to their readings. You can book a demo to review integration options.
Open condition jobs, reserved parts, and task lists give planners a ready scope instead of a guess.
Turn Mill Condition Signals Into Planned Repairs
Connect bearing, gearbox, and drive condition data to assigned work, reserved spares, and a failure history your team can learn from.