When a 280-ton steel ladle failed catastrophically during transfer at a Gulf Coast integrated mill, the refractory breakthrough didn't just release molten steel onto the melt shop floor—it ended three careers, hospitalized seven workers with severe burns, triggered an 18-month OSHA investigation, and ultimately cost the company $127 million in direct damages, legal settlements, and lost production. The post-incident forensic analysis revealed that the ladle's working lining had been worn to 31% of minimum safe thickness in the slag zone—a condition that routine thickness monitoring would have detected four campaigns earlier. The ladle tracking system showed the unit had completed 847 heats against a design life of 120 heats per campaign, but nobody had correlated campaign count with actual refractory condition because the data lived in three separate systems that didn't communicate. The ladle had been screaming for retirement. The systems designed to protect workers couldn't hear it. Talk to our team about implementing integrated ladle management through CMMS.
This guide provides steelmaking operations managers, ladle yard supervisors, refractory engineers, and maintenance planners with a comprehensive framework for managing ladle maintenance through CMMS-integrated tracking systems. Oxmaint transforms ladle lifecycle data—heat counts, refractory thickness measurements, preheat cycles, slide gate conditions, and shell integrity assessments—into automated maintenance workflows that maximise ladle availability while ensuring absolute safety compliance. We cover ladle types and their maintenance requirements, refractory management strategies, tracking system architecture, preheat optimisation, and the CMMS integration that unifies all ladle data into actionable intelligence. Teams ready to transform ladle management from reactive tracking to predictive optimisation can start their free Oxmaint trial today.
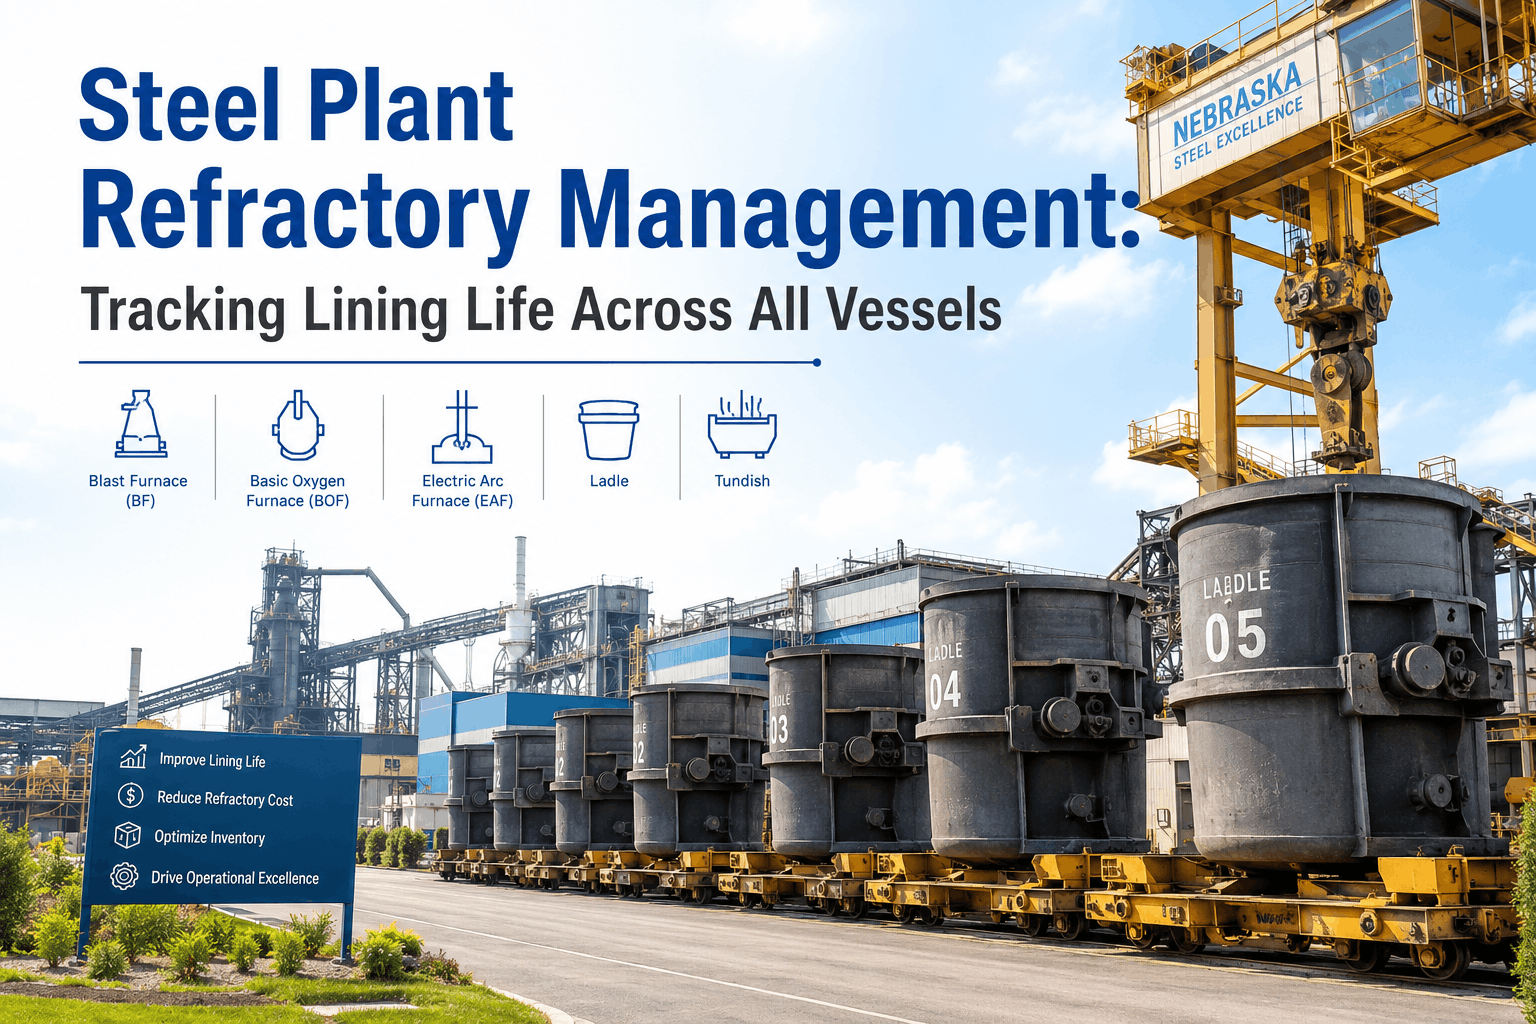
Steel ladles represent one of the largest refractory cost centres in any melt shop—consuming $8-15 million annually in lining materials and labour for a typical 2-3 MTPA operation. Yet most plants manage ladles through paper logs, disconnected spreadsheets, and tribal knowledge that walks out the door with every retirement. The result: premature relining wastes $2-4 million per year in unused lining life, while unexpected failures cause $500K-3M per incident in emergency repairs and lost production.
$12M
Average annual ladle refractory spend for 2.5 MTPA integrated mill
23%
Typical lining life wasted through conservative fixed-campaign relining
4.2 hrs
Average unplanned downtime per ladle failure event
Source: Association for Iron & Steel Technology Ladle Practices Committee 2024
A steel ladle is far more than a refractory-lined vessel—it is a complex system integrating structural shell, multi-layer refractory lining, bottom pour mechanisms (slide gates or stopper rods), gas stirring systems, lifting trunnions, and thermal management requirements. Each subsystem has distinct failure modes, inspection requirements, and maintenance intervals. When these subsystems are managed independently through disconnected systems, critical correlations are missed: the relationship between preheat adequacy and lining life, the impact of steel grade sequences on slag zone wear, the connection between trunnion pin wear and safe working load certification. CMMS integration creates the unified data environment where these correlations become visible and actionable.
Ladle Types and Maintenance Requirements
Steel operations employ multiple ladle types, each with specific design features and maintenance requirements. Understanding these differences is essential for configuring appropriate CMMS maintenance programmes. The primary ladle categories in integrated and EAF-based operations include transfer ladles, treatment ladles, and teeming ladles—though many operations use dual-purpose designs.
Transfer Ladles
Capacity: 100-350 tons
Transport molten steel from BOF/EAF to secondary metallurgy stations. Primary exposure to tap temperatures and initial slag contact.
Key Maintenance Focus:
- Impact zone refractory from tapping stream
- Slag zone erosion from oxidising slag
- Trunnion integrity for crane handling
- Shell stress monitoring during thermal cycling
Typical Campaign: 80-150 heats
Treatment Ladles (LMF/VD/RH)
Capacity: 100-350 tons
Secondary metallurgy operations including desulphurisation, deoxidation, alloying, and inclusion modification. Extended hold times and gas stirring.
Key Maintenance Focus:
- Porous plug condition and flow verification
- Slag line wear from extended treatment
- Freeboard buildup and cleaning
- Bottom refractory from gas stirring erosion
Typical Campaign: 60-120 heats
Teeming Ladles
Capacity: 100-350 tons
Deliver steel to continuous caster or ingot moulds. Critical pour control through slide gate or stopper rod. Longest thermal exposure per heat.
Key Maintenance Focus:
- Slide gate plate wear and alignment
- Nozzle well block condition
- Ladle shroud seating surface
- Bottom pour mechanism reliability
Typical Campaign: 100-180 heats
Many modern operations use dual-purpose ladles that serve both treatment and teeming functions, reducing fleet size but increasing complexity of maintenance requirements. The CMMS must track not just heat count but the specific duty cycle each ladle experiences—treatment time, gas stirring duration, steel grades processed, and slag chemistry exposure—to accurately predict remaining lining life and schedule maintenance appropriately.
Ladle Refractory System Architecture
The ladle refractory system is a multi-layer construction designed to contain molten steel at 1,600°C while protecting the steel shell and minimising heat loss. Each layer serves a specific function and has distinct wear mechanisms, inspection requirements, and replacement intervals. CMMS must track each layer independently to optimise total refractory cost.
Refractory wear varies dramatically by zone—CMMS tracks each independently for optimised maintenance
Slag Zone
Highest Wear
3-8 mm/heat
Chemical attack from slag, thermal cycling, erosion from stirring
Monitor every 5-10 heats; gunning repair as needed
Metal Zone
Moderate Wear
0.5-2 mm/heat
Thermal shock, steel erosion, gas stirring effects
Monitor every 15-25 heats; typically lasts full campaign
Impact Zone
Variable Wear
1-4 mm/heat
Mechanical erosion from tapping stream, thermal shock
Inspect at tap position change; wear pads for protection
Bottom
Lower Wear
0.3-1 mm/heat
Static steel contact, porous plug area erosion
Monitor porous plug; bottom usually outlasts sidewalls
The Ladle Tracking Problem
Effective ladle management requires tracking dozens of parameters across a fleet of 15-40 ladles, each cycling through preheating, service, maintenance, and repair phases. Traditional tracking methods—paper logs, standalone spreadsheets, and siloed databases—create information gaps that lead to both over-maintenance (replacing linings with remaining life) and under-maintenance (failures from undetected wear).
Spreadsheet Tracking
- Data entry errors and omissions
- No real-time visibility
- Multiple conflicting versions
- No automated alerts or triggers
Disconnected Systems
- Heat tracking in Level 2
- Refractory data in separate database
- Maintenance in paper logs
- No correlation between data sources
Tribal Knowledge
- Critical knowledge in heads of veterans
- Inconsistent decisions between shifts
- Knowledge lost with turnover
- No documented decision criteria
The Result:
23% of ladle linings replaced with 15-40% remaining useful life; 8% of failures occur from undetected over-wear; average 4.2 hours unplanned downtime per ladle failure
CMMS-Integrated Ladle Management System
A comprehensive ladle management system built on CMMS infrastructure unifies all ladle data into a single platform where heat history, refractory condition, maintenance records, and operational parameters create a complete picture of each ladle's health. This integration enables predictive lining replacement, optimised maintenance scheduling, and real-time fleet visibility.
CMMS Actions
Automated PM work orders based on heat count
Condition-based reline scheduling from profiler data
Alert generation for out-of-spec conditions
Ladle fleet status dashboard
Refractory consumption forecasting
Compliance documentation for safety certification
01
Heat Count Tracking
Automatic increment from Level 2 integration. Campaign limits by ladle type and grade mix. Automatic work order generation at threshold.
02
Refractory Life Prediction
Zone-specific wear rate trending from laser profiling. Remaining life calculation considering grade-adjusted wear factors. Reline scheduling optimisation.
03
Preheat Management
Preheat cycle tracking and verification. Temperature requirement by next assignment. Alert for inadequate preheat before service.
04
Slide Gate Lifecycle
Pour count per plate set. Wear measurement tracking. Automatic plate change work orders. Supplier performance analytics.
05
Fleet Optimisation
Real-time ladle status visibility. Rotation optimisation for even wear distribution. Capacity planning for production schedules.
06
Safety Compliance
Trunnion inspection scheduling and documentation. Shell integrity certification tracking. Audit-ready compliance reporting.
Refractory Condition Monitoring
The transition from fixed-campaign relining to condition-based relining requires systematic refractory thickness measurement and wear rate analysis. Laser profiling technology enables rapid, accurate measurement of lining thickness across all zones, while CMMS integration converts measurement data into remaining life predictions and optimised reline scheduling.
Fixed Campaign Approach
—
Reline at fixed heat count (e.g., 100 heats)
—
No consideration of actual lining condition
—
Conservative limits waste 15-30% of lining life
—
Aggressive limits risk breakthrough failures
—
No grade mix or treatment time adjustment
Wasted lining life or failure risk
→
CMMS Condition-Based Approach
+
Laser profile every 10-20 heats
+
Zone-specific thickness tracking in CMMS
+
Wear rate adjusted for grade/treatment history
+
Remaining life prediction to minimum safe thickness
+
Reline scheduled at optimal point
Maximum lining utilisation with safety assurance
Slag Zone
180-230 mm
90-100 mm
65-75 mm
Alert at threshold; remove from service at minimum
Metal Zone
150-200 mm
75-85 mm
50-60 mm
Monitor wear rate; flag if accelerating
Impact Zone
200-250 mm
100-120 mm
75-85 mm
Wear pad installation at alert; reline at minimum
Bottom
180-230 mm
85-100 mm
60-70 mm
Usually outlasts sidewall; verify at sidewall reline
Slide Gate Maintenance Management
The slide gate mechanism controlling steel flow from ladle to caster represents a critical safety and quality control point. Gate failure during casting causes sequence breaks, tundish freezing, or uncontrolled steel flow—each with significant cost and safety implications. CMMS tracking of slide gate components ensures reliable operation throughout rated life.
Preheat Optimisation
Ladle preheat adequacy directly impacts refractory life, steel quality, and energy consumption. Insufficient preheat causes thermal shock damage and excessive steel temperature loss; over-preheating wastes energy and can damage refractories. CMMS-integrated preheat management ensures each ladle receives appropriate thermal preparation for its next assignment.
Cold Start (new lining)
1,100-1,200°C
8-16 hours
Staged heating profile; dry-out verification
Cold (ambient start)
1,000-1,100°C
4-8 hours
Block service until threshold reached
Warm (recent service)
900-1,000°C
1-3 hours
Verify temperature before next heat
Hot cycle (continuous use)
Maintain >600°C
N/A
Track cycle time; alert if exceeding limit
Lining Life Extension
+15-25%
Proper preheat reduces thermal shock damage that accelerates wear
Energy Optimisation
-20-30%
Right-sized preheat for ladle condition eliminates over-heating waste
Temperature Control
±5°C
Consistent ladle temperature improves casting superheat control
Case Study: Midwest Steel Ladle Management Transformation
Midwest Steel Corporation operates a 2.1 MTPA BOF-based steel complex with a fleet of 24 ladles serving two BOF vessels, an LMF station, and a two-strand slab caster. Prior to implementing CMMS-integrated ladle management, the operation experienced chronic issues with ladle availability, unpredictable reline scheduling, and two significant safety incidents related to refractory condition.
The Starting Point
67%
Ladle availability—chronic shortage requiring production delays
$14.2M
Annual refractory spend—rising 8% year-over-year
2
Safety incidents from refractory breakthrough in prior 3 years
26%
Lining life variability—same ladle type ranging 68-142 heats
Root Causes Identified
1
Heat tracking in Level 2 not connected to maintenance planning—campaign limits managed manually
2
Laser profiler data stored locally—no integration with reline decision process
3
Fixed campaign limits (95 heats) ignored grade mix and treatment time variations
4
Preheat verification manual—ladles occasionally entered service with inadequate temperature
The Oxmaint Implementation
Months 1-4
Foundation: CMMS ladle asset registry built with complete component hierarchy. Level 2 integration established for automatic heat count tracking. Historical profiler data imported to establish wear rate baselines.
Months 5-9
Active Monitoring: Real-time profiler integration deployed. Zone-specific wear rate algorithms calibrated. Automatic work order generation activated for inspection and reline scheduling. Preheat verification gates implemented.
Months 10-18
Optimisation: Remaining life prediction refined with machine learning. Grade-adjusted wear factors implemented. Fleet rotation optimisation activated. Refractory supplier performance analytics deployed.
89%
Ladle Availability
Up from 67%—eliminated production delays from ladle shortage
$3.4M
Annual Refractory Savings
24% reduction through optimised campaign length
0
Safety Incidents
Zero refractory-related safety events since implementation
118 avg
Campaign Length
Up from 95 fixed—with improved safety margin
6.2 mo
Payback Period
Full system investment recovered from refractory savings
100%
Preheat Compliance
No ladle enters service without verified temperature
Implementation Roadmap
Implementing CMMS-integrated ladle management follows a phased approach that builds capability systematically while delivering value at each stage. The roadmap below outlines a typical 12-18 month implementation for a steel plant transitioning from manual or fragmented ladle tracking.
Phase 1
Months 1-4
Foundation
Ladle fleet inventory and asset registry
Component hierarchy definition
Historical data migration
Level 2 integration for heat tracking
Basic campaign limit work orders
Deliverable: All ladles tracked in CMMS with automatic heat count updates
Phase 2
Months 5-9
Condition Monitoring
Laser profiler CMMS integration
Zone-specific wear tracking
Preheat monitoring integration
Slide gate lifecycle tracking
Condition-based work order triggers
Deliverable: Reline decisions based on actual condition data, not fixed intervals
Phase 3
Months 10-14
Optimisation
Remaining life prediction algorithms
Grade-adjusted wear factors
Fleet rotation optimisation
Refractory consumption forecasting
Supplier performance analytics
Deliverable: Predictive reline scheduling optimised for cost and availability
Phase 4
Months 15+
Excellence
Machine learning wear prediction
Digital twin ladle modelling
Automated reline scheduling
Continuous improvement analytics
Cross-site best practice sharing
Deliverable: World-class ladle management with minimal manual intervention
Financial Impact Summary
The financial case for CMMS-integrated ladle management is built on refractory cost reduction, improved ladle availability, and safety incident prevention. A typical 2-3 MTPA operation with 20-30 ladles realises $2-5 million in annual savings from optimised lining life alone, with additional value from production gains and risk reduction.
Without CMMS Management
Refractory consumption (conservative campaigns)
$12,800,000
Production delays from ladle shortage
$2,400,000
Emergency relines (unplanned failures)
$1,200,000
Safety incident risk exposure
$2,000,000
Annual Exposure: $18,400,000
With Oxmaint Ladle Management
CMMS platform and integration
$95,000
Profiler integration and sensors
$180,000
Implementation and training
$120,000
Optimised refractory consumption
$9,700,000
Annual Cost: $10,095,000
Annual Savings:
$8,305,000
Payback Period:
4-7 Months
Transform Your Ladle Fleet Into a Predictable, Optimised Asset
Oxmaint CMMS integrates with Level 2 systems, laser profilers, preheat monitors, and inspection workflows to create a unified ladle management platform. Maximise refractory life, ensure safety compliance, and eliminate production delays from ladle shortage.
Frequently Asked Questions
What data sources need to integrate with CMMS for effective ladle management?
A comprehensive ladle management system requires integration with multiple data sources. Level 2 production system provides heat identification, steel grade, tap time, treatment duration, and casting time—enabling automatic heat count tracking and grade-adjusted wear factors. Laser profiler systems provide refractory thickness measurements by zone after each measurement cycle, enabling remaining life calculation. Preheat station monitoring provides temperature data and heating duration for preheat verification. Shell thermocouple systems provide real-time temperature data for hot spot detection. Manual inspection inputs capture visual condition assessments, slide gate measurements, and safety observations. Oxmaint provides standard integrations for major Level 2 systems (ABB, Primetals, SMS) and laser profiling systems (Ferrotron, Minteq, RHI Magnesita), with open APIs for custom integrations.
Sign up free to discuss integration requirements for your specific systems.
How does condition-based relining actually work compared to fixed campaigns?
Fixed campaign relining schedules relines at a predetermined heat count (e.g., 100 heats) regardless of actual lining condition. This approach is either conservative (wasting 15-30% of remaining lining life) or aggressive (risking failure). Condition-based relining uses laser profiling to measure actual refractory thickness by zone every 10-20 heats. The CMMS calculates wear rate by zone, adjusting for grade mix and treatment history, and predicts when each zone will reach minimum safe thickness. Reline is scheduled when the fastest-wearing zone approaches minimum threshold—not before (wasting life) and not after (risking failure). The system accounts for reline lead time, scheduling the ladle for reline 10-15 heats before predicted end-of-life to ensure availability of reline resources. This approach typically extends average campaign length 15-25% while actually improving safety margins because decisions are based on measured condition rather than assumptions.
What is the typical ROI and payback period for ladle management systems?
Steel plants implementing CMMS-integrated ladle management typically achieve payback within 4-8 months, with annual savings of $2-5 million depending on fleet size and current practices. The primary value drivers are: refractory cost reduction (20-30% savings through optimised campaign length)—typically $2-4M annually for a 2.5 MTPA operation; production improvement from better ladle availability—typically $500K-1.5M from eliminated delays; emergency reline reduction—typically $200-500K from prevented unplanned failures; and safety risk reduction—difficult to quantify but significant given $10-100M+ exposure per breakthrough incident. Implementation costs range from $300-600K including CMMS platform, integrations, sensors, and training. Most plants report the system "pays for itself" from the first prevented failure or first optimised reline campaign that would have been scheduled early under the old system.
How does the system handle different ladle types and steel grade requirements?
The CMMS maintains distinct asset profiles for each ladle type (transfer, treatment, teeming, or dual-purpose) with specific maintenance requirements, component hierarchies, and wear factor calibrations. Steel grade processing history is tracked per ladle, with wear rate adjustments based on slag chemistry—high-manganese grades, calcium-treated heats, and other aggressive chemistries apply multipliers to base wear rates. The system can enforce grade restrictions when a ladle approaches end-of-campaign (limiting to less aggressive grades to extend life) or when specific grades require ladle preparation (higher preheat, freeboard cleaning). This grade-aware tracking ensures accurate remaining life prediction even when ladles process varied product mixes, and enables grade-sequencing optimisation to maximise campaign length.
Book a demo to see grade-aware ladle management in action.
What safety certifications and compliance documentation does the system support?
Ladle safety requires documented compliance with multiple requirements. Trunnion inspection and certification (typically annual or per campaign) is tracked with inspection scheduling, results documentation, and certification expiration alerts. Refractory thickness documentation provides auditable records of all measurements with zone-specific trending for safety review. Shell integrity assessment tracking includes ultrasonic thickness testing results and hot spot monitoring history. Operating limit enforcement prevents service of ladles exceeding maximum heat count or below minimum refractory thickness. All inspection and maintenance records are timestamped with technician identification and stored for regulatory compliance. The system generates audit-ready reports for safety reviews showing complete maintenance history, inspection results, and certification status for each ladle. This documentation has proven valuable during incident investigations (demonstrating due diligence) and insurance audits (supporting coverage positions).