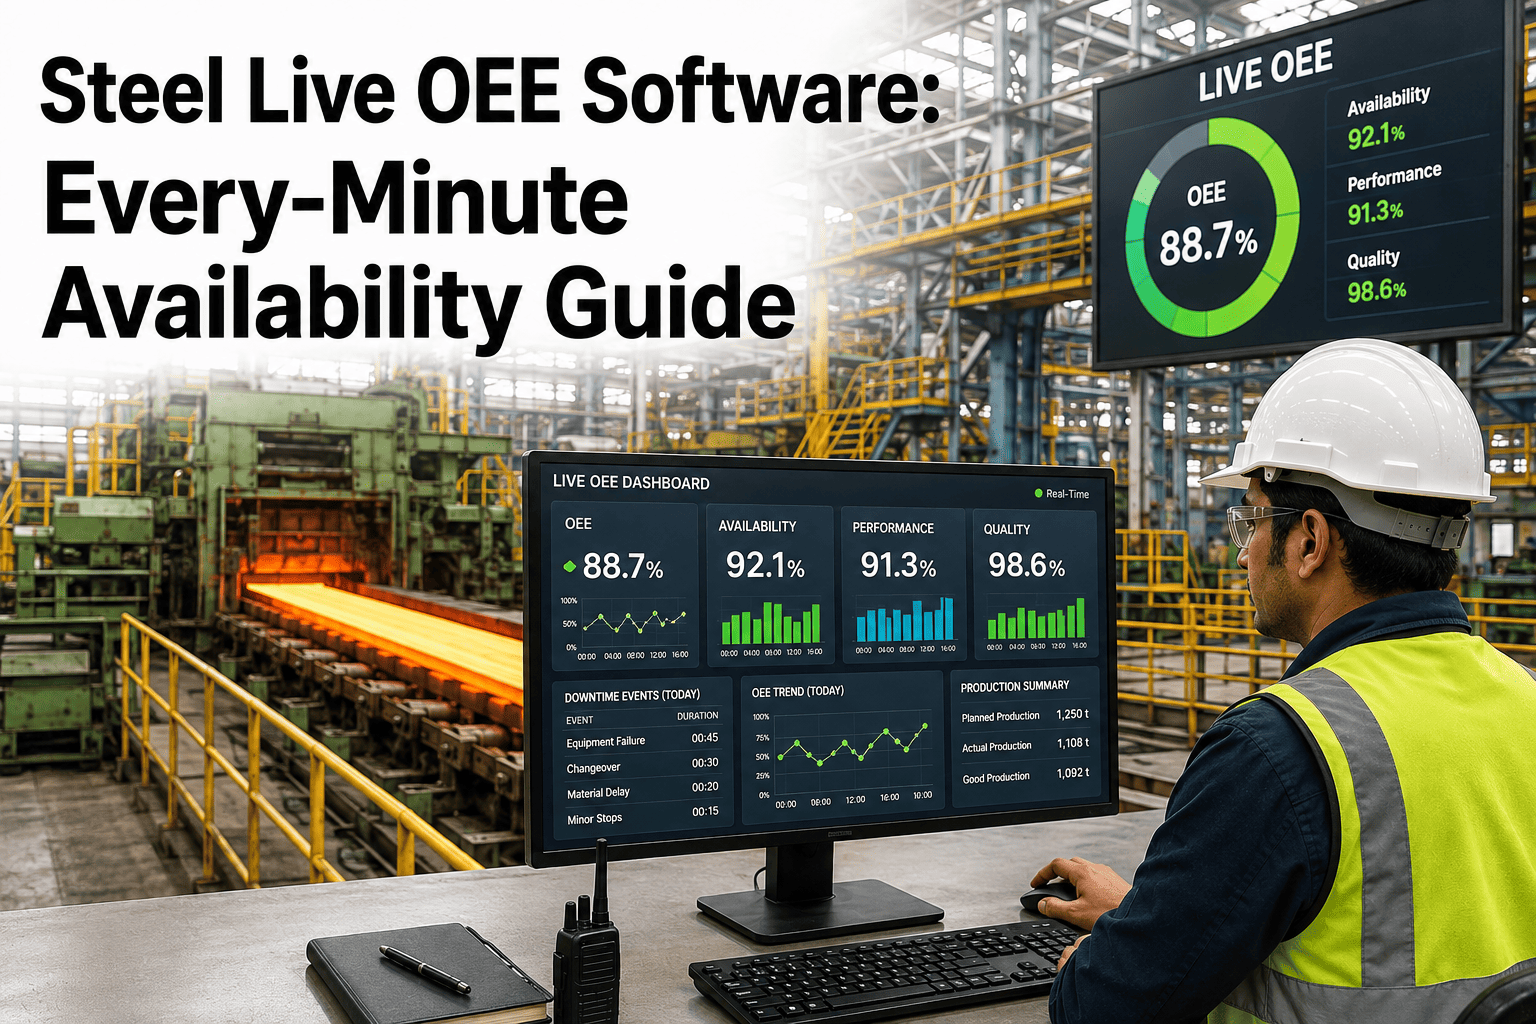
Walk onto almost any steel plant floor and ask the shift supervisor for last week's downtime report, and the number that comes back will look reasonable — maybe 78% availability, in line with what the plant has always reported. Now install automated monitoring for a single week and count every interruption, including the 40-second jam at the coiler and the 90-second sensor fault at the shear, and the real number is often twelve percentage points lower. Those sub-3-minute stops never make it onto a clipboard because nobody can write down "10:42, jam, cleared" fast enough to matter, and by the time a supervisor walks over, the line is already running again. Multiply a 45-second stop by 80 occurrences in a shift and it adds up to an hour of production that exists nowhere in any report. Oxmaint's micro-stop detection module connects directly to your PLCs and sensors so every one of those short stops gets captured, classified, and turned into a fixable pattern instead of a rounding error.
The Stops Too Short To Log Are The Ones Costing You The Most
Sub-3-minute jams, sensor faults, and minor interventions never reach a downtime report — but they are usually the single largest source of hidden OEE loss on a steel line.
What Manual Downtime Logs Actually Miss
A line that looks like it is running fine on paper can be losing a fifth of its available capacity to stops nobody wrote down.
Manual logs capture major breakdowns only. Sub-3-minute stops are cleared and forgotten before anyone can record them.
Every micro-stop is captured automatically, ranked by impact, and traced to a mechanical root cause that gets fixed.
Why A 45-Second Stop Is Not A Small Problem
A single 45-second jam feels irrelevant on its own — clear it, restart, move on. The problem is frequency, not duration. Steel lines running at speed can see the same jam signature dozens of times in a single shift, and none of it shows up until someone adds it up.
Average length of a typical feed jam or sensor fault
Times it repeats across a single 8-hour shift
Of production lost — invisible in a manual report
Big Stops Get The Attention. Micro-Stops Get The Capacity.
When a motor fails for four hours, the whole plant reacts. When forty jams cost four hours across a month, almost nobody notices — until the total is added up.
Major Breakdowns
Rare, dramatic, and fully logged — maintenance responds immediately and a root cause analysis is filed the same day.
Fully VisibleSub-3-Minute Micro-Stops
Frequent, brief, and cleared by the operator before anyone can log the event — the largest source of hidden Performance loss on the line.
Mostly InvisibleSpeed Loss
The line runs, but below its ideal cycle time — disguised as normal operation rather than counted as a loss.
Mostly InvisibleStop Losing Capacity To Stops You Never See
Connect your PLCs and sensors to Oxmaint and capture every sub-3-minute stop automatically, from first shift onward.
From Invisible Stop To Fixed Root Cause
Connect The Line
Oxmaint reads cycle counts and machine state directly from your PLCs and sensors via OPC-UA, MQTT, or Modbus — no manual logging step required.
Capture Every Stop, Down To Seconds
Any interruption under the 3-minute threshold is logged automatically with timestamp, duration, and asset — including the ones that clear themselves in under a minute.
Rank By Total Time Impact
Events are grouped by signature and sorted by cumulative time lost over a rolling window, so a jam that repeats 80 times a shift outranks a one-off five-minute stop.
Generate A Targeted Work Order
The top pattern — a worn guide rail, a misaligned sensor, a loose chute liner — gets a work order pointed at the mechanical cause, not a generic reminder to "check the line."
What A Ranked Micro-Stop Report Actually Looks Like
| Stop Signature | Frequency Per Shift | Avg Duration | Total Time Lost |
|---|---|---|---|
| Feed Guide Jam | 80 | 45 sec | 60 min |
| Photo-Eye Sensor Fault | 35 | 30 sec | 18 min |
| Coil Threading Delay | 12 | 90 sec | 18 min |
| Chute Liner Blockage | 9 | 2 min | 18 min |
| Minor Alignment Stop | 6 | 150 sec | 15 min |
Swipe horizontally on mobile to see the full table.
Built To Catch What A Manual Log Cannot
Second-Level Capture
Machine state changes are logged automatically down to one-second resolution, so a 20-second stop is recorded exactly as reliably as a two-hour one.
Automatic Pattern Grouping
Recurring stop signatures are grouped by asset and cause automatically, turning a wall of individual events into a short, actionable Pareto list.
Zero Manual Logging
Operators never touch a screen to record a stop — the system captures it whether or not anyone on shift even notices the interruption happened.
Root-Cause Work Orders
The top-ranked pattern generates a work order pointed at the specific mechanical fix, tracked through to close and verified against the next shift's cycle data.
A steel mill that tracked only stoppages over ten minutes reported a comfortable 78% availability for a full year. Once automated monitoring captured every interruption down to thirty seconds, those "minor" stoppages turned out to be consuming twelve percent of total production time that had never appeared in any report.
Frequently Asked Questions
Find The OEE Points Hiding In Your Micro-Stops
Connect your line to Oxmaint and see your first hidden-loss report within days, not months.