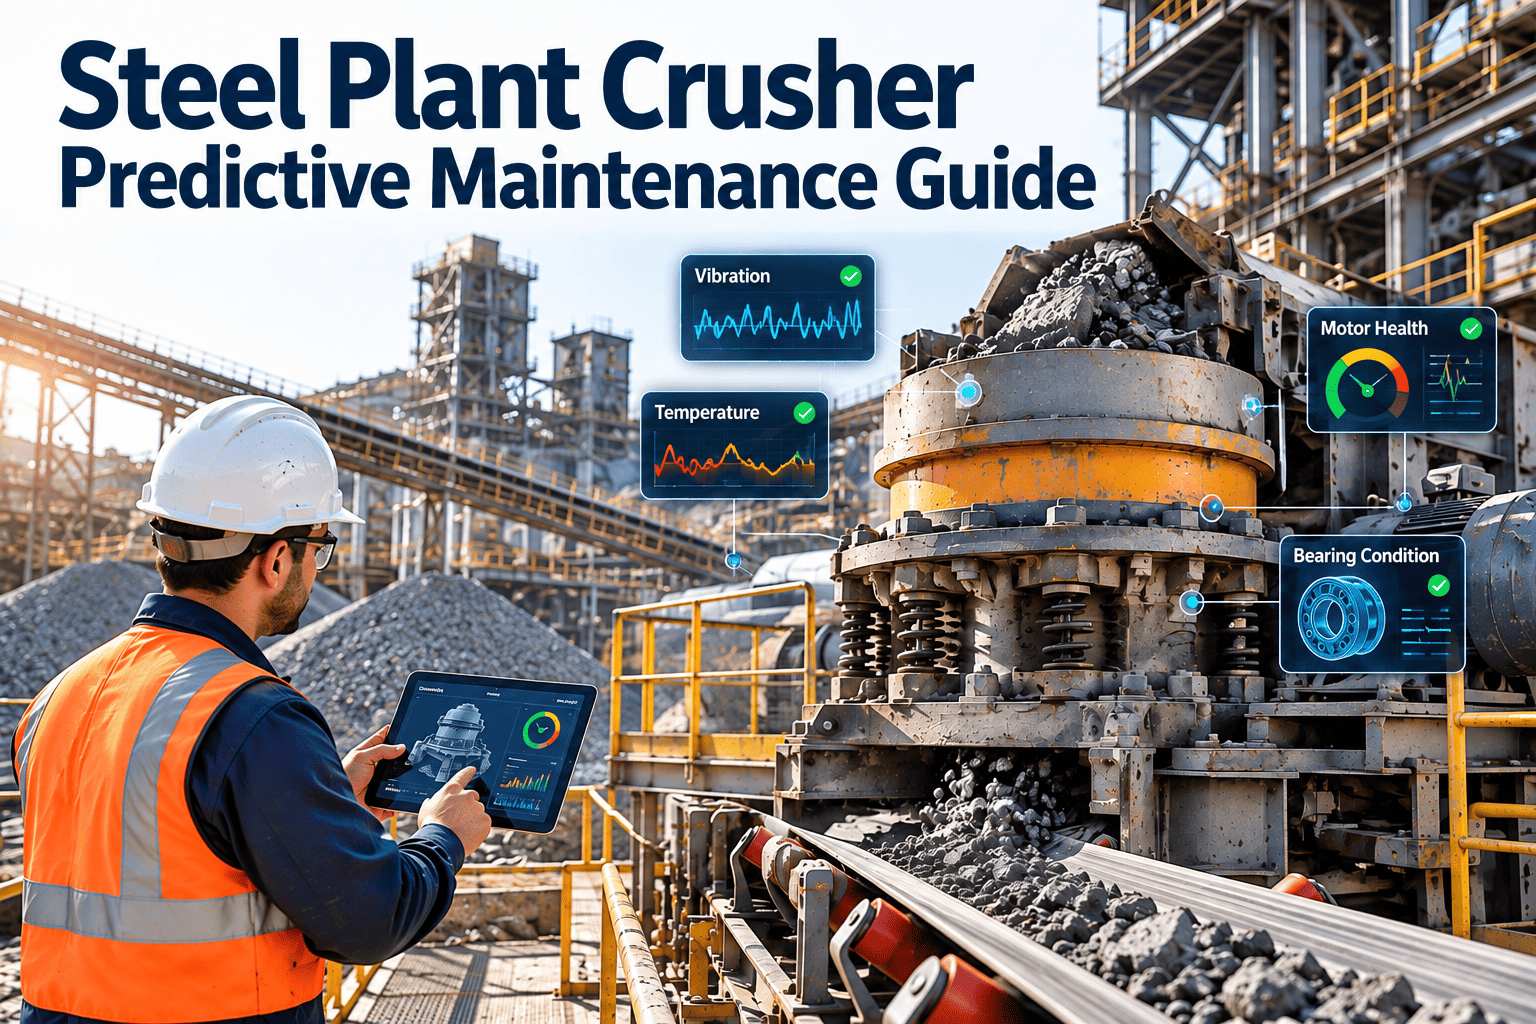
Crushers sit at the front of the steel plant material chain. Coke, limestone, dolomite, coal and ore lumps are reduced here before they reach screens, sinter strands and furnace bunkers. When a crusher stops, the stockyard keeps delivering and the plant behind it starts to run down its buffers. Bearing damage, gearbox wear, motor overload and liner erosion give measurable warning long before a stoppage, and this guide shows how to use it with Oxmaint maintenance software.
Steel plant crusher predictive maintenance
Predict bearing, gearbox, motor, liner and vibration problems on raw material crushers, and plan the repair before feed to sinter and furnace is interrupted.
Where crushers are used and why failures spread
Steel plants use several crusher types across raw material handling. Each has different wear parts and different early warnings.
Hammer and impact crushers
Common for coke, coal and limestone. Hammers, blow bars, breaker plates and rotor bearings wear quickly and unevenly.
Jaw crushers
Used for hard lumps and oversize. Jaw plates, toggle plates, pitman bearings and flywheels need close attention.
Roll crushers
Often used for coke and sinter breaking. Roll shell wear, gap setting and drive gearboxes drive most of the maintenance.
Sinter cooler and hot sinter crushers
Run in hot, abrasive conditions. Heat stress and dust add to bearing and seal problems.
A crusher failure also stresses neighbours. Feeders back up, belts stop under load and stacker reclaimers wait, so one fault can create several jobs.
The failure chain: how crusher problems build
Most crusher stoppages follow a chain. Breaking the chain early is cheaper than repairing the end result.
Wear or contamination starts
Liners thin, grease breaks down and dust enters seals. Nothing looks wrong on the control screen.
Signals shift
Vibration, bearing temperature and motor current move away from baseline at the same feed rate.
Damage spreads
A worn bearing raises rotor deflection. Loose liners strike the frame. Gear teeth pit under uneven load.
Trip or breakdown
Overcurrent, high vibration or a mechanical failure stops the crusher during production.
Crusher components and the evidence each one gives
Use this table to decide what to measure on each part. Not every crusher needs every measurement.
Vibration and bearing monitoring on shock-loaded machines
Crushers create high vibration by design, so limits copied from smooth-running fans will trigger constant alarms.
Set useful baselines
- Measure at the same feed rate and material type each time
- Record separate baselines for hard and soft feed
- Use trend change relative to the machine, not a general standard alone
- Compare the same bearing position across sister crushers
Watch for these changes
- Rising high-frequency energy at bearing positions
- Growing 1x vibration from rotor imbalance after hammer loss
- New harmonics that suggest looseness or foundation cracking
- Bearing temperature rising while load stays the same
Rotor balance deserves special mention. Uneven hammer or blow bar wear changes balance long before the bearings fail, so vibration trends can also guide when to change a full set.
Bring crusher condition and maintenance history together
Register each crusher, set baseline limits and let Oxmaint create inspection and repair jobs when readings drift.
Liner and wear part life: from new to change-out
Liners are consumables, but the timing of their replacement is a decision that affects product size, throughput and the risk to the frame.
- Measure wear at fixed points, with photographs, at each planned stop.
- Convert measurements to wear rate per tonne crushed, not only per calendar month.
- Use the wear rate to forecast the change date and order parts in time.
- Record supplier, alloy and mounting method so different liner sets can be compared honestly.
Tramp metal, oversize and blockages
Many sudden failures are triggered by something that should not have been in the feed.
Causes to control
- Tramp iron from upstream equipment or scrap contamination
- Oversize lumps from a damaged grizzly or screen
- Wet or sticky feed that blocks chutes
- Uneven feeding that overloads one side of the rotor
Preventive checks
- Magnet and metal detector function tests
- Grizzly and screen deck inspection
- Chute wear plate and level sensor inspection
- Emergency stop and interlock testing
Reactive crusher upkeep versus a condition-based routine
Reactive
- Bearings changed after seizure
- Liners changed when noise becomes severe
- Spare parts ordered after failure
- Oil and grease done when someone remembers
Condition-based
- Bearings changed from trend and temperature
- Liners planned from measured wear rate
- Spares reserved from forecast dates
- Lubrication tasks scheduled and recorded on the asset
Daily and weekly crusher inspection checklist
Every shift
- Listen for new knocks or rubbing
- Check motor current against the usual band
- Look for leaks at bearings and gearbox
- Confirm dust suppression is working
Weekly
- Take vibration and temperature readings
- Check grease points and oil level
- Inspect visible liners and fasteners
- Review feeder and chute condition
At planned stops
- Measure wear parts and photograph them
- Inspect rotor, shaft and frame for cracks
- Check coupling alignment
- Test protection devices and interlocks
Managing dust, safety and environmental records
Crushing releases dust and noise, and repair work involves heavy lifting and confined access. The maintenance record supports both safety and compliance.
- Log dust collector and suppression checks with the crusher record, since a failing collector often accompanies heavy dust deposits on bearings.
- Store isolation, lockout and confined space permit references on each work order.
- Keep lifting equipment inspections and rigging plans for liner changes attached to the job.
- Record noise and guarding checks where site rules require them.
- Use consistent job plans so contractors and internal crews follow the same steps.
Gearbox and lubrication: reading the oil
Crusher gearboxes carry high torque and shock loads. Oil condition is often the earliest reliable sign of trouble.
Sample and test
- Viscosity and water content
- Particle count and wear metals
- Sampling from the same point each time
Watch on site
- Sump temperature at steady load
- Breather condition and seal leaks
- Magnetic plug debris
Act on findings
- Change or filter oil on condition
- Investigate rising wear metals early
- Correct misalignment before overhaul
Store each result against the gearbox, so a rising trend is visible across several samples and several years, not in isolation.
Motor and electrical health on crusher drives
A crusher motor works hard. Starts under load, feed surges and dust all shorten winding and bearing life.
- Trend running current against feed rate. A rising current at the same feed points to friction, worn liners or blocked flow.
- Record winding and bearing temperatures at steady load, and compare with the motor's own history.
- Check starter, soft starter or drive alarms as part of every weekly review.
- Keep vents and fan covers clear, since dust build-up is a frequent cause of overheating.
- Inspect terminal boxes and cable entries for heat marks and loose connections.
Spare parts strategy for crushers
A predictive warning has little value if the part is not available. Match stock to lead time and consequence.
Common crusher maintenance mistakes
Changing liners by calendar only
Wear depends on material hardness and tonnage, so a fixed date wastes life or risks the frame.
Overgreasing bearings
Too much grease raises temperature and damages seals. Record quantity as well as date.
Ignoring feed conditions
A crusher fed unevenly or with wet material will wear faster, however well it is maintained.
Skipping the post-repair check
Bolt torque, alignment and clearances should be verified and recorded before the crusher returns to service.
A phased rollout for a raw materials area
Technology that supports crusher condition monitoring
Plants can start with simple tools and add technology where the return is clear.
Simple and low cost
- Handheld vibration and temperature readings on a fixed route
- Thermal imaging of bearings, motors and electrical connections
- Ultrasonic tools for lubrication and early bearing noise
- Photographic wear records at each stop
Continuous and connected
- Fixed vibration and temperature sensors on critical bearings
- Motor current and power taken from the drive or starter
- Laser or scanner wear profiling on selected crushers
- Data fed to the maintenance system to raise jobs on limits
Whatever the tool, the discipline is the same: a defined baseline, an owner for each alarm and a closed record of what was found.
Coordinating with stockyard, screening and sinter operations
Crusher maintenance is easier to schedule when it is planned together with the equipment around it.
- Share condition warnings with the raw material planner so stockpiles and bunker levels can cover a planned stop.
- Align crusher outages with belt, screen and stacker reclaimer work, so one shutdown serves several jobs.
- Agree which crushers can back each other up and keep those standby units in serviceable condition.
- Review the effect of crushed product size on sinter mix quality, and tell maintenance when liner wear starts to change it.
- Include crusher condition in the daily production meeting, with one line on the top open warning and its planned date.
- Keep a shared calendar of planned stops so contractors, operators and stores staff prepare in the same week.
- Use the maintenance record to show operations how many hours were lost to each cause, and what planned work avoided.
Operational symptoms that point to a maintenance cause
Operators often see the first sign. A short guide helps them record it in a useful way.
Indicators that show whether the programme is working
How Oxmaint fits the crusher maintenance workflow
Plan
- Asset records for each crusher, feeder, gearbox and motor
- Preventive tasks for lubrication, inspection and testing
- Measurement templates for liner thickness and rotor clearance
- Scheduled outages linked to production plans
Execute and learn
- Mobile work orders with photos, readings and sign-off
- Inventory for hammers, liners, bearings and seals
- Corrective jobs raised from out-of-limit readings
- Reports on repeat failures, cost and downtime by crusher
Frequently asked questions
What should we monitor first on a steel plant crusher?
Start with bearing temperature, vibration and motor current, then add wear measurements for liners and hammers.
How do we set vibration limits on a machine that shakes?
Use trends against your own baseline at a steady feed rate. You can record baselines in Oxmaint for each crusher.
Can liner replacement be predicted?
Yes, if wear is measured at fixed points and tied to tonnes crushed, the change date becomes a forecast.
Does this apply to stacker reclaimers and feeders too?
The same approach applies to their drives and gearboxes, with limits adjusted to their duty.
How do we see it for our plant?
Please book a short demo and we will walk through a crusher asset set-up.
Keep raw material moving with planned crusher maintenance
Track wear, trend condition and plan repairs around production. Build your crusher programme in Oxmaint or review it with our team.