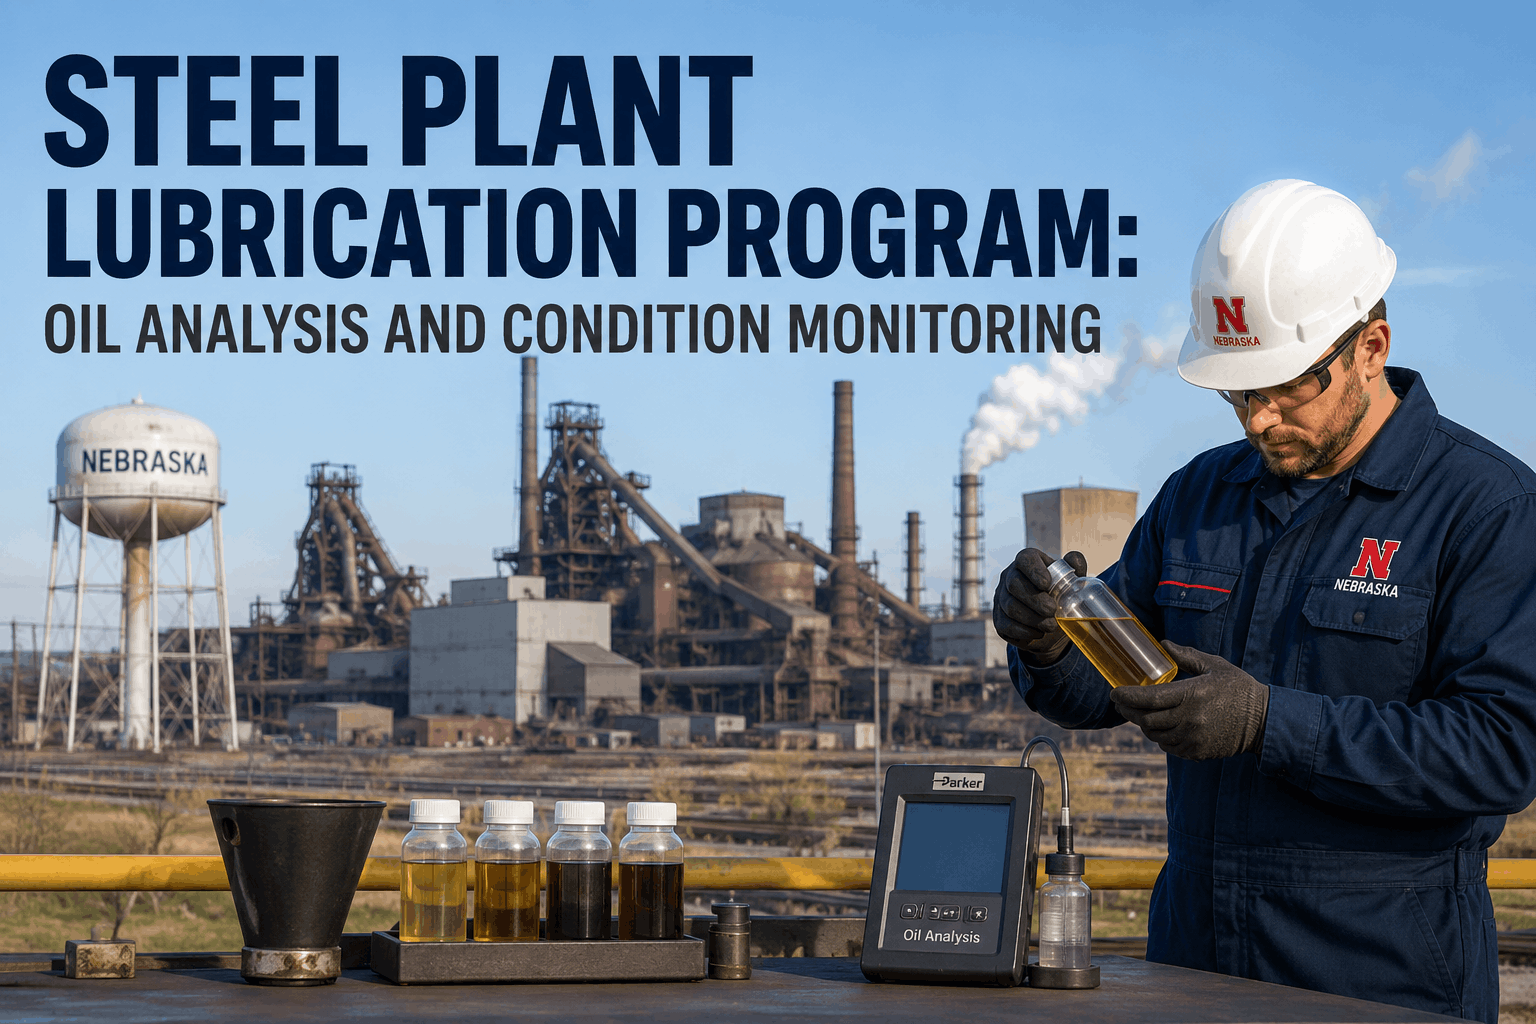
Most steel plants already take oil samples, yet many still learn about a failing gearbox from noise or heat instead of from the lab report. The gap is rarely the laboratory. It is the program around it: unclear sample points, irregular schedules, results that sit in email and alerts that no one owns. A working oil analysis program links every sample to an asset, a limit and an action, and maintenance management software for steel plants keeps that chain unbroken from bottle to work order.
Steel Plant Oil Analysis Program for Gearboxes, Hydraulics and Critical Machinery
Build a sample schedule, set trend-based alert limits and turn lab results into planned maintenance, so oil condition drives decisions before wear turns into downtime.
Why Steel Plants Need More Than Routine Sampling
Steel production punishes lubricants. Heat, scale, water, dust and shock loads all reach the oil, and the machines are expensive to stop.
Sampling without a program
- Samples taken when someone remembers
- Different ports and methods each time
- Reports filed but not trended
- Oil changed by calendar, not condition
- Alarms noticed after the next breakdown
Sampling inside a program
- Schedule set by asset criticality
- Fixed sample points and one procedure
- Results trended against a baseline
- Oil changes and filtration based on condition
- Alerts create owned work orders
What the Oil Is Telling You
Each test answers a different question. Choose the panel by machine type and failure risk, not by habit.
| Test | What It Shows | Typical Finding |
|---|---|---|
| Elemental spectroscopy | Wear metals, additives and contaminants | Rising iron or copper points to gear or bearing wear |
| Particle count | Cleanliness level of the fluid | High counts shorten pump and valve life in hydraulics |
| Water content | Moisture from leaks, condensation or cooling | Water cuts film strength and drives corrosion |
| Viscosity | Oil thickening or thinning | Shift suggests oxidation, mixing or fuel and solvent entry |
| Acid number and oxidation | Oil ageing and additive depletion | Guides oil change timing |
| Ferrography or patch test | Size and shape of wear debris | Confirms severe wear modes before failure |
Program Readiness Checklist
Settle these items before the first bottle is filled. Most failed programs skipped at least half of them.
- List every gearbox, hydraulic unit, circulating system and bearing system in scope, with location and criticality ranking.
- Record oil type, grade, sump volume and filter details for each asset from nameplates and manuals.
- Keep a new-oil sample for each lubricant to serve as the baseline for later comparison.
- Define target cleanliness and contamination limits per component, using manufacturer guidance as the starting point.
- Fit proper sample ports or valves where only drain plugs exist, and label each port clearly.
- Choose a laboratory and agree on test panels, turnaround time and the format of results.
- Assign one owner for sampling, one for reviewing results and one for closing resulting actions.
- Train samplers on the procedure and confirm they have clean bottles, tubing and labels.
Sampling Procedure Checklist
A bad sample is worse than none, because it produces confident but wrong conclusions.
- Sample while the machine is running or immediately after shutdown, when oil is warm and wear particles are still suspended.
- Use the same port, same method and similar operating conditions every time so trends are comparable.
- Flush the port and line before collecting, and discard the flush volume away from the sample area.
- Use clean, sealed bottles suited to the test, and never reuse bottles or wipe the inside.
- Avoid sampling from drain plugs, sump bottoms or stagnant dead legs where sludge distorts results.
- Label each bottle with asset tag, date, hours since oil change and any top-ups made.
- Note abnormal conditions such as leaks, recent maintenance or unusual load, and send them with the sample.
- Record the sample in the maintenance system the same day so the result can attach to the asset.
Sample Schedule by Machine Type
Start with these intervals, then tighten them for critical assets or shorten them after an abnormal result.
| Machine Group | Suggested Starting Interval | Key Tests | Main Risk |
|---|---|---|---|
| Rolling mill gearboxes | Monthly | Wear metals, water, viscosity | Gear and bearing wear, water ingress |
| Hydraulic systems for mill and caster | Monthly | Particle count, water, oxidation | Valve sticking, pump wear |
| Crane and ladle handling gearboxes | Quarterly | Wear metals, viscosity | Shock load wear, heat |
| Fan and blower gearboxes | Quarterly | Wear metals, water | Bearing damage, dust entry |
| Circulating oil systems | Monthly | Particles, water, acid number | Filter loading, oxidation |
| Lower criticality drives | Twice a year | Basic wear and viscosity | Gradual wear |
Intervals are starting points. Set final frequencies from machine criticality, operating hours, environment and supplier guidance.
Schedule Every Sample Before It Is Missed
Create recurring sample tasks per asset, record who collected them and see overdue samples at a glance.
Gearbox Oil Monitoring Checklist
- Check sump level, breather condition and seals at every round, and log any top-up volume.
- Review iron, copper and other wear metal trends together rather than one reading at a time.
- Compare water content with previous samples, and inspect cooler tubes and seals when it rises.
- Watch viscosity for drift from the baseline, which may signal mixing, oxidation or contamination.
- Look for particle size shifts that suggest a change from normal wear to severe wear.
- Correlate oil results with vibration and temperature readings before deciding on action.
Hydraulic Oil Analysis Checklist
- Compare particle counts with the target cleanliness code for the most sensitive component in the circuit.
- Confirm filter condition, differential pressure indicators and bypass status at each sampling round.
- Check water and air entrainment, especially after leaks, reservoir work or seal replacement.
- Review acid number and oxidation to plan fluid change before varnish forms on valves.
- Inspect fill points, breathers and reservoir caps for dirt entry paths and replace damaged parts.
- Record every top-up and filter change so results can be interpreted correctly.
Trend-Based Alert Levels
Fixed limits catch gross failure. Trends catch the slow change that gives you time to plan.
Set numeric limits for each asset from manufacturer data, lab guidance and your own baseline history.
Linking Lab Results to Maintenance Actions
| Result | Likely Cause | Maintenance Response |
|---|---|---|
| High water content | Failed seal, cooler leak, condensation | Inspect seals and coolers, dry or replace oil |
| Rising wear metals | Gear or bearing wear | Add vibration check, plan inspection window |
| High particle count | Poor filtration, dirty top-ups | Replace filter, flush system, review fill practice |
| Viscosity out of range | Oxidation, mixing, contamination | Confirm lubricant, plan oil change |
| High acid number | Oil ageing, overheating | Check temperature, schedule fluid change |
Running the Program in Oxmaint
The program fails when data stays in separate files. Keep the whole loop in one maintenance system.
Inventory tracking also helps keep the right lubricants, filters and breathers in stock.
Metrics That Show the Program Is Working
Mistakes That Weaken an Oil Analysis Program
- Changing sample points or methods, which breaks trend comparison.
- Skipping new-oil baselines, which leaves nothing to compare against.
- Reading single results without checking vibration, temperature and operating history.
- Letting reports pile up without a named reviewer.
- Topping up with the wrong oil or from unclean containers.
Oil Analysis Program FAQs
How often should steel plant gearboxes be sampled?
Critical mill gearboxes are often sampled monthly, others quarterly. Adjust by criticality, operating hours and recent results.
Which tests matter most for hydraulic oil?
Particle count, water content and oxidation matter most, since they drive valve and pump wear.
What is the best way to set alert limits?
Start from manufacturer guidance and lab data, then refine with your own trends. Track limits per asset in one place.
Can oil analysis replace vibration monitoring?
No. They complement each other, and using both gives stronger confirmation of wear before you commit to a stop.
How does Oxmaint support oil analysis programs?
It schedules samples, logs results, trends readings and raises work orders. Book a demo to see the setup.
Turn Oil Reports Into Planned Maintenance
Put sample schedules, trend limits and corrective actions in one system, and let oil condition guide your next maintenance decision across gearboxes and hydraulics.