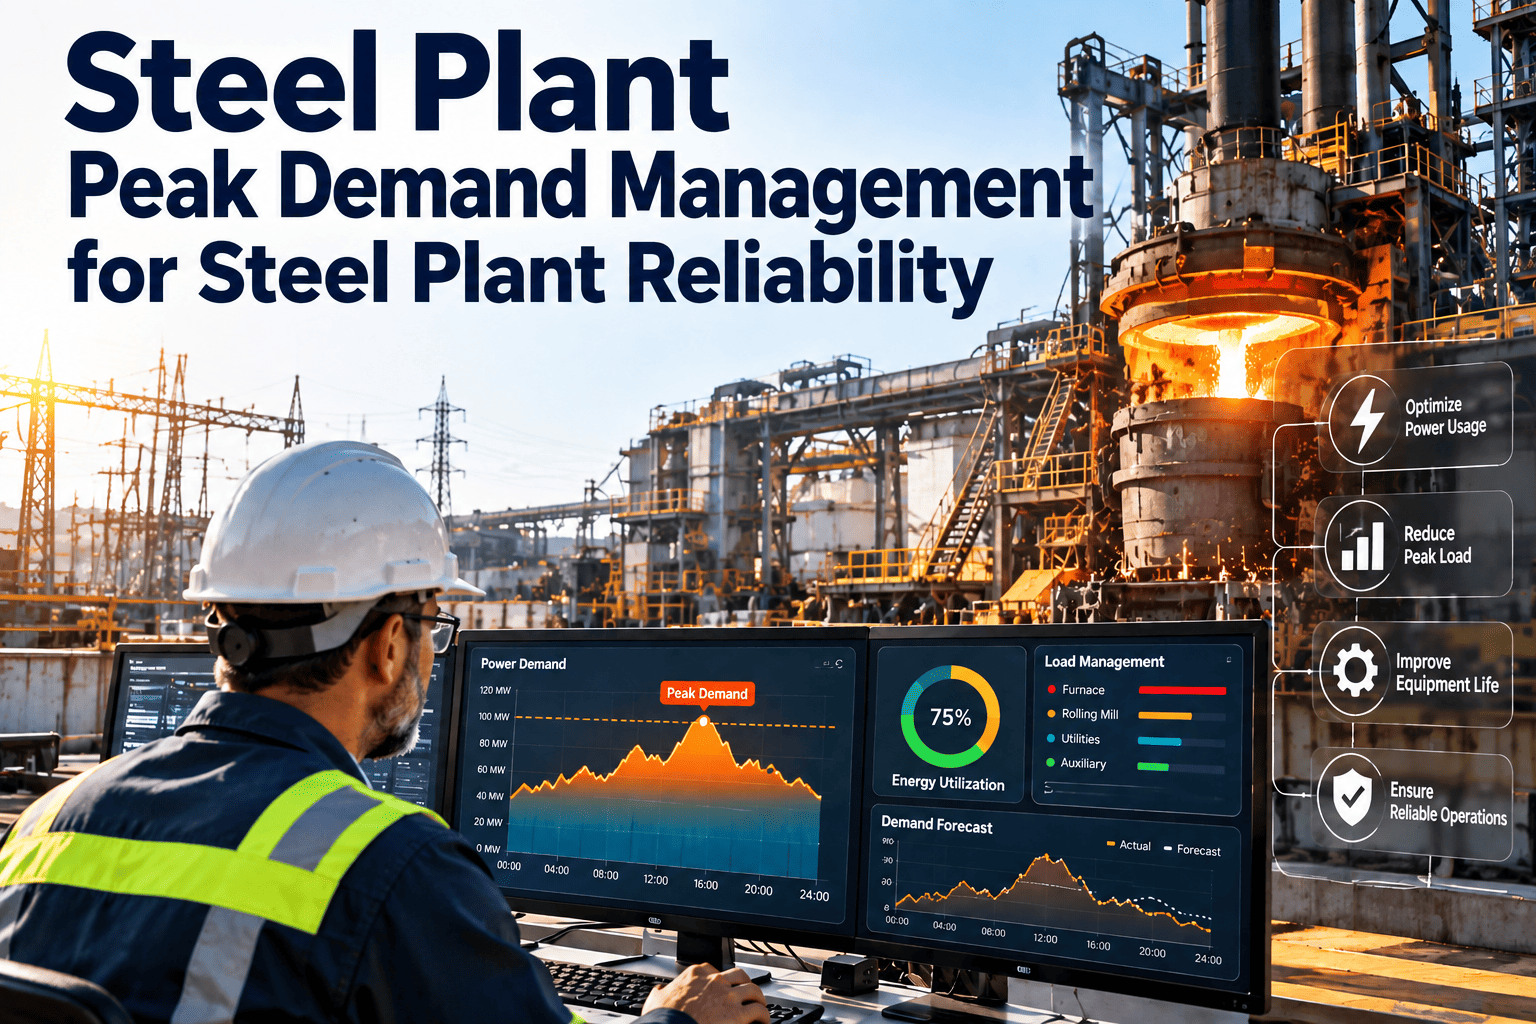
A steel plant can run a good month and still pay for one bad fifteen minutes. When an EAF, a ladle furnace, a rolling mill drive and several compressors all peak together, the utility meter records the highest average demand and the bill follows it. The trouble is that many of these overlaps start with equipment problems, not scheduling choices. This guide shows how to manage steel plant peak demand as a reliability topic, and how OXMAINT AI helps maintenance teams reduce the faults behind the spikes.
Steel Plant Peak Demand Management for Steel Plant Reliability
Peak demand is set by a short window and a stack of loads. Find the loads, fix the equipment behind the overlaps and keep restarts under control.
How Demand Charges Work
Which interval is used?
Is there a ratchet?
Are there peak windows?
Who supplies the data?
Reliability Causes Behind Avoidable Peaks
Scheduling causes
- EAF and ladle furnace heats that finish together
- Rolling mill start-up at the same time as furnace charging
- Compressors all loading after a shift change
- Planned tests scheduled inside the peak window
Equipment causes
- Drive or motor trips followed by rushed restarts
- Air leaks that keep compressors running
- Failed capacitor stages and poor power factor
- Blocked filters that push fan power higher
The Steel Plant Load Map
| Load | How it drives peak | Reliability factor | Control lever |
|---|---|---|---|
| Electric arc furnace | Highest power during melting, especially at start-up after charge | Electrode, regulator and transformer condition affect arc stability | Charge timing and power step profile |
| Ladle furnace | Overlaps with EAF heats when schedules bunch | Electrode and cooling faults extend heating time | Sequence with EAF tap timing |
| Rolling mill drives | Large motor loads with fast changes | Drive faults and trips cause restarts | Start sequencing and soft-start settings |
| Compressors | Many machines loading together | Air leaks increase run time | Load and unload sequencing |
| Fume extraction fans | Continuous, with large motors | Blocked filters and damper faults raise power | Variable speed control and duct repair |
| Cooling water pumps | Steady load with start-up spikes | Fouling and worn pumps increase draw | Staged starts and flow control |
Why Peak Demand Is a Reliability Problem
Find the Faults Behind Your Demand Peaks
Connect trips, restarts and repairs to the assets that caused them so your team removes the cause and not only the spike.
A Load Priority Ladder
A Peak Event Playbook
Where to Focus First: Impact and Controllability
Restart Discipline After a Trip
- Agree a restart order that brings large motors back one at a time, with a defined gap
- Confirm the cause of the trip before restarting, so a fault does not repeat under load
- Check that soft starters, drives and protection settings match the approved values
- Record the trip, the restart time and the demand result in a work order
- Review repeat trips on the same asset as a reliability issue, not a demand issue
EAF and Ladle Furnace Coordination
Share the heat schedule
Use start-up power steps
Keep the electrical path healthy
Record overlaps and causes
Compressors, Fans and Pumps: The Quiet Contributors
- Compressors often start together when pressure falls after a demand event, so staggering start delays and load bands reduces overlap
- Fume extraction fans run through the heat, so filter differential pressure and damper condition directly affect their power draw
- Cooling water pumps need staged starts, and worn pumps or fouled heat exchangers increase their steady consumption
- Standby machines should be tested on a schedule, so a failed unit does not force an unplanned start during a peak window
- Leak surveys on compressed air lines reduce run time and give a simple, repeatable maintenance task
Meter and Data Quality for Demand Work
A Sample Review of One Peak Interval
| Question | Where the answer comes from | Likely follow-up |
|---|---|---|
| Which loads were running? | Interval meter data and plant control logs | Update the sequencing rules |
| Did any large load restart just before the peak? | Trip log and operator notes | Raise a reliability work order for the tripped asset |
| Was power factor lower than usual? | Feeder power factor readings | Inspect capacitor banks and filters |
| Were compressors or fans working harder than normal? | Specific power trend by machine | Leak survey or filter replacement |
| Was planned work running in the window? | Maintenance schedule | Move similar tasks outside peak-critical hours |
Common Mistakes in Peak Demand Programs
- Setting a target without reading the tariff details
- Shedding loads that later cause a process or safety issue
- Treating each peak as a one-off event
- Leaving demand alerts with no named responder
- Scheduling maintenance tests at peak-sensitive hours
- Document the tariff rules and review them each year
- Agree the shed list with operations and safety
- Code every peak to a cause and track repeats
- Assign owners to alerts, by shift
- Plan work to avoid sensitive windows where possible
Records That Support Utility and Energy Reviews
- Peak event log with date, interval, cause and action taken
- Maintenance history for the assets involved in each event
- Calibration records for meters and protection devices
- Inspection records for capacitor banks, transformers and drives
- Evidence that corrective actions were completed and reviewed
Power Factor and Electrical Health
| Equipment | Why it matters for demand | Maintenance activity |
|---|---|---|
| Capacitor banks | Failed stages reduce power factor and raise apparent demand | Inspection, thermal scan, stage function test |
| Harmonic filters | Poor performance can affect power quality and heating | Condition checks and record of settings |
| Transformers | Overheating and tap issues affect losses | Oil, temperature and tap changer inspection |
| Motor starters and drives | Faults cause trips, restarts and stacked inrush | Preventive checks and fault history review |
| Metering and relays | Bad data hides the real peak driver | Calibration and communication checks |
Pre-Peak Window Readiness Checklist
Seasonal and Operating Condition Effects
- Warmer weather can raise cooling water temperature and increase fan, pump and chiller loads, so review cooling systems before summer
- Furnace campaigns and product mix change the load pattern, so revisit sequencing rules when the production plan changes
- Planned outages alter which loads run together, and restart plans after outages need the same care as trip recovery
- New equipment commissioning can create unusual start-up demand, which should be recorded and reviewed with maintenance and operations
KPIs for Demand and Reliability
| KPI | Meaning | Use |
|---|---|---|
| Peak demand versus target | Highest interval demand compared with the plant limit | Shows overall performance |
| Peak-hour overlap count | Number of intervals where large loads ran together | Finds scheduling issues |
| Trip-related restarts | Restarts within a set time after an unplanned stop | Links reliability to demand |
| Demand events with a maintenance cause | Peaks traced to equipment faults | Prioritizes repair work |
| Power factor by feeder | Measured power factor at main circuits | Tracks capacitor and filter health |
| Energy action closure rate | Demand-related work orders finished on time | Confirms follow-through |
A Practical Rollout
How a Steel Plant CMMS Supports Peak Demand Management
- Asset registers hold transformers, capacitor banks, drives, compressors and pumps with their history
- Preventive maintenance covers thermal scans, capacitor checks, filter changes and leak surveys
- Work orders record trips, restarts and repairs, and connect each to the demand event it affected
- Scheduling helps keep planned work out of peak-critical windows where operations allow
- Reports show repeat failures on assets that regularly take part in peak events
- Inventory tracking keeps critical electrical spares available for fast, safe recovery
Frequently Asked Questions
Keep Peaks Low by Keeping Equipment Healthy
Bring trips, restarts, electrical health and planned work into one maintenance system built for steel plant teams.