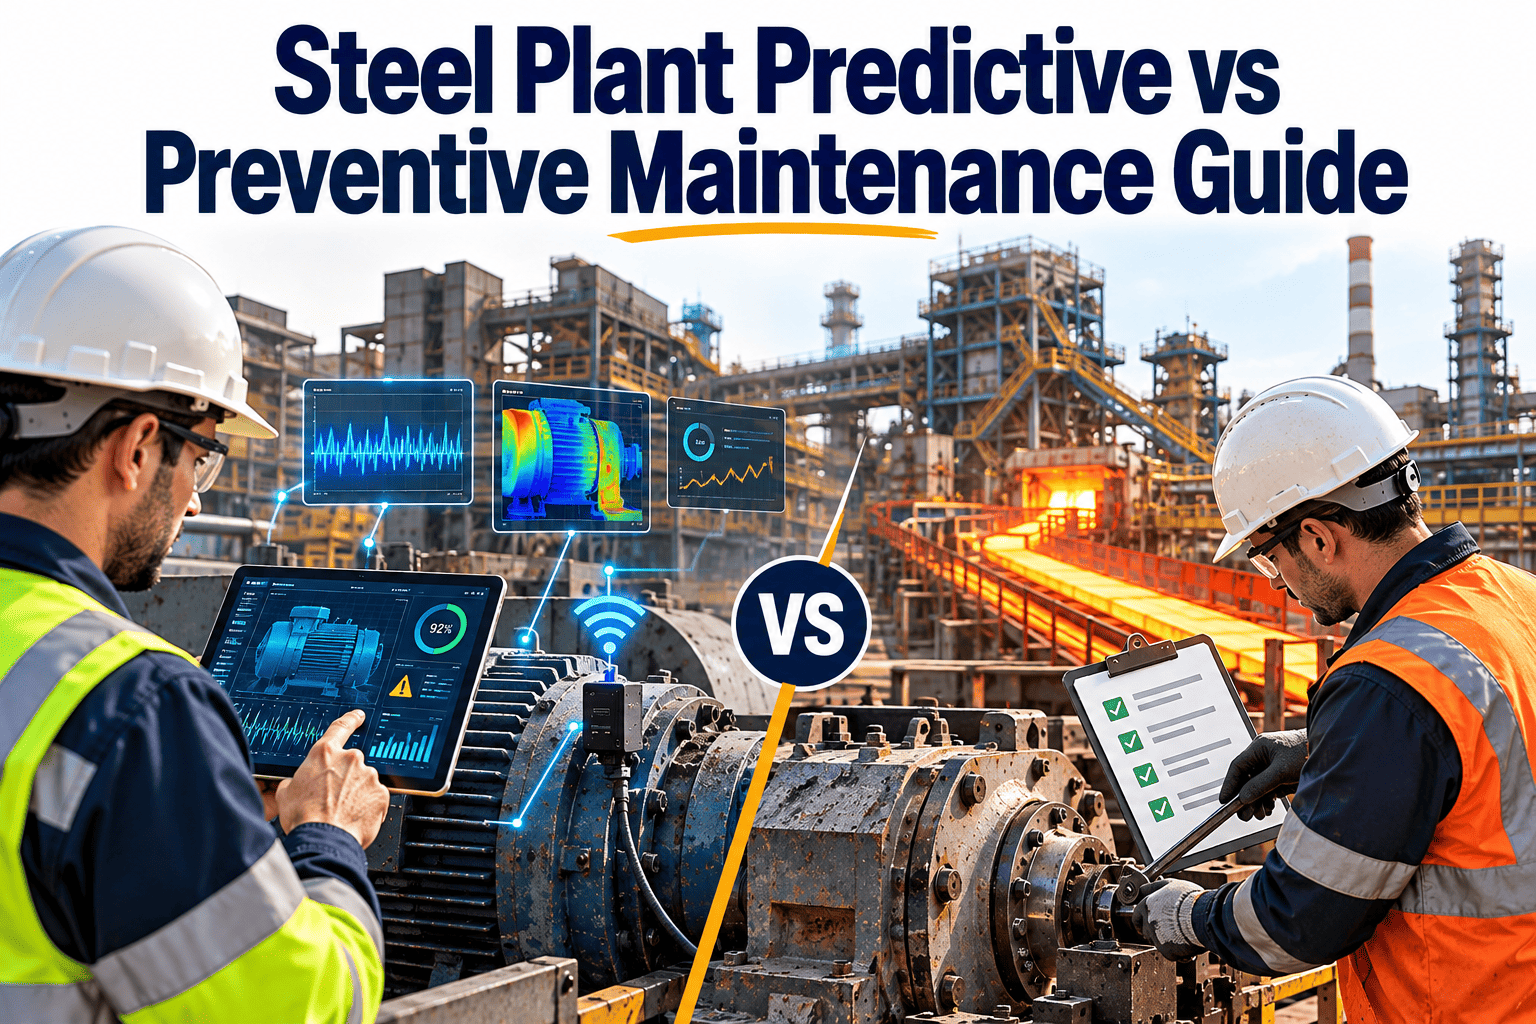
Reliability teams in steel plants face a constant question when planning maintenance strategy: should a bearing, gearbox, or hydraulic system be inspected on a fixed schedule, or should it be monitored continuously and worked on only when data shows a problem developing? The honest answer is that most steel plants need both, applied deliberately by asset criticality and failure mode rather than as a blanket policy. This guide breaks down where each approach fits, and where a maintenance platform that supports both strategies at once pays off.
Predictive or preventive? The right answer depends on the failure mode, not the asset type
A practical framework for deciding when sensors and condition data should drive maintenance, and when fixed-interval inspections and calendar tasks remain the better tool for steel plant reliability.
What preventive and predictive maintenance actually mean in a steel plant
Both strategies exist to avoid unplanned failure, but they reach that goal through very different mechanisms, and each has situations where it clearly outperforms the other.
Time or usage-based tasks
Lubrication, filter changes, belt tensioning, and component swaps performed on a fixed schedule regardless of measured condition, based on manufacturer guidance or historical failure data.
Condition-triggered tasks
Vibration, thermal, oil, and current data continuously assessed against thresholds, generating work orders only when a specific asset shows measurable degradation.
Predictive vs preventive maintenance across key decision factors
Neither strategy is universally better. The comparison below highlights where each one has a structural advantage for steel plant equipment.
| Factor | Preventive Maintenance | Predictive Maintenance |
|---|---|---|
| Best for | Low-cost, high-count components with predictable wear | High-value, high-downtime-cost rotating and thermal assets |
| Data requirement | Manufacturer intervals or historical failure records | Continuous sensor data and defined alert thresholds |
| Risk of over-maintenance | High — components replaced while still serviceable | Low — replacement tied to actual measured wear |
| Risk of missed failure | Moderate — interval may not match actual wear rate | Low, if sensor coverage and thresholds are well tuned |
| Upfront investment | Low — labor and parts only | Higher — sensors, gateways, and CMMS integration |
| Typical steel plant use | Filters, seals, lubrication, safety-critical checks | Motors, bearings, gearboxes, casters, furnace shells |
A practical checklist for choosing the right strategy per asset
Rather than deciding maintenance strategy plant-wide, reliability engineers get better results applying this checklist asset by asset, or even failure-mode by failure-mode on the same machine.
- Does failure of this asset stop production, or only degrade a non-critical function? High-impact assets favor predictive coverage.
- Is the failure mode gradual and detectable through vibration, temperature, or oil condition, or is it sudden and random? Gradual wear favors predictive.
- Is the component inexpensive relative to the labor cost of monitoring it? Low-value, high-count parts often favor simple preventive intervals.
- Is there regulatory or safety documentation required regardless of condition? Compliance-driven tasks usually stay preventive.
- Has failure history shown the fixed interval is consistently too early or too late? A mismatch is a strong signal to move to condition-based triggers.
Why RCM and FMEA still matter even with sensors everywhere
Reliability Centered Maintenance and Failure Mode and Effects Analysis are not replaced by predictive sensors — they are what tells a team which sensors to install and which thresholds actually matter.
Identify failure modes
List the specific ways each critical asset can fail, not just "bearing failure" but the mechanism behind it.
Rank by severity and frequency
Score each failure mode on downtime cost, safety impact, and historical occurrence rate.
Match the detection method
Assign each high-priority failure mode to a sensor signal, an inspection task, or both.
Build the maintenance plan
Codify the result into CMMS asset records as a mix of predictive triggers and preventive tasks.
Run predictive and preventive maintenance side by side, in one system
Manage sensor-triggered work orders and fixed-interval tasks together, with full asset history and reporting in one CMMS.
How to know if your maintenance mix is actually working
The right blend of predictive and preventive maintenance shows up in a small set of reliability metrics tracked over time rather than in any single work order.
Mean time between failures should trend upward as predictive coverage expands on critical assets.
The ratio of planned to unplanned work orders should shift steadily toward planned as thresholds mature.
Time spent on value-adding repair work, not searching for parts or diagnosing unclear faults, should rise.
Average bearing, gearbox, and belt life should extend as replacement shifts from calendar to condition.
Predictive vs preventive maintenance in steel plants, answered
Should a steel plant fully replace preventive maintenance with predictive?
No. Most reliable plants run a hybrid model, using predictive triggers on critical rotating and thermal assets while keeping preventive tasks for safety checks and low-cost components.
How do we decide which assets get sensors first?
Start with an FMEA-style ranking of downtime cost and failure frequency, then instrument the highest-impact assets whose failure modes are detectable through vibration, thermal, or oil data.
Can a single CMMS manage both strategies together?
Yes, a modern CMMS can run fixed-interval preventive schedules and sensor-triggered predictive work orders on the same asset record. Book a demo to see both in one dashboard.
What is the biggest risk of moving too fast to predictive maintenance?
Poorly tuned thresholds generate either alarm fatigue or missed failures. A shadow monitoring period before activating automatic work orders reduces this risk significantly.
How long does it take to build a mature RCM-based maintenance plan?
Most plants complete an initial FMEA and strategy assignment for critical assets within a few months, then refine thresholds and task intervals continuously using real failure data.
Build a maintenance strategy matched to each failure mode, not a one-size-fits-all schedule
Combine predictive sensor triggers with preventive scheduling in one platform built for steel plant reliability teams.