A steel plant rarely runs short of spares because nobody ordered them. It runs short because the ordering rules were built on guesses instead of consumption history. Gate plates, mill bearings, hydraulic valves, couplings and crane brakes all wear at different rates, and each melt shop, caster and rolling mill pulls them differently. This guide shows how to turn issue records and work order history into maintenance planning decisions, so the parts that stop production are on the shelf and the parts that do not are not tying up cash. If you want to see how stock, work orders and asset history can sit in one record, you can start with Oxmaint.
Steel Plant Spare Parts Consumption Analytics for Maintenance Planning
Read what each part actually does in your plant: how fast it is consumed, what drives that demand, and what happens when it is missing. Then set stocking rules that follow the evidence.
Shortage and excess happen in the same storeroom
Where the plant is short
- A critical bearing or coupling is needed and the only spare is already installed elsewhere.
- Returned parts were never booked back, so the system shows zero while the part sits on a bench.
- Lead time changed at the supplier, but the reorder point still assumes the old figure.
- Emergency purchases fill the gap at premium price and the part arrives after the repair window.
Where the plant is overstocked
- Parts for equipment that was modified or retired still sit on shelves with live stock values.
- One-time project purchases were stocked as if they were routine consumables.
- Safety stock was set once, copied across similar items and never revisited.
- Duplicate item records split the true consumption of one part across several codes.
Six questions consumption data should answer
What is consumed, and how often?
Issues per month by item, split by planned jobs and breakdowns, show whether demand is steady, seasonal or lumpy.
Which asset is driving it?
Consumption linked to a mill stand, ladle crane or pump group shows where wear is concentrated and where a design or lubrication fix may pay back.
Is demand planned or random?
Planned replacements can be forecast from the maintenance schedule. Random failures need statistical history and criticality judgment.
How long does replenishment really take?
Measure actual order-to-receipt time, not the quoted figure. The gap between them is hidden risk.
What happens if the part is missing?
Criticality decides how much stock the plant should hold, regardless of how rarely the part is used.
Which stock has stopped moving?
Items with no issues across several maintenance cycles are candidates for review, return, transfer or write-off.
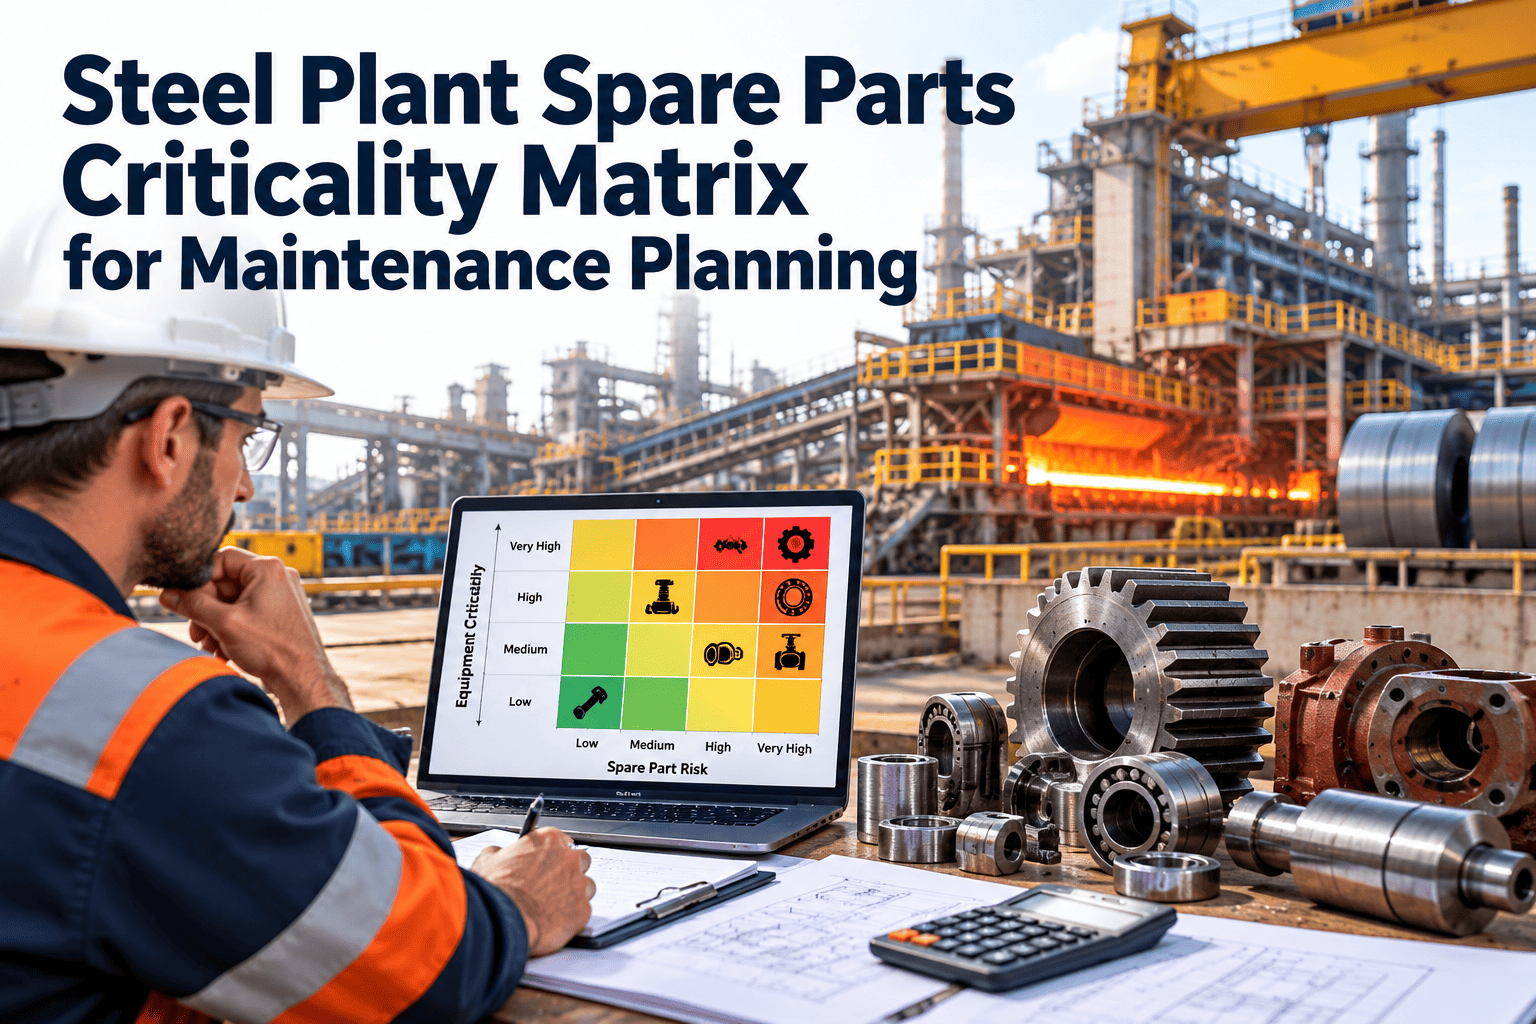
Classify spares by value and by consequence
ABC analysis ranks parts by annual consumption value. VED analysis ranks them by criticality: vital, essential or desirable. Combining the two gives nine stocking strategies instead of one blanket rule.
Demand behaves differently in each production area
Melt shop and ladle handling
Wear items such as ladle slide gate plates, nozzles and lining shapes follow heat counts and campaign plans. Crane, hydraulic and safety-related spares need protected stock instead.
Driver: heats and campaignsContinuous casting
Mold components, segment rollers, bearings and spray nozzles combine scheduled replacement with failure-driven demand. Track both streams separately.
Driver: casting hours and segment conditionHot rolling
Rolls, chocks, bearings, gearbox parts and hydraulic components have long lead times and high outage cost. Link stock to the roll change and shutdown calendar.
Driver: tonnage and shutdown planRaw material handling and utilities
Conveyor belts, idlers, pumps, fans and compressors show steady consumption that suits statistical reorder rules, with exceptions for single-point-of-failure items.
Driver: running hours and dutyFrom consumption history to a reorder rule
Reorder point
Safety stock grows with demand variability, lead time variability and the service level you want. For vital items, add a minimum quantity that does not depend on the formula at all.
Worked example with assumed figures
- Average consumption: 3 units per month
- Actual lead time: 2 months
- Safety stock chosen for service level: 2 units
- Reorder point: 3 x 2 + 2 = 8 units
Intermittent demand needs different logic
Many critical spares are used once every few years. An average built from such sparse history is misleading, so use criticality, installed population and failure mode instead of a consumption average.
Clean the data before you trust the analytics
Before: analytics built on weak records
- Parts issued to a cost center, not to an asset or work order.
- Free-text descriptions create duplicate item codes.
- Unused parts are not returned in the system.
- Consumption is booked at month end, not at the job.
After: analytics built on usable records
- Every issue references an asset and a work order.
- One controlled item master with approved descriptions.
- Returns booked back the same shift.
- Cycle counts focus on vital and high-value items first.
Measures that show whether planning is working
| Measure | What it shows | Warning sign |
|---|---|---|
| Stockout rate on vital items | How often a critical part was needed and not available | Repeat stockouts on one item point to a wrong reorder point or lead time |
| Emergency purchase share | Portion of purchases raised as urgent or expedited | Rising share means planning is losing to breakdowns |
| Inventory turns by class | How quickly stock is consumed in each tier | Low turns on C-class items hide carrying cost |
| Slow and non-moving share | Stock with no issues over a defined review period | Growth after equipment changes suggests orphaned spares |
| Parts ready at job start | Planned jobs with all required parts reserved | Low readiness stretches downtime and repeat visits |
| Stock record accuracy | Match between system quantity and physical count | Poor accuracy makes every other measure unreliable |
Link every spare part to the asset that consumes it
Oxmaint connects inventory, work orders and asset history so consumption analysis starts from real maintenance events instead of spreadsheets.
A monthly consumption review that feeds maintenance planning
Reconcile stock records
Resolve open returns, unreserved issues and negative balances so the month starts clean.
Rank consumption by value and asset
List the top consumed items and the assets behind them, then ask whether the wear is expected.
Check vital items against lead time
Confirm on-hand quantity covers the current replenishment time plus the next planned outage.
Match parts to the forward schedule
Compare upcoming preventive work and shutdown tasks to stock, and order shortfalls early.
Review slow movers and emergencies
Decide what to hold, return or retire, and trace each emergency purchase to its root cause.
Where a CMMS fits in spare parts analytics
Software helps only with disciplined records
No tool can repair inaccurate issues or duplicate item codes. Agree item naming, return rules and reservation habits first, then let the system enforce them.
Planning mistakes to avoid
Using one safety stock percentage everywhere
Criticality and lead time should set the buffer, not a flat rule.
Ignoring parts for retired equipment
Review stock whenever an asset is modified, replaced or decommissioned.
Trusting quoted lead times
Record actual receipt dates and update reorder points from them.
Cutting stock without checking criticality
Reducing value is only safe after vital items are protected.
Treating every consumption spike as normal
Repeated high consumption on one asset often signals a reliability problem.
Reviewing stock once a year
Short monthly reviews catch drift before it becomes a stockout.
Four demand profiles and what each one needs
Grouping parts by how they are consumed matters more than grouping them by catalogue category. Each profile calls for a different trigger and a different kind of review.
Steady consumables
Filters, lubricants, seals and standard fasteners are used at a predictable rate. Statistical reorder points and periodic review work well, and supplier-managed replenishment can reduce handling.
Production-driven wear
Nozzles, plates, rolls and liners wear with heats, tonnage or running hours. Forecast them from the production and campaign plan rather than from last month's issues.
Random failure parts
Motors, gearbox components and valves fail unpredictably. Stock depends on criticality, number of installed units and the time needed to repair or replace.
Project and outage parts
Items bought for a rebuild or shutdown should be linked to that job and cleared afterwards, so they do not slip into normal stock and distort consumption history.
Use consumption history to plan the shutdown
Planned outages concentrate demand into a short window, and missing parts there cost more than at any other time. Consumption analytics helps build the parts list long before the outage starts.
Pull history from comparable outages
Review which parts were issued, which were requested but missing and which were drawn from stock and never used.
Add condition findings
Inspection reports and deferred corrective work show which components are likely to need replacement during the window.
Compare against lead times
Anything with a lead time longer than the time left must be ordered now, expedited, sourced as a repairable exchange or deferred.
Reserve parts against work orders
Reservations prevent two jobs from relying on the same spare and give the planner an honest readiness figure.
Record what was not used
After the outage, return unused parts and log those that were needed but absent. That list is the most valuable input for the next outage plan.
Supplier and lead time analytics
A reorder point is only as good as the lead time behind it. Track supplier performance with the same discipline you apply to consumption.
Actual versus quoted lead time
Compare order date with receipt date by supplier and item. Use the observed range when setting safety stock, not the catalogue figure.
Single-source exposure
List vital parts that depend on one supplier or one country of origin, and decide where a second source or a buffer is justified.
Repair and exchange options
For high-value rotating parts, a repairable cycle with a refurbishment partner can reduce the number of full spares held.
Handling excess and obsolete stock
Signals an item is excess
- No issues across several maintenance cycles and no planned job that needs it.
- Quantity on hand covers many years of observed consumption.
- The asset it belongs to has been replaced or modified.
- A newer part number has superseded it.
Options before a write-off
- Check whether another plant area uses the same or a compatible part.
- Ask the supplier about return or buy-back terms.
- Reduce the minimum to zero and stop reordering.
- Keep one unit only when the part is vital and cannot be sourced quickly.
Frequently asked questions
What is spare parts consumption analytics in a steel plant?
It is the analysis of issue history by item, asset and work order to set reorder rules and safety stock. The aim is fewer critical stockouts and less idle inventory.
How do I stock parts that are rarely used but critical?
Use criticality, installed population and lead time instead of an average. Hold a defined minimum, such as one insurance spare, and review it before outages.
What data do I need to start?
Issue and return records linked to assets and work orders, actual lead times and a clean item master. You can book a demo to see how this is organized in a CMMS.
Does a CMMS replace the ERP for purchasing?
Not necessarily. Many plants keep ERP for procurement and finance while using the maintenance system for asset-linked consumption and planning.
How often should reorder points be reviewed?
Review vital items monthly and the rest quarterly or after any lead time, equipment or process change. Static levels drift quickly in a steel plant.
Plan maintenance around the parts you will actually need
Bring consumption history, criticality and work orders into one workspace, and set stocking rules your maintenance team can defend.