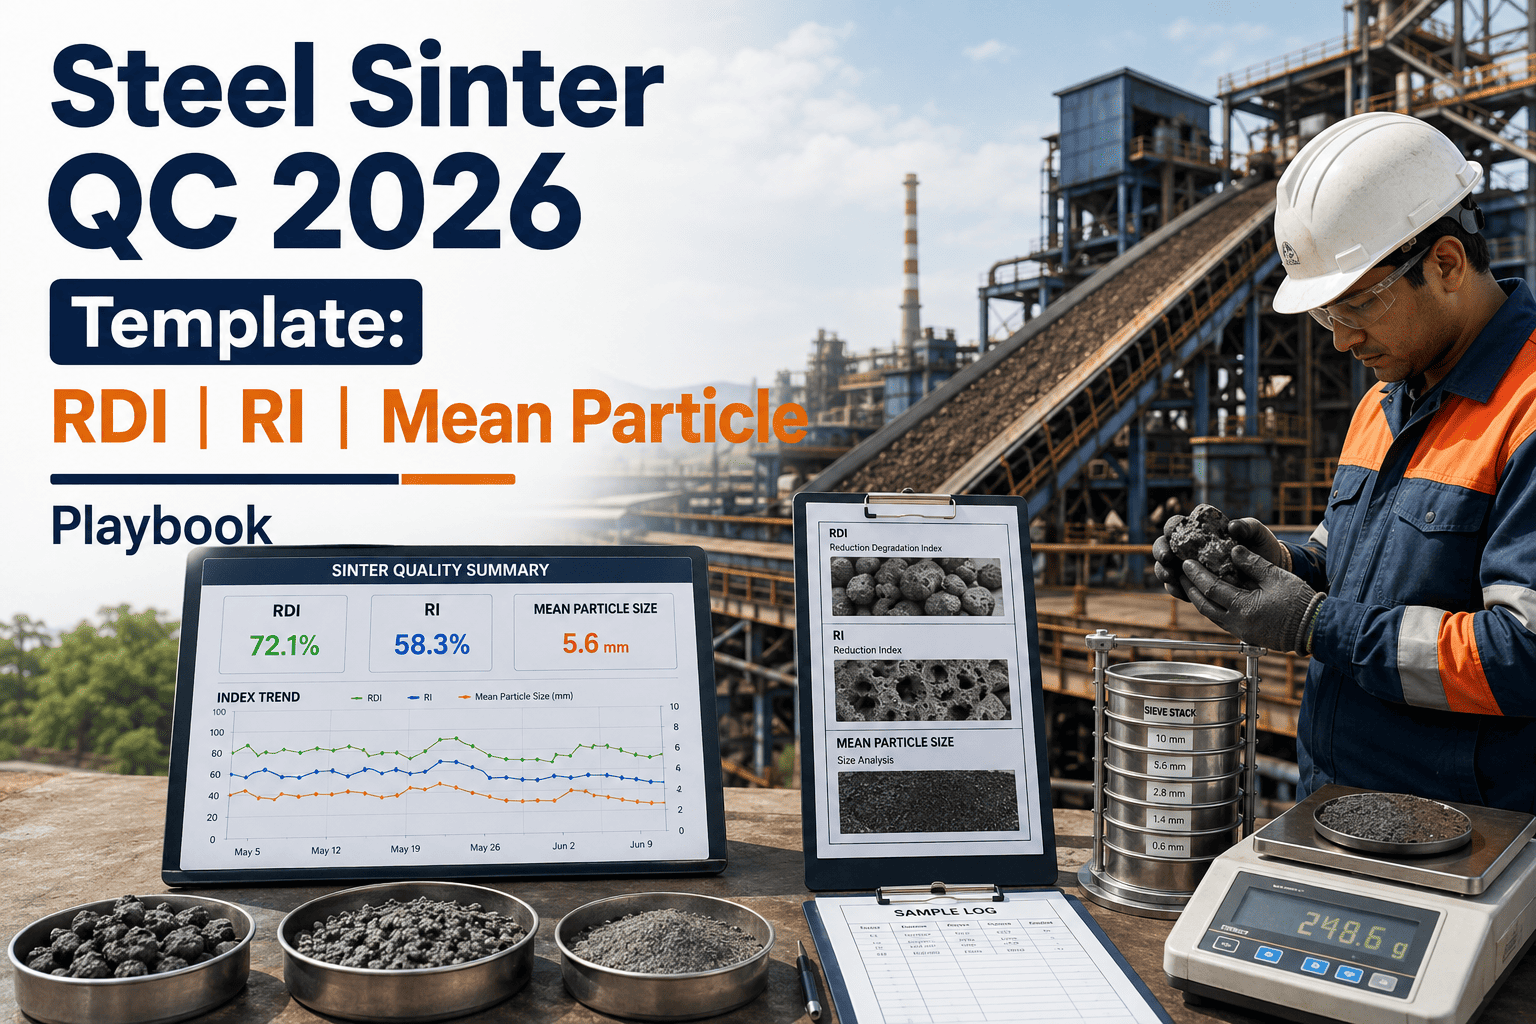
A blast furnace does not care how a sinter plant explains an off-spec strand — it only cares whether the sinter charged into the stack holds its strength, breaks down slowly under reduction, and keeps the burden permeable enough for gas to flow. This page is built as a working checklist — index targets, strand-side process checks, sampling cadence, and root-cause reference — grouped exactly the way a sinter plant QC checklist should run shift to shift. Open this checklist inside Oxmaint to run it against your own strand data.
The RDI, RI & Mean Particle Size Checklist For Every Strand
Six checklist sections covering index targets, strand-side process checks, sampling cadence, raw mix checks, documentation, and root-cause reference.
Index Target Checklist
Confirm each of these five indices is being tracked against a defined target band before relying on any single lab result in isolation — they move together, and optimizing one without watching the others creates a new problem.
Confirm RDI is tracked and trending toward target
Reduction Degradation Index, tested per ISO 4696, measures disintegration under reducing conditions. High RDI increases fines in the cohesive zone — controlled primarily by FeO content and MgO addition.
Confirm RI is tracked against the FeO balance
Reducibility Index — high RI lowers blast furnace coke rate and improves productivity, but trades off against RDI when FeO is pushed too low.
Confirm Tumbler Index is tracked per shift
TI is the primary measure of mechanical strength, based on plus-6.3mm retention after tumbling — controlled by coke breeze rate, basicity, and burn-through point.
Confirm basicity is held in the 1.7–2.1 band
CaO/SiO2 ratio, controlled by limestone and lime dosing — drift in either direction moves both RI and TI off target at the same time.
Confirm mean particle size is holding 15–25mm
A shift toward smaller particle size usually tracks with declining strength and often shows in the windbox profile first.
Confirm FeO is balanced against RDI and TI
Low FeO improves reducibility but reduces strength; high FeO improves strength but penalizes RDI — the core daily optimization problem on most strands.
Predict The Lab Result Before The Strand Discharges
Oxmaint tracks windbox pressure, burn-through point, and basicity trend against historical results, so the checklist flags a developing deviation before the sixty-to-ninety-minute lab lag confirms it.
Strand-Side Process Checklist
Lab results confirm quality after the fact. These are the process signals a strand operator and shift supervisor should be checking continuously, because they move the five indices before the lab ever sees a sample.
Verify burn-through point is within 85–92% of strand length
A BTP outside this window signals strand speed or coke breeze rate is off, and correlates directly with both TI and RDI drift.
Compare the windbox pressure profile against the expected zone curve
Compare the live profile per zone against the historical curve correlated with acceptable TI and RDI results.
Confirm bed height and moisture are within target
Both feed directly into permeability and burn-through consistency across the strand width.
Log strand speed against the current coke breeze rate
Strand speed and coke breeze rate move together — logging them separately hides the correlation that explains most BTP shifts.
Log the return fines ratio each shift
A rising return fines ratio is often the earliest visible sign that TI is trending down before the lab confirms it.
Sampling & Test Method Checklist
Pull a per-shift composite sample for Tumbler Index
Tested per ISO 3271 rotating drum method by the sinter plant lab technician.
Pull a daily composite sample for RDI and RI
RDI tested per ISO 4696-1 / 4696-2; RI tested using the ISO relative reducibility method.
Sample raw mix and product basicity hourly
By XRF or wet chemistry, logged by the blending yard operator against the target band.
Run a screen analysis for mean particle size per shift
Performed post-screening by the sinter plant lab technician.
| Index / Check | Test Method | Sampling Frequency |
|---|---|---|
| Tumbler Index (TI) | ISO 3271 rotating drum test | Per shift composite sample |
| Reduction Degradation Index (RDI) | ISO 4696-1 / 4696-2 | Daily composite sample |
| Reducibility Index (RI) | ISO relative reducibility test | Daily composite sample |
| Basicity (CaO/SiO2) | XRF or wet chemistry | Hourly, raw mix and product |
| Mean Particle Size | Screen analysis | Per shift, post-screening |
Turn Windbox Data Into An Early-Warning Checklist
Connect your strand PLC and windbox thermocouple array to Oxmaint and get a live checklist status instead of a shift-end paper log.
Equipment & Raw Mix Checklist
Chemistry checks get most of the attention, but mechanical condition on the strand and pallet cars directly affects yield and fines generation just as much as raw mix control does.
Weekly: measure pallet car grate bar gap
Gaps exceeding 8mm let raw mix fall through, reducing yield and increasing the return fines ratio fed back into the mix.
Daily: lubricate pallet cars and check wheel condition
Minimum standard maintenance to prevent uneven bed distribution across the strand width.
Verify raw mix basicity against the blending bed target
Checked hourly, since basicity drift moves RI and TI in opposite directions and is one of the fastest levers to correct.
Confirm limestone and lime dosing equipment calibration
Dosing inconsistency is the most common cause of a basicity swing outside the target band.
Reading The Result — In-Spec vs Out-Of-Spec
In-Spec Sinter
Out-of-Spec Sinter
Reading these two columns side by side during a shift handover is often more useful than reciting the raw numbers, because it forces the outgoing and incoming shift to agree on which direction the strand is trending before a lab result confirms it either way. Plants that build this comparison into the daily handover routine tend to catch a developing deviation a full shift earlier than plants relying on the lab report alone.
Root Cause Reference Checklist
When an index moves off target, use this reference to point the shift toward the most probable cause instead of leaving the diagnosis to memory.
| Observed Deviation | Most Likely Cause | Corrective Action |
|---|---|---|
| RDI trending upward across shifts | FeO content running low relative to target | Adjust coke breeze rate, review burn-through point position |
| TI trending downward | Basicity drift or coke breeze rate inconsistency | Re-check raw mix proportioning against blending bed target |
| Basicity swinging outside 1.7–2.1 band | Limestone or lime dosing inconsistency | Verify dosing equipment calibration, sample raw mix hourly |
| Mean particle size trending smaller | Burn-through point outside 85–92% strand length | Adjust strand speed or coke breeze rate |
| Rising return fines ratio | Grate bar gap beyond 8mm tolerance | Inspect and replace worn grate bars on the pallet cars |
How A CMMS Runs This Checklist Across Every Strand Campaign
Live windbox profile comparison
Every zone's live pressure profile is compared against the historical curve tied to acceptable TI and RDI outcomes.
Predictive quality forecast
Models trained on historical operating data forecast FeO, RDI, and basicity ahead of strand discharge, replacing the lab lag with a live estimate.
Grate bar and pallet car PM
Weekly grate bar gap measurement and pallet car PM schedules are tracked alongside quality data, not in a separate system.
Shift checklist with sign-off
Burn-through point, bed height, and basicity checks are logged per shift with a supervisor sign-off, building a full audit trail.
Frequently Asked Questions
What is a typical basicity target for blast furnace sinter?
Why do RDI and RI sometimes move in opposite directions?
How long does a lab result typically lag behind the strand?
What causes mean particle size to drift smaller?
Can grate bar condition really affect sinter quality?
Run RDI, RI & Mean Particle Size On One Connected Checklist
Windbox trends, basicity checks, grate bar PM, and lab results — one shift checklist instead of five disconnected logs.