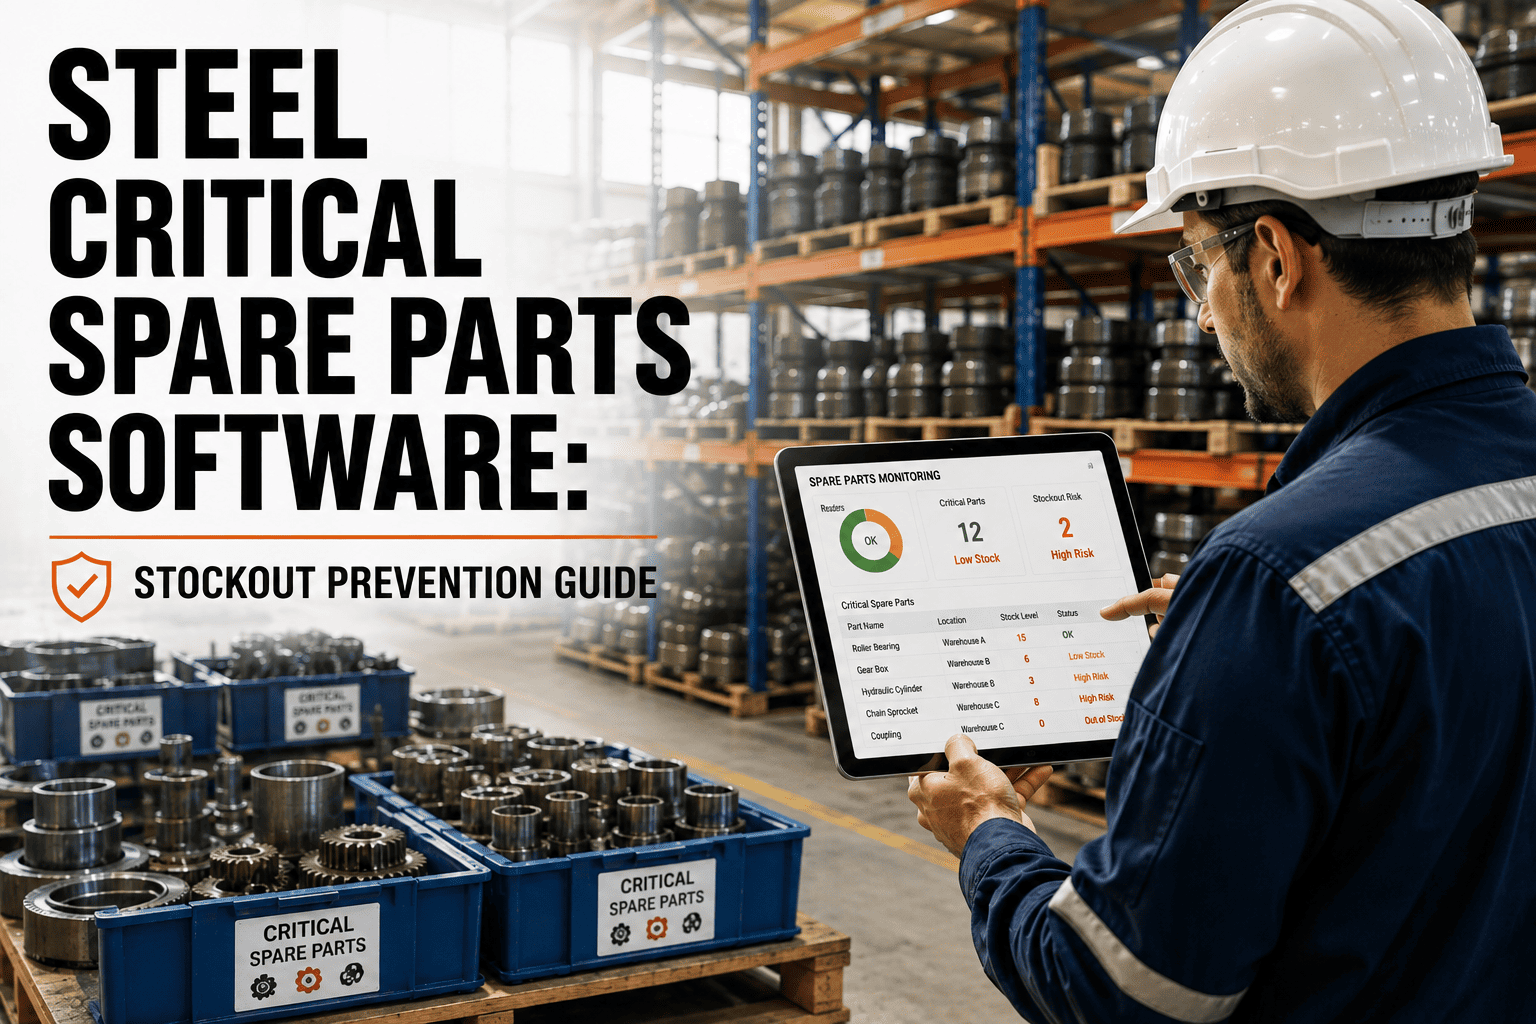
Every steel plant storeroom has the same two complaints at once: shelves full of parts nobody uses, and urgent orders for parts nobody expected to need. Both come from reorder points that were set once and never tested against real usage. This guide shows how consumption trend analysis by asset, failure mode, and shop turns issue history into better stock levels, and how Oxmaint inventory and maintenance software keeps the supporting data clean.
Steel spare consumption trend software for smarter reorder points
Track what is actually used, where, and why. Then set stock levels from evidence instead of memory.
Monthly issues of one spare, illustrative
Two spikes come from planned outages. Averaging all twelve months would overstate steady demand. Sample shape only, not plant data.
Why reorder points drift away from reality
Most reorder points start as a sensible guess from an experienced storekeeper. Then equipment changes, vendors change, and nobody revisits the number.
- Set once, never reviewed.The reorder point was entered when the part was created and not touched after the asset changed.
- Lead time frozen at setup.The vendor now takes longer, but the stock level still assumes the old delivery time.
- Outage demand mixed with routine demand.Totals include planned shutdown usage, which inflates the average.
- Usage booked to the wrong asset.Parts are issued to a cost center, so nobody sees which machine really consumes them.
From storeroom issue to a usable consumption signal
Analytics are only as good as the chain that creates the data. Each link below must be recorded at the moment of work, not reconstructed later.
- 1Part issuedIssue the part against a work order, not a general account.
- 2Work order linked to assetThe order names the exact machine or component position.
- 3Failure mode codedThe technician selects the reason, such as wear, leakage, or overload.
- 4Work type taggedMark it as preventive, corrective, emergency, outage, or project.
- 5Shop recordedNote which crew or workshop used the part.
- 6Trend reviewedUsage is summarized by asset, failure mode, and shop on a regular cycle.
- 7Stock level adjustedReorder point and order quantity are updated from the findings.
Three lenses on the same consumption data
Looking at consumption one way answers one question. Using three views together tells you what to stock, what to fix, and who needs help.
Per asset
Which machines consume the most parts?
- Finds bad actor equipment
- Supports asset replacement cases
- Reveals how much a line really costs to run
Per failure mode
Why are parts being consumed?
- Separates wear from misuse or poor installation
- Points to root cause projects
- Shows which failures repeat
Per shop
Who is using the parts, and how?
- Compares usage of the same part across crews
- Flags practice or training differences
- Shows where rebuilt parts return sooner
A short example of the lenses working together
Suppose roller bearings are issued heavily. By asset, one conveyor accounts for most of them. By failure mode, most are contamination related. By shop, one crew uses far fewer. That points to a seal problem and a best practice to share, not a bigger stock level.
Why lumpy demand breaks simple averages
Maintenance spares are used irregularly. Many parts sit untouched for months, then several are needed at once. A plain average hides that pattern.
Illustrative calculation
- Steady usage, outages removed: 6 units in 30 days, or 0.2 per day
- Vendor lead time: 30 days
- Demand during lead time: 0.2 x 30 = 6 units
- Safety stock set by criticality: 3 units
- Reorder point: 6 + 3 = 9 units
The figures are only a worked example. The method matters more: remove outage usage, use the real lead time, and set safety stock from how much a stockout would hurt production.
Put consumption history to work in your storeroom
See how issues, work orders, and stock levels connect for your plant.
Separate planned from unplanned consumption
The same part may be used in four very different ways. Tag the type so each can be forecast on its own terms.
| Consumption type | How to tag it | How to forecast it |
|---|---|---|
| Preventive | Work order from a PM schedule | Forecast from the PM calendar and asset count |
| Corrective | Planned repair after a found defect | Use failure history by asset and failure mode |
| Emergency | Unplanned breakdown work order | Use safety stock and failure probability |
| Outage | Orders tied to a shutdown event | Plan from the outage scope, not the monthly average |
| Project | Orders under a capital project | Exclude from routine reorder calculations |
Data hygiene checklist before you trust any trend
Run through these checks first. Dirty data produces confident but wrong stock levels.
- Parts are issued to work orders, not to general cost centers
- Returns to stock are posted so usage is not overstated
- Duplicate part numbers for the same item are merged
- Units of measure are consistent for each part
- Failure codes are selected from a short standard list
- Asset names match the plant hierarchy used by operations
- Counts of physical stock are checked against system balances
- Vendor lead times are updated from actual delivery dates
Where steel plant consumption patterns show up
Different areas consume different parts for different reasons. The table lists common examples to consider when reviewing your own data.
| Area | Frequently consumed spares | What to look for in the trend |
|---|---|---|
| Raw material and sinter conveyors | Idlers, belt fasteners, scrapers | Zone based wear and dust related failures |
| Blast furnace and stoves | Valve seals, actuator parts, instruments | Cycling frequency and heat related repeat failures |
| Steel melt shop | Hydraulic hoses, cooling components, wear parts | Consumption linked to heat count |
| Casting and rolling | Bearings, seals, roll related parts, nozzles | Consumption by campaign and tonnage |
| Utilities and pumps | Mechanical seals, bearings, couplings | Repeat seal failures on specific pumps |
Link usage to production volume
Where output varies, express consumption per tonne, per heat, or per campaign. That lets you tell the difference between a part failing more often and a plant simply running harder.
Comparing shops fairly
Shop level comparison is powerful, but only if the work is comparable. Compare like with like before drawing conclusions.
- Use the same asset type and similar operating conditions
- Compare per operating hour, per tonne, or per job, not raw counts
- Look at repeat failures after repair, not only the first fix
- Ask the crew what they do differently before assuming a fault
Share what works
When one crew consistently uses fewer parts, write their method into the job plan. The goal is to spread good practice, not to rank people against each other.
Signals worth acting on
Rising use on one asset
Raise a root cause review before simply stocking more.
Use falls after a PM change
The change may be working. Keep the new interval and recheck stock.
One shop uses far fewer
Study the method and share it as a standard job step.
Sudden step change
Check for a new vendor, new part grade, or process change.
Which parts deserve analysis first
A plant may stock tens of thousands of items, and trend analysis on all of them is not realistic. Combine usage value with criticality to decide where to look first.
| Group | Description | Analysis depth |
|---|---|---|
| High value and vital | Expensive parts whose absence stops a production line | Full review by asset, failure mode, and lead time risk |
| Low value and vital | Cheap parts that can still halt output | Safety stock check and supplier backup |
| High value and routine | Costly parts with workable alternatives | Consumption trend and order quantity tuning |
| Low value and routine | Common consumables | Simple minimum and maximum rules |
Criticality scoring should be explicit
Write down how criticality is scored, such as production impact, safety effect, and replacement lead time. When the scoring is visible, the team can challenge it and update it as the plant changes.
How to read a monthly consumption review
A short, regular meeting beats a large annual exercise. Bring the same four views each month and the discussion stays practical.
- 1Top assets by parts usedAsk whether each one is expected or a bad actor.
- 2Top failure modesChoose one repeat mode for a root cause study.
- 3Parts below or above targetAdjust stock levels where usage clearly changed.
- 4Emergency purchasesExplain each one and note what stock rule would have prevented it.
Keep decisions small and traceable. One level change with a reason is better than a bulk rewrite nobody can explain.
Supplier and quality effects hide inside consumption
A part that suddenly fails sooner may not be a maintenance problem. Check the supply side before you raise stock.
- Compare usage before and after a vendor or brand change
- Record batch or supplier details on high consumption parts
- Note whether rebuilt or repaired parts last as long as new ones
- Track warranty returns so claims are not missed
Turn findings into purchasing evidence
Documented early failures give purchasing a factual basis to negotiate with suppliers, change specifications, or qualify a second source.
From usage trends to a maintenance budget
Consumption history also supports budget planning. When parts use is tied to assets and work types, finance can see which lines drive spend and why.
- Forecast preventive part costs from the PM calendar
- Estimate corrective needs from failure history with a clear margin
- Plan outage purchases separately from routine spend
- Show how root cause fixes reduce future parts demand
Common mistakes to avoid
- Raising stock every time a stockout happens without asking why
- Treating all parts the same regardless of criticality
- Leaving obsolete parts in the system and in the totals
- Reviewing reorder points only when the auditor asks
KPIs for spares and consumption
- Stockout rateRequests that could not be filled from stock divided by all requests.
- Emergency purchase countUrgent orders per month, trended by area.
- Reorder point review ageShare of critical parts reviewed within the last year.
- Inventory turnsAnnual issue value divided by average stock value.
- Slow moving shareStock value with no usage in a defined period.
Slow movers, obsolete stock, and repairable spares
Consumption trends also show what the plant no longer needs. Parts with no usage for a long period deserve a deliberate decision rather than quiet storage.
- Flag parts with no issues in a defined period and review them with engineering
- Confirm whether the asset they serve is still in service
- Consider return to vendor, transfer to another site, or disposal
- Keep slow movers that protect a critical asset, but record the reason
Repairable and exchange items
Gearboxes, motors, and similar items are repaired and returned to stock. Track each cycle separately, because the useful number is how often a unit fails, not how often a new one is bought.
Using consumption data in shutdown planning
Outage scope lists often grow from habit. Past consumption on comparable jobs gives planners a factual starting point for parts lists.
- Pull parts used on similar jobs from earlier outages
- Compare planned and actual usage and record the difference
- Check lead times early so long delivery items are ordered in time
- Return unused outage parts to stock with correct postings
Closing the loop after each outage makes the next parts list shorter, safer, and cheaper.
A staged rollout
Stage one
Clean part masters and link critical spares to the assets that use them.
Stage two
Issue every part against a work order and require work type and failure code.
Stage three
Review consumption monthly and adjust reorder points for the highest value and highest criticality parts first.
Keep the first pass small
Choose one production area and its top fifty critical spares. Prove that the data chain works there, then extend the same routine to the next area with the lessons already learned.
How Oxmaint supports consumption analytics
Oxmaint connects the storeroom to maintenance work so consumption data is created at the point of use.
| Need | Oxmaint capability |
|---|---|
| Know where parts go | Parts issued against work orders and linked to assets |
| Control stock levels | Inventory with minimum and reorder levels |
| Forecast preventive demand | Preventive maintenance schedules showing upcoming part needs |
| Capture usage in the field | Mobile work orders with parts and readings |
| See trends | Reports and dashboards by asset, work type, and period |
Frequently asked questions
How much history do I need?
Twelve to twenty four months is useful, with outages tagged separately. Less data still helps if it is clean.
Should every part get a calculated reorder point?
Start with critical and high value parts. Low value items can use simple rules.
What if usage is too irregular?
Use criticality and failure history to set safety stock. See how in a short demo.
Does consumption data help beyond stock?
Yes. It finds bad actors and training gaps. You can start tracking in Oxmaint today.
How often should levels be reviewed?
Review critical parts at least annually and after any major equipment or vendor change.
Stop guessing stock levels and start reading the usage
Connect issues, assets, and failure modes in one system and let the data set your reorder points.